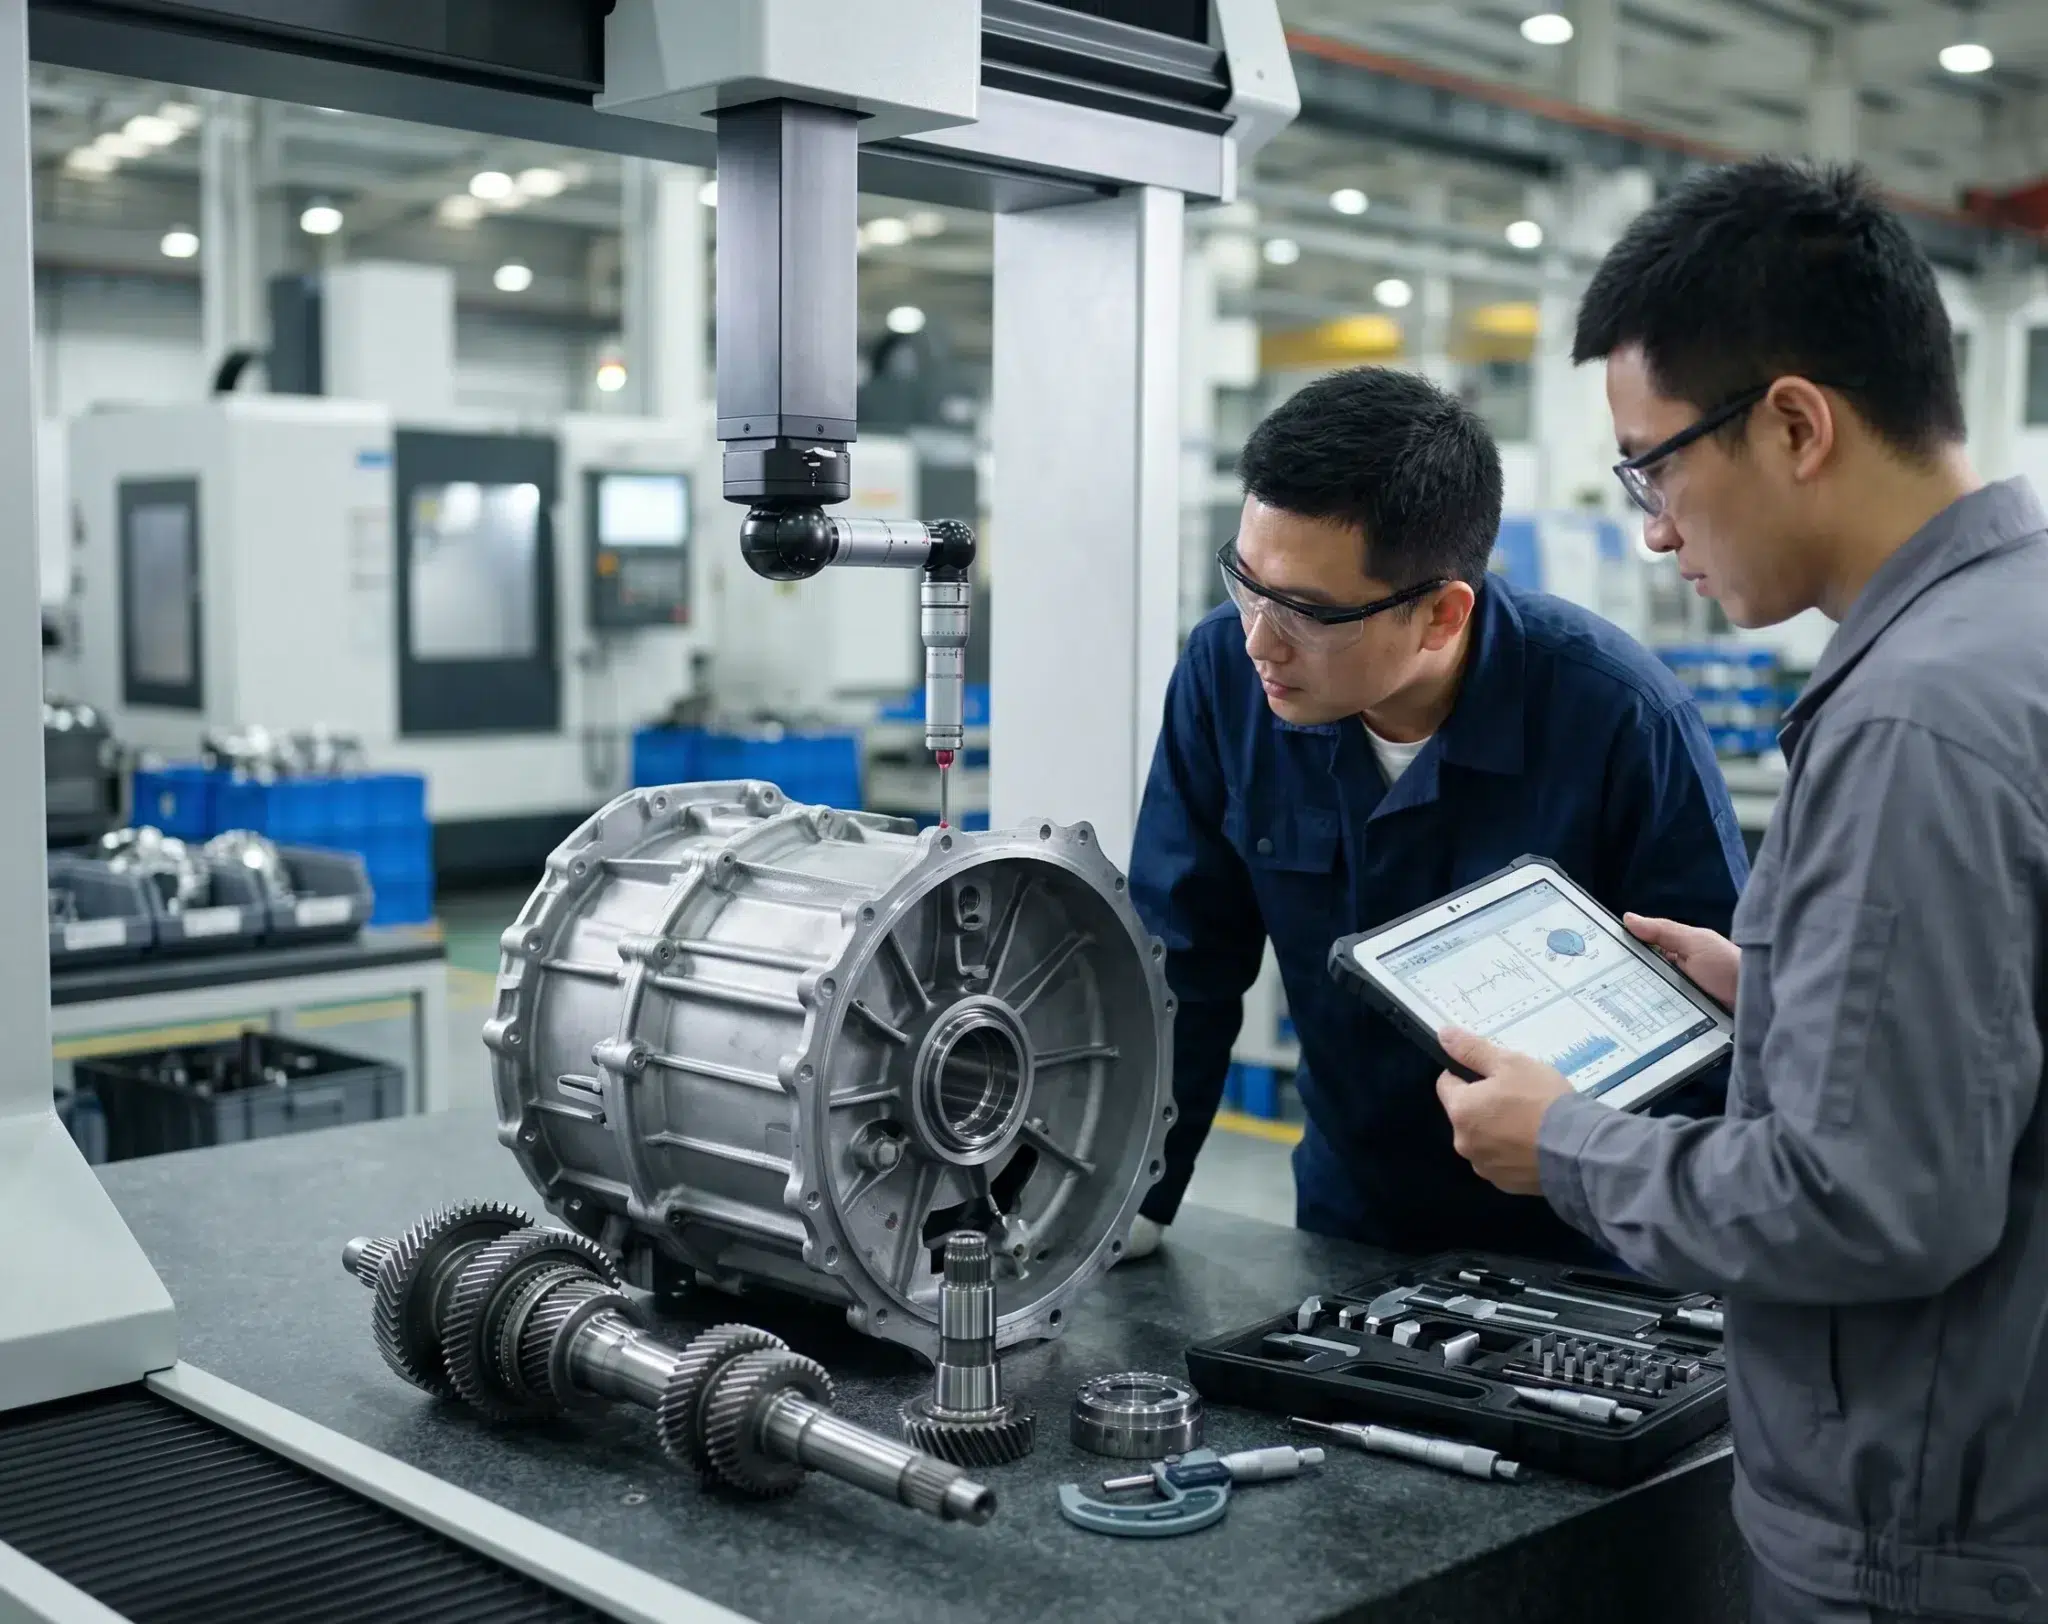
A machining process can look stable on the shop floor and still produce parts that get rejected at the customer’s dock. A tool offset entered a few thousandths off, a datum picked up from the wrong face, or a drawing note that nobody ballooned can send an entire lot back. An FAI exists to catch those problems on part number one, before the shop cuts the other 499. This guide explains what the check involves, when buyers require one, what goes inside the report, and how to run it without losing weeks of schedule.
What Is First Article Inspection?
An FAI is a documented verification that a part, produced with production tooling, production materials, and the production process, meets every requirement shown on the engineering drawing and in the purchase order. Each dimension, tolerance, note, material callout, and special process is checked and recorded with an actual measured result.
The word “first” points to the first part made under real production conditions, not a prototype cut on a different machine with temporary fixturing. That distinction matters, because the purpose is to validate the manufacturing process itself rather than one lucky sample.
In the aerospace and defense supply chain, the governing standard is AS9102, currently at Revision C. Automotive suppliers run a similar exercise under PPAP, and medical device and industrial buyers often ask for an equivalent report written to their own template. The documentation format changes between industries. The underlying logic does not.
What an FAI Is Not
- Not a prototype approval. Prototypes prove the design works. An FAI proves the process repeats.
- Not a batch sampling check. Sampling verifies a lot. An FAI verifies a setup.
- Not a replacement for in-process controls. It is the baseline those controls are measured against.
- Not a one-time event. Any change to how the part is made can trigger a new one.
Why FAI Matters for CNC Machined Parts
CNC machining is repeatable by nature, which is exactly why a setup error becomes expensive so quickly. Once a CAM program, fixture, and tool library are proven, the machine produces the same geometry hour after hour, including the same mistake.
A few common failure points show up again and again on machined parts:
- A work coordinate origin picked up from a face that shifts after the second operation
- Cutter compensation values that hold size on the first part and drift as the tool wears
- A 5-axis rotation that puts a hole within tolerance on position but out on perpendicularity
- A thin wall that measures correctly in the fixture and springs back once released
- A finish callout applied to the wrong surface during post-processing
Catching one of these on the first article costs a few hours of inspection time. Catching it after delivery costs scrap, rework, freight, a corrective action report, and usually a missed program date. For buyers sourcing precision components, the report is the clearest piece of manufacturing quality control evidence that a supplier’s CNC machining process is under control before volume begins.
When Is an FAI Required?
Most buyers call out the requirement in the purchase order. AS9102 defines the situations where aerospace suppliers must produce one, and other industries follow similar triggers.
| Trigger | Typical scope |
| First production run of a new part number | Full |
| Design change affecting form, fit, or function | Partial or full |
| Change of manufacturing source, plant, or supplier | Full |
| Change in process, tooling, or material | Partial |
| Change in numerical control program affecting geometry | Partial |
| Production lapse beyond two years | Full, or as the customer specifies |
Full Versus Partial FAI
A full FAI verifies every characteristic on the drawing. A partial, sometimes called a delta FAI, verifies only the characteristics affected by the change and references the approved baseline report for everything else.
Partial reports save time, but only when the baseline is clean and traceable. If the original has gaps, the customer will usually ask for full re-verification rather than accept a reference to incomplete data.
What Goes Into a First Article Inspection Report
Under AS9102, a first article inspection report is built on three forms, each answering a different question.
Form 1: Part Number Accountability
Identifies the part being inspected: part number, part name, revision level, drawing number, serial or lot number, the reason for the inspection, and any sub-assemblies that roll into the build. Every sub-component gets its own line with its own part number and revision.
Form 2: Product Accountability
Covers raw material, specifications, special processes, and functional testing. Typical entries for a machined part include the alloy and temper, heat treat condition, anodizing or plating specifications, and any proof or leak test called out on the drawing. Each line should point to where the requirement appears on the drawing or purchase order, so an auditor can trace it back to its source.
Form 3: Characteristic Accountability
The heart of the report. Every drawing characteristic gets a unique balloon number, and each balloon number gets a row recording the requirement, the measured result, and a conformance status. This is where dimensional inspection data lives, alongside notes, finish callouts, and general tolerance requirements that apply across the part.
The balloon numbers on the drawing and the characteristic numbers on Form 3 must match exactly. That link is what makes the report auditable.
Alongside the forms, a complete submission package normally includes the ballooned drawing or annotated 3D model, material certifications, special process certifications, the CMM output, and any functional test records.
The FAI Process Step by Step
The FAI process runs in a predictable sequence. Skipping ahead is where most delays start.
- Review the design data package. Confirm the drawing revision, the model, the purchase order flow-downs, and the customer’s report template before anything is cut.
- Balloon the drawing. Number every characteristic, including notes, general tolerances, surface finish symbols, and material callouts. Basic dimensions are not inspected directly, but the geometric tolerances that reference them are.
- Build the inspection plan. Assign a measurement method to each balloon and record the datum alignment strategy for geometric characteristics.
- Produce the part under production conditions. Production tooling, production fixturing, production material, and the same operator instructions the volume run will use.
- Measure and record actual values. Numbers, not checkmarks. A result of “pass” tells a reviewer nothing about where the feature sits in the tolerance band.
- Review and disposition. Any nonconformance needs a documented disposition before submission, not a blank row.
- Package and submit. Forms, ballooned drawing, certifications, and inspection data delivered together in the format the customer asked for.
Measurement Methods Used in Dimensional Inspection
The method has to match the tolerance being verified. A caliper is fine for a 0.5 mm general tolerance and useless for a 0.01 mm position callout.
| Characteristic | Common method | Notes |
| Linear dimensions, position, profile | Coordinate measuring machine | Requires correct datum alignment to the drawing |
| Small bores and pins | Bore gauge, pin gauge | Faster and often more repeatable than a probe |
| Threads | Go and no-go thread gauges | Records as attribute data, class noted |
| Surface roughness | Profilometer | Ra value with the sampling length recorded |
| Complex contours and organic shapes | 3D scanning | Color map plus extracted point data |
| Wall thickness on closed features | Ultrasonic gauge | Useful where a probe cannot reach |
Two details are worth controlling on any measurement. Work at a stable temperature close to 68 degrees Fahrenheit, since aluminum moves noticeably across a warm shop. And align to the drawing datums in the specified order, because a correct measurement taken from the wrong datum structure is still a wrong result. Suppliers that run this work in a climate-controlled metrology room with calibrated equipment, as described on the XC Machining facilities page, can defend their numbers when a customer re-measures.
Where FAI Reports Usually Get Rejected
Most rejections have nothing to do with the part. They come from the paperwork.
- Unballooned notes. Material specs, finish callouts, marking requirements, and general tolerance notes are characteristics too.
- Missing special process certifications. Anodizing, plating, heat treat, and welding all need evidence from an approved processor. Reviewing the surface finishing specifications early prevents a scramble at submission.
- Recorded results instead of measured values. Writing “OK” in the results column is the fastest way to get a report returned.
- Revision mismatch. The report cites Rev C while the purchase order calls out Rev D.
- Non-production conditions. The part was cut on a different machine or with fixturing the production run will not use.
- Missing material traceability. The certification does not tie back to the heat lot on the part. Confirming material certifications at the quoting stage avoids this entirely.
- No disposition for out-of-tolerance results. Nonconformances are acceptable when documented and approved. Silence is not.
How to Set Up a Smooth FAI With Your Machining Supplier
Expectations are cheapest to settle before the first chip is cut. A short conversation at the quoting stage prevents most FAI delays.
- Send the complete data package: model, drawing, purchase order notes, and any customer-specific flow-downs.
- State the standard, revision, and template format you expect for submission.
- Agree on who balloons the drawing and who owns the inspection plan.
- Ask to see a redacted sample FAI report before awarding the work.
- Build inspection time into the schedule. A full report on a complex part is days of work, not hours.
- Decide up front who has authority to disposition a nonconformance.
Suppliers that treat first article work as a normal part of production, with documented procedures and a defined quality assurance process, tend to submit cleaner reports and clear customer review faster. That matters most in regulated markets, where aerospace and medical programs will not release production until the report is approved. Teams sourcing machined components for those programs can review capabilities and inspection support directly with XC Machining before releasing a first article order.
FAQs
Q: How long does an FAI take?
A simple machined part with 20 to 40 characteristics usually takes one to two days, including measurement and documentation. Complex aerospace components with several hundred ballooned features can take a week or more, depending on fixturing and review time.
Q: Who pays for the FAI report?
The buyer normally absorbs the cost, either as a separate line item or built into the first article part price. Suppliers should quote it openly, since a full report on a complex part carries real engineering and metrology hours.
Q: Is an FAI required for non-aerospace CNC parts?
Not by regulation, but many industrial, medical, and energy buyers request one. Automotive programs use PPAP instead. Even without a customer requirement, running the FAI process internally is a practical manufacturing quality control step before committing to a volume run.
Q: What happens if a dimension fails during dimensional inspection?
The nonconformance is documented on Form 3 with the actual value and submitted for disposition. The customer may accept it as is, request rework, or require a process correction and a re-inspection before approving the report.
Q: Does a new revision always require a full FAI?
No. If the change affects only specific characteristics, a partial or delta report covering those features is usually acceptable, provided it references an approved baseline report. Changes to manufacturing source or a production lapse beyond two years typically require a full FAI.