Home - Selective Laser Sintering (SLS)

SLS 3D Printing Services

XC Machining provides SLS 3D printing for US product teams. A CO2 laser sinters PA12, PA11, glass-filled nylon, TPU and PP powder at 100 to 150 μm. Parts need no supports and hold ±0.3 mm. First parts ship in 2 to 5 business days with no tooling.

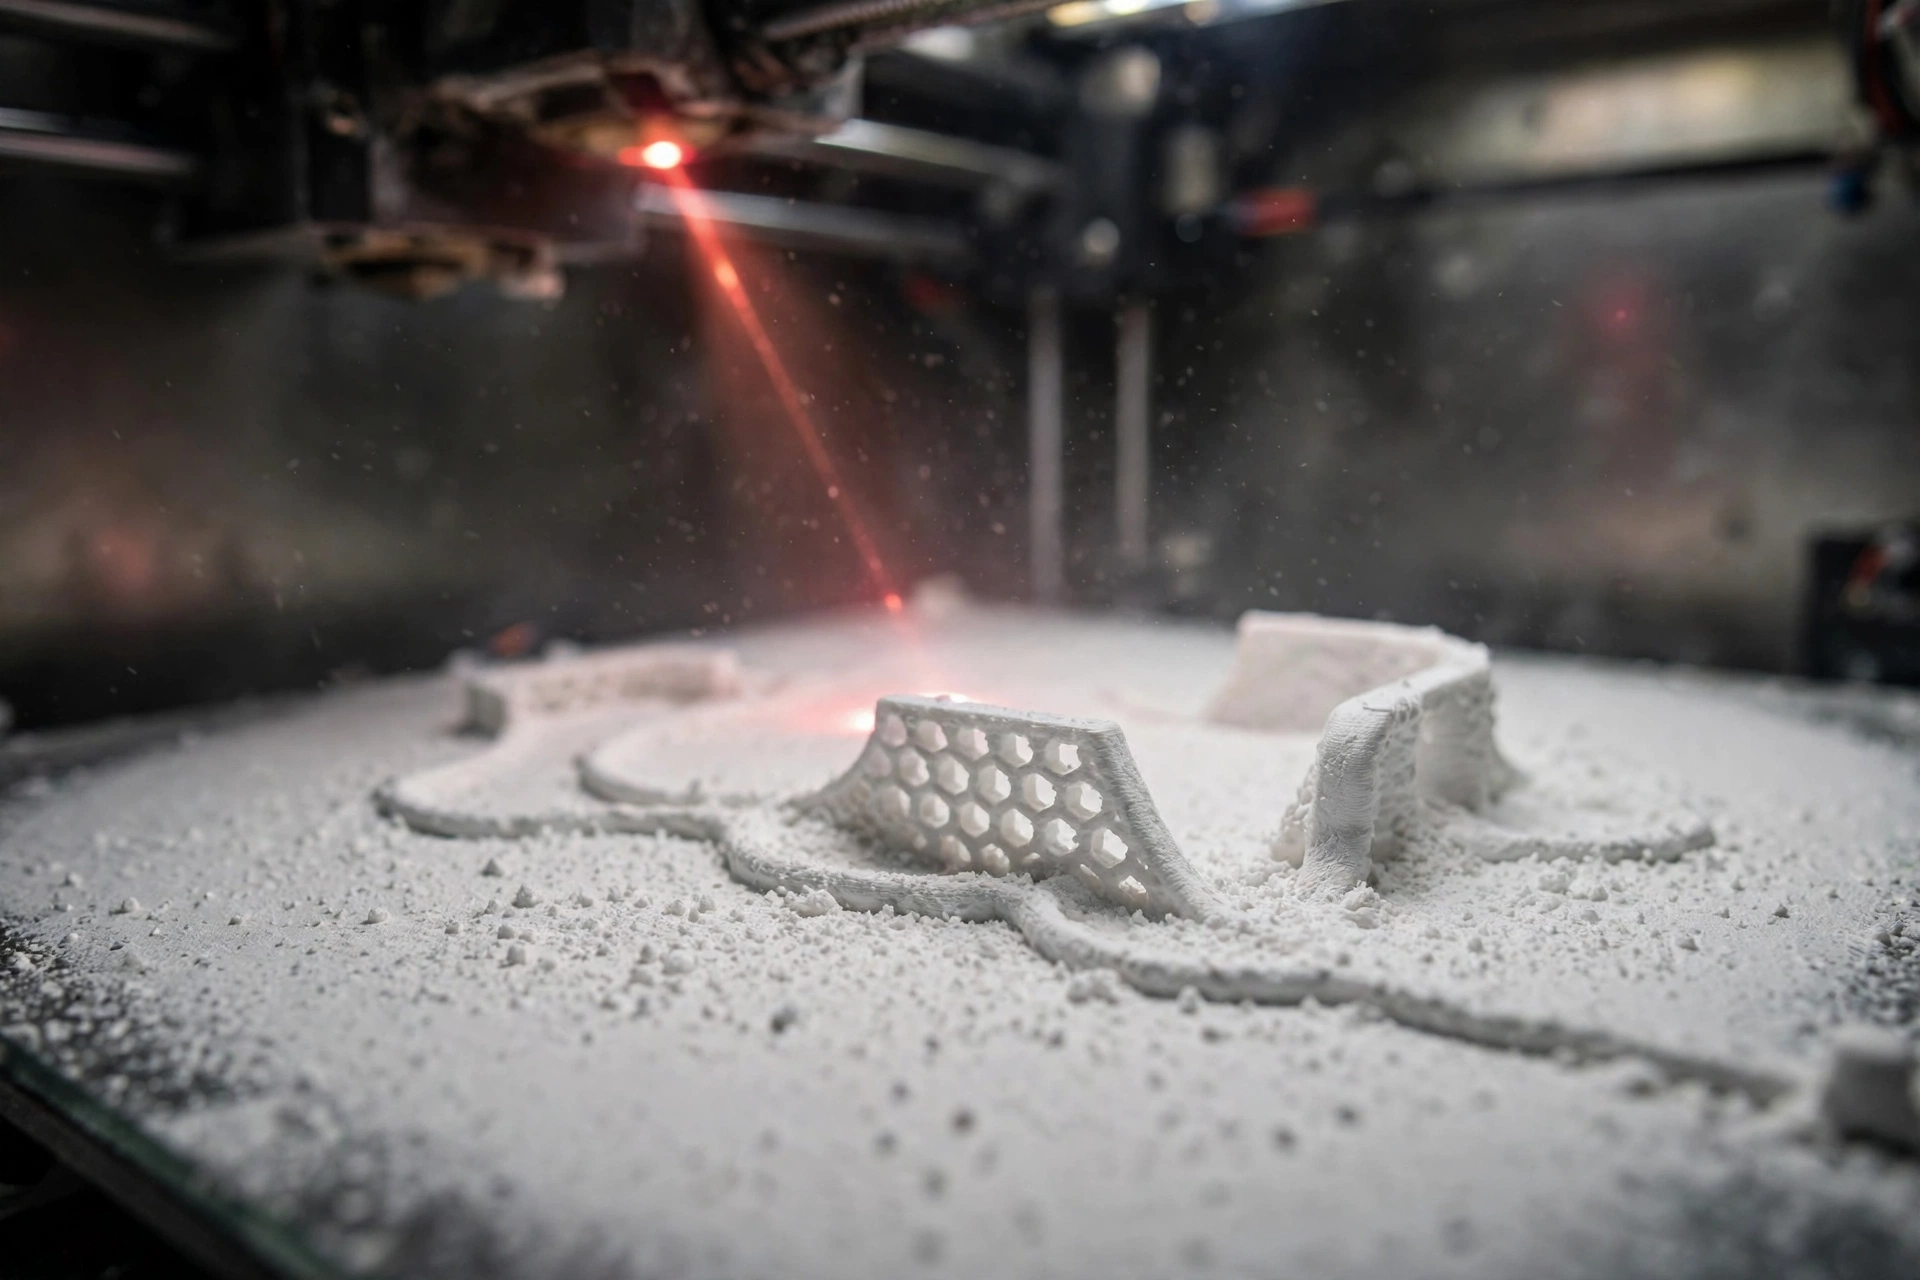
SLS 3D printer build chamber: CO2 laser scanning white nylon powder bed with sintered lattice parts emerging
Selective Laser Sintering (SLS) - XC Machining

What Is SLS 3D Printing at XC?

Selective laser sintering is a powder bed fusion process. A CO2 laser fuses nylon powder one layer at a time, 100 to 150 μm thick. Unsintered powder holds the part in place during the build.

That powder bed is why SLS prints complex shapes without supports. It also gives parts with near-equal strength in all three axes.

SLS Support for US Product Teams

XC Machining serves US teams from its Dongguan factory. Our engineers advise on material, accuracy and finish for each SLS part. Parts ship worldwide by DHL, FedEx or UPS, and the quote comes back within 12 hours.

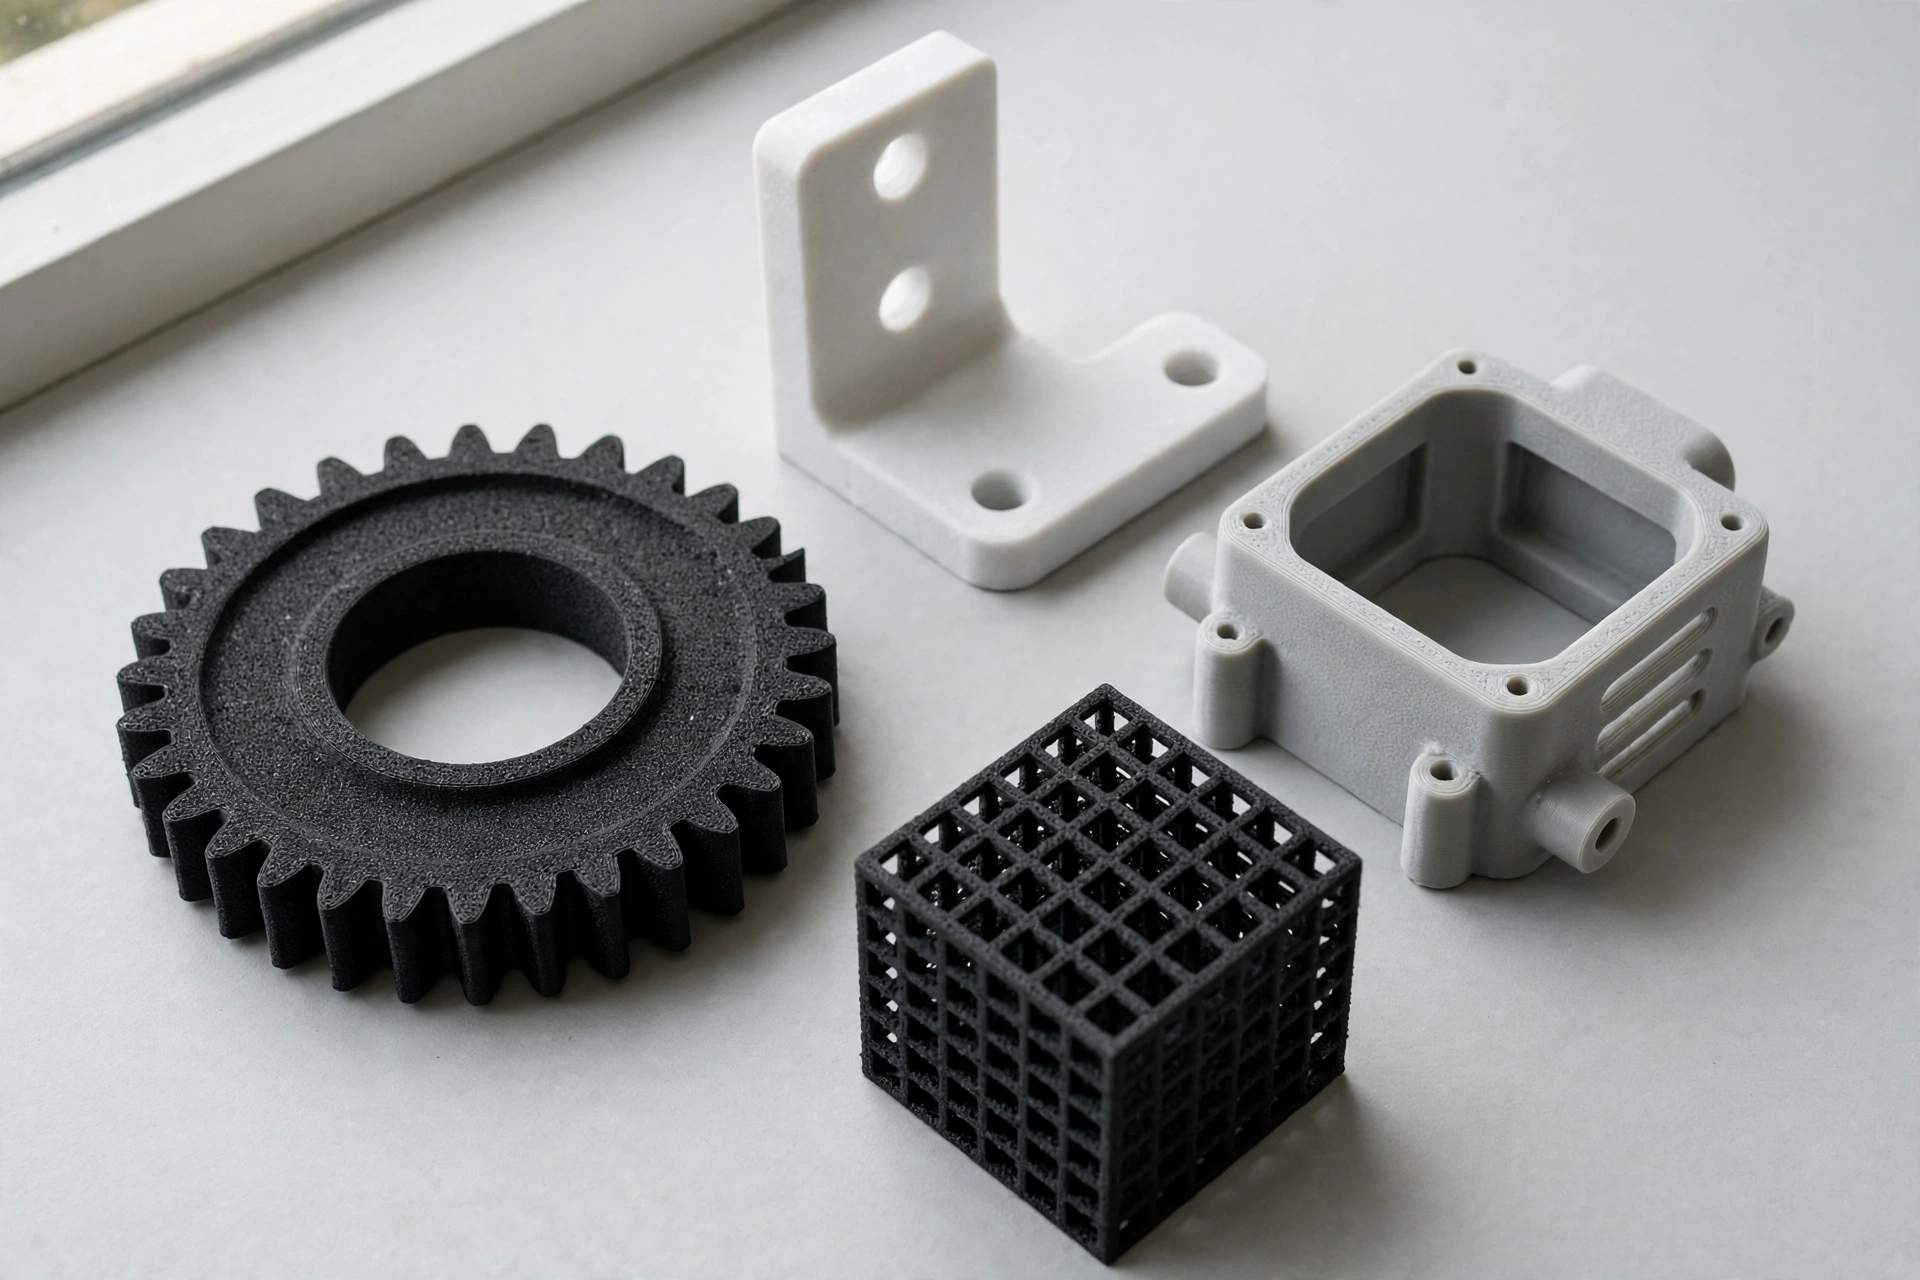
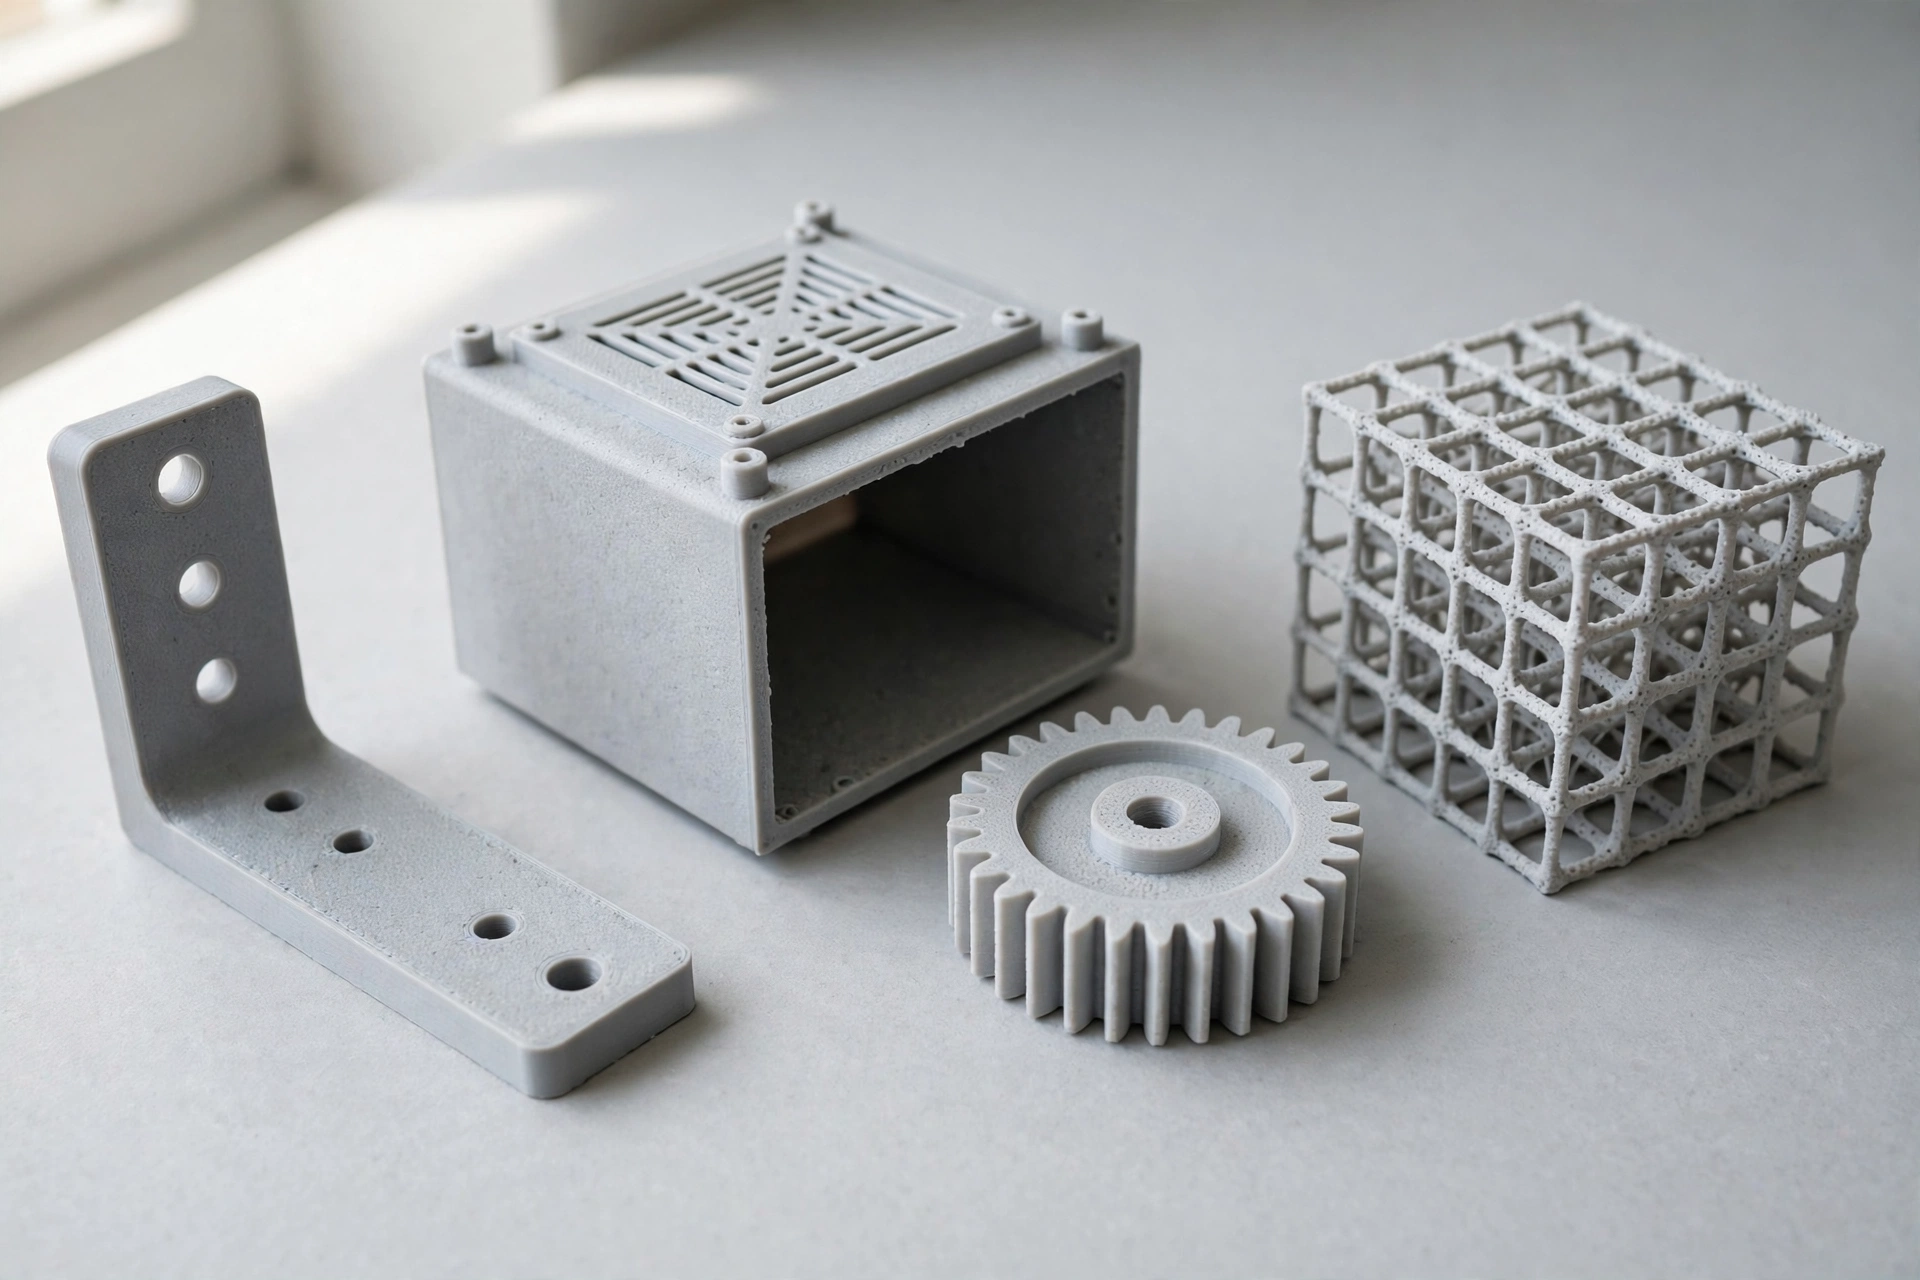
SLS 3D printed nylon functional parts: bracket, housing enclosure, gear and lattice structure in light gray PA12

SLS 3D Printing Tolerances

Accuracy depends on the material and the shape of the part. The table lists the limits we work to.

ItemSpecification
Precision tolerances±0.2 mm for most parts, with finer values possible on small geometry
Layer resolutionAs fine as 0.1 mm, depending on material and printer setup
Minimum wall thickness1 mm, depending on material and part design
Minimum feature size0.5 mm, varies by material
Maximum part sizeUp to 600 × 600 × 500 mm, depending on machine capacity
Minimum part sizeAs small as 5 × 5 mm, depending on printer and material
Production volumeLow volume 1 to 100 pieces, high volume 100 to 2,000, large volume 2,000 or more
Lead time5 to 7 business days for most orders, faster for simple designs

SLS Design Rules at a Glance

Follow these limits and the DFM review passes faster. Each one comes from the checks XC runs on every file.

RuleLimitWhy it matters
Wall thicknessAt least 1.0 mmThin walls fail in depowdering
Internal channel clearanceAt least 2.0 mmLoose powder must drain out
Feature sizeAt least 0.5 mmSmaller detail does not resolve
Sealed cavitiesAdd an exit holeTrapped powder cannot escape
Large flat or thin featuresAsk for an orientation checkThey warp most easily
Build volume340 × 340 × 600 mmLarger parts print in pieces
Tolerance±0.3 mm or ±0.5%, the largerSets what you can specify

If a design needs finer surface or faster batches, MJF 3D printing uses the same nylon with a different heat source.

Why Choose XC for SLS Printing

XC SLS parts hold ±0.3 mm in PA12, PA11, PA12-GF, TPU and PP powder, with 100 to 150 μm layers and no supports. The build volume is 340 × 340 × 600 mm. DFM review takes 12 hours, and parts ship in 2 to 5 business days.

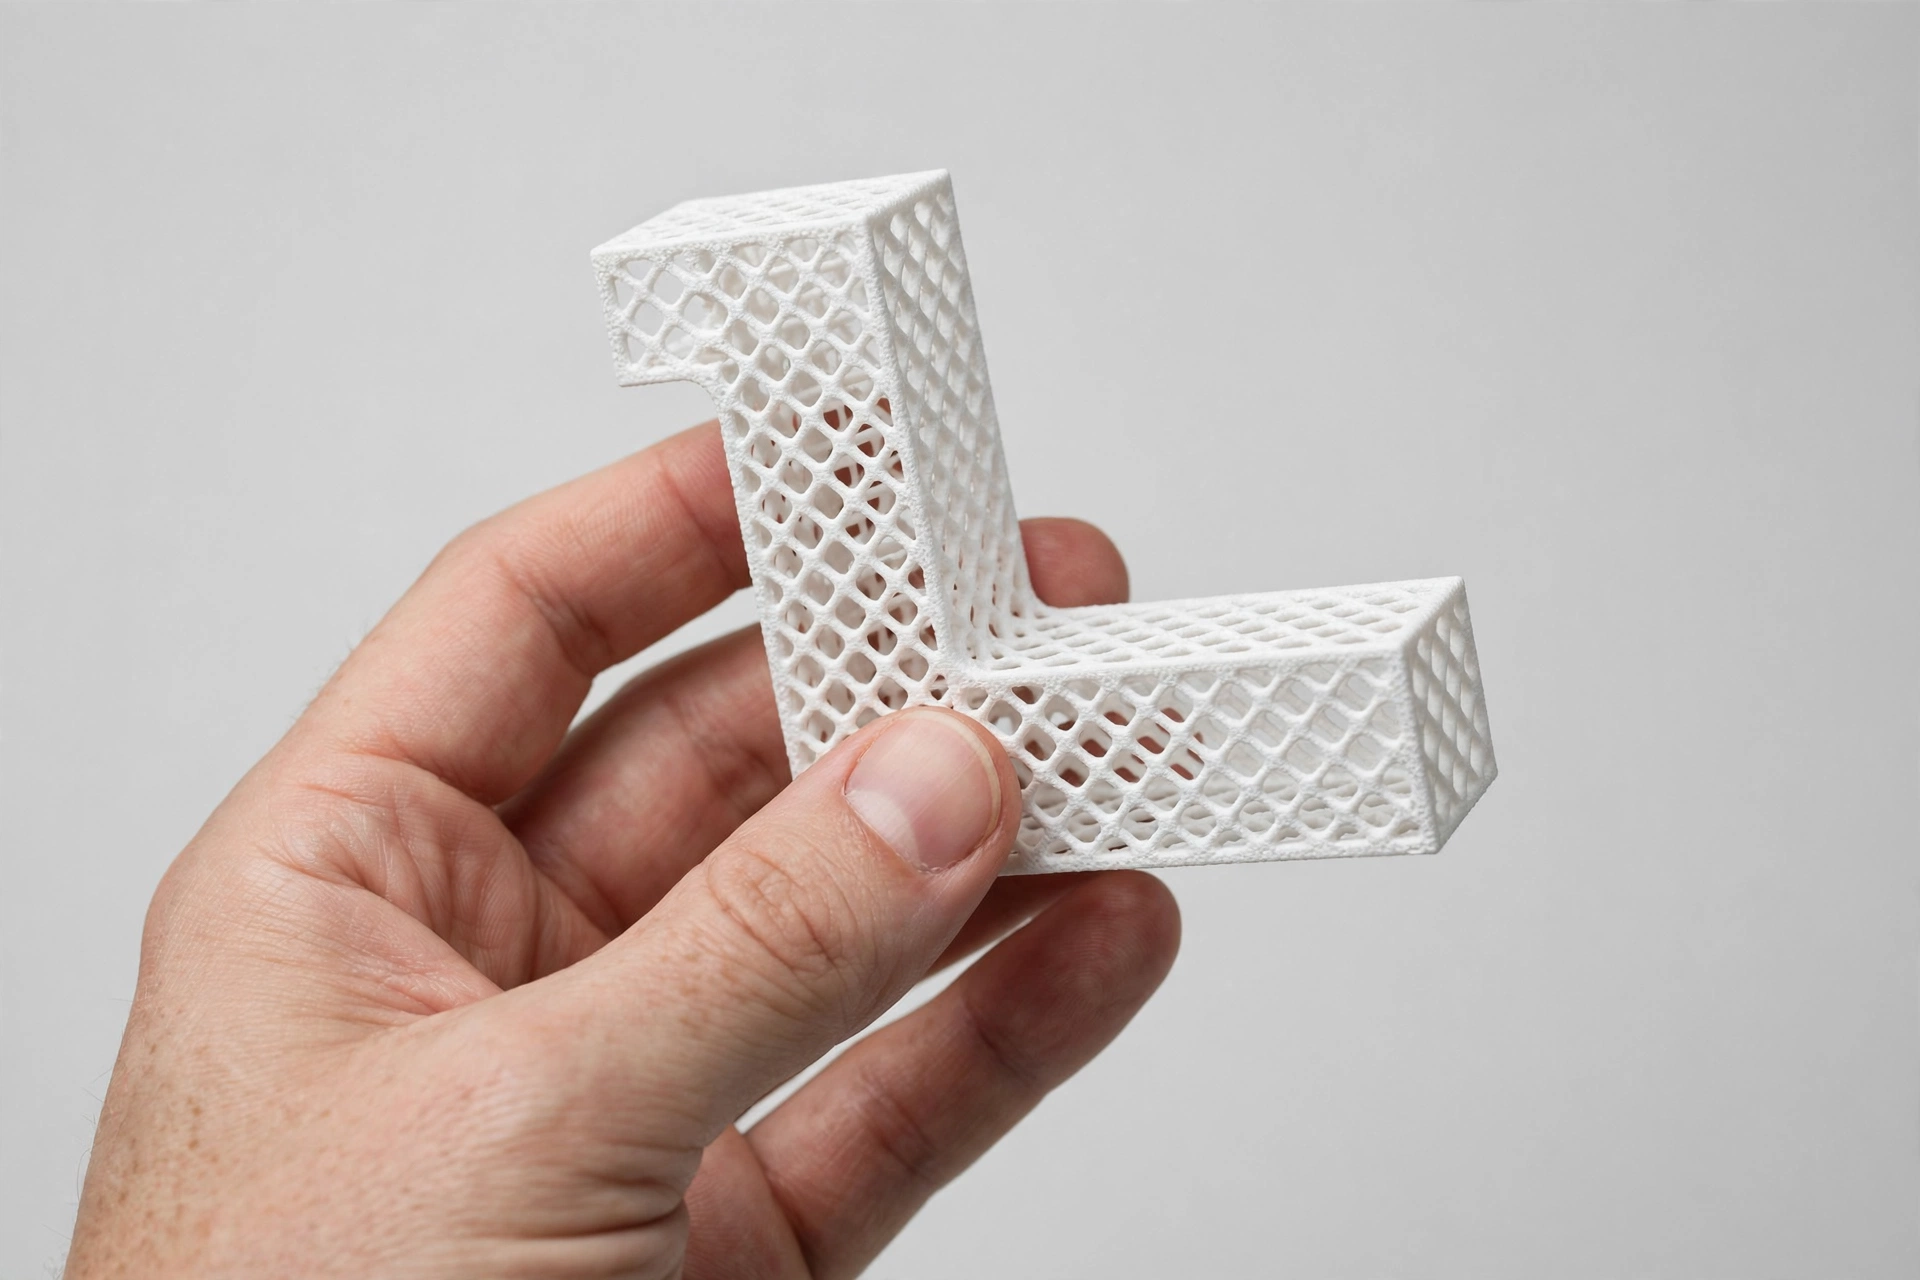
Hand holding a white SLS 3D printed nylon lattice bracket
Selective Laser Sintering (SLS) - XC Machining
No Supports Needed

The powder around the part holds it up, so internal channels, undercuts, lattices, interlocking assemblies and moving hinges print in one build. There are no support marks and no removal labor. That is the main edge SLS has over SLA and FDM on complex parts.

Selective Laser Sintering (SLS) - XC Machining
Dense Nesting Cuts Part Cost

Parts nest in 3D through the full build volume, from one prototype to hundreds of production pieces. Cost per part falls with quantity. A build of 50 parts costs 60 to 70% less per unit than a build of 5.

Selective Laser Sintering (SLS) - XC Machining
Strength in Every Direction

Sintering bonds powder in all directions, so tensile strength, elongation and fatigue resistance match in X, Y and Z. PA12 reaches 48 MPa tensile in both XY and Z. FDM parts are weaker in Z and can fail under multi-direction load.

Selective Laser Sintering (SLS) - XC Machining
DFM Review Within 12 Hours

Upload an STL or STEP file. Engineers check wall thickness, channel clearance for depowdering and trapped volume. They also recommend a build orientation and a material, PA12, PA11, TPU or PP, for your load, heat and chemical needs.
Finishes for SLS Printed Parts

SLS parts come off the build with a grainy matte surface. The table shows what XC offers. Our surface finishing page covers other options for printed parts.

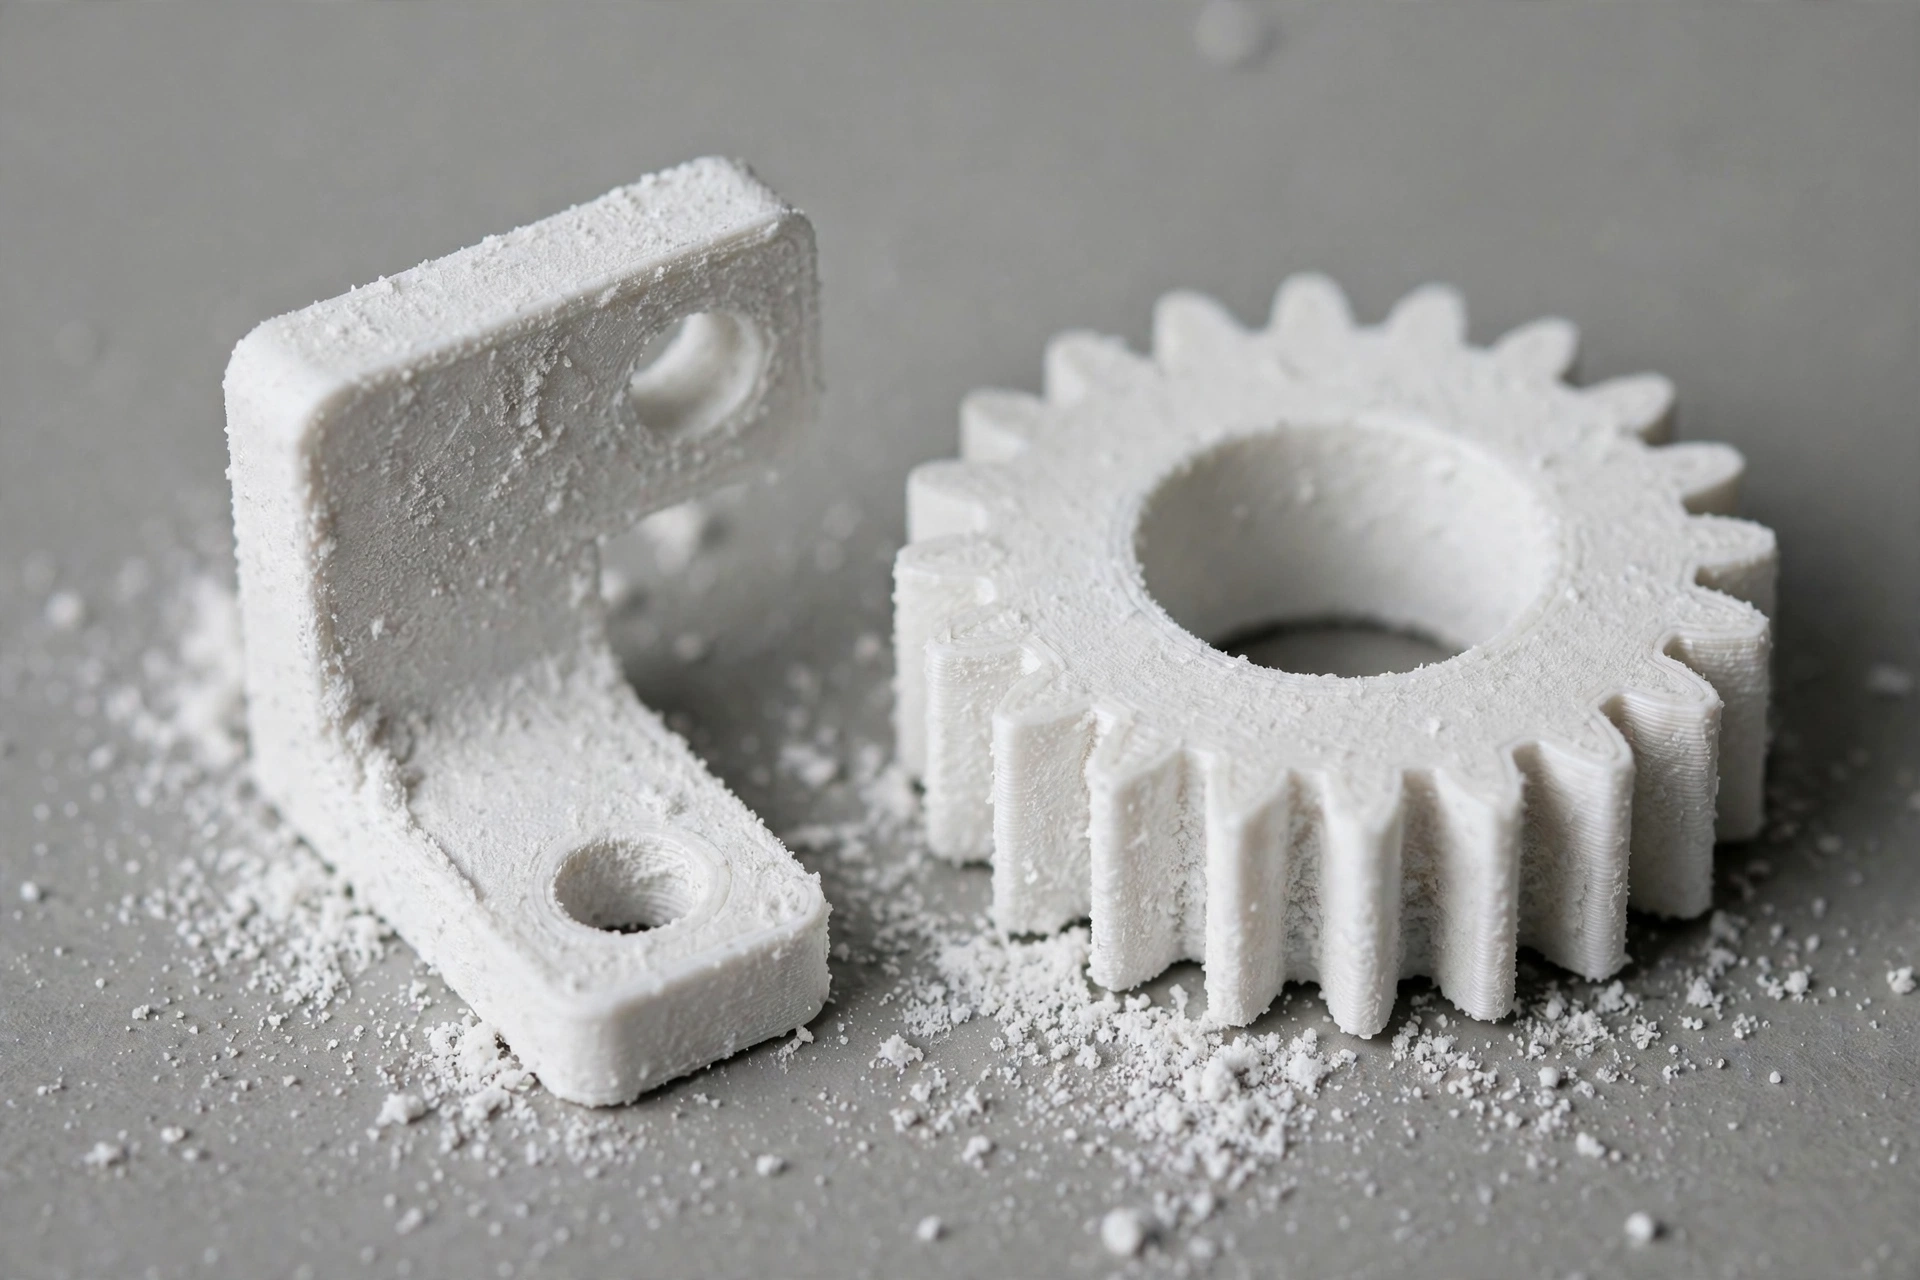
White SLS 3D printed nylon parts fresh from the build with grainy matte powdery surface texture
As printed

As printed to Ra 6 to 12 μm. Grainy matte, natural white or gray PA12 or black PA11. Suits fit tests and internal parts

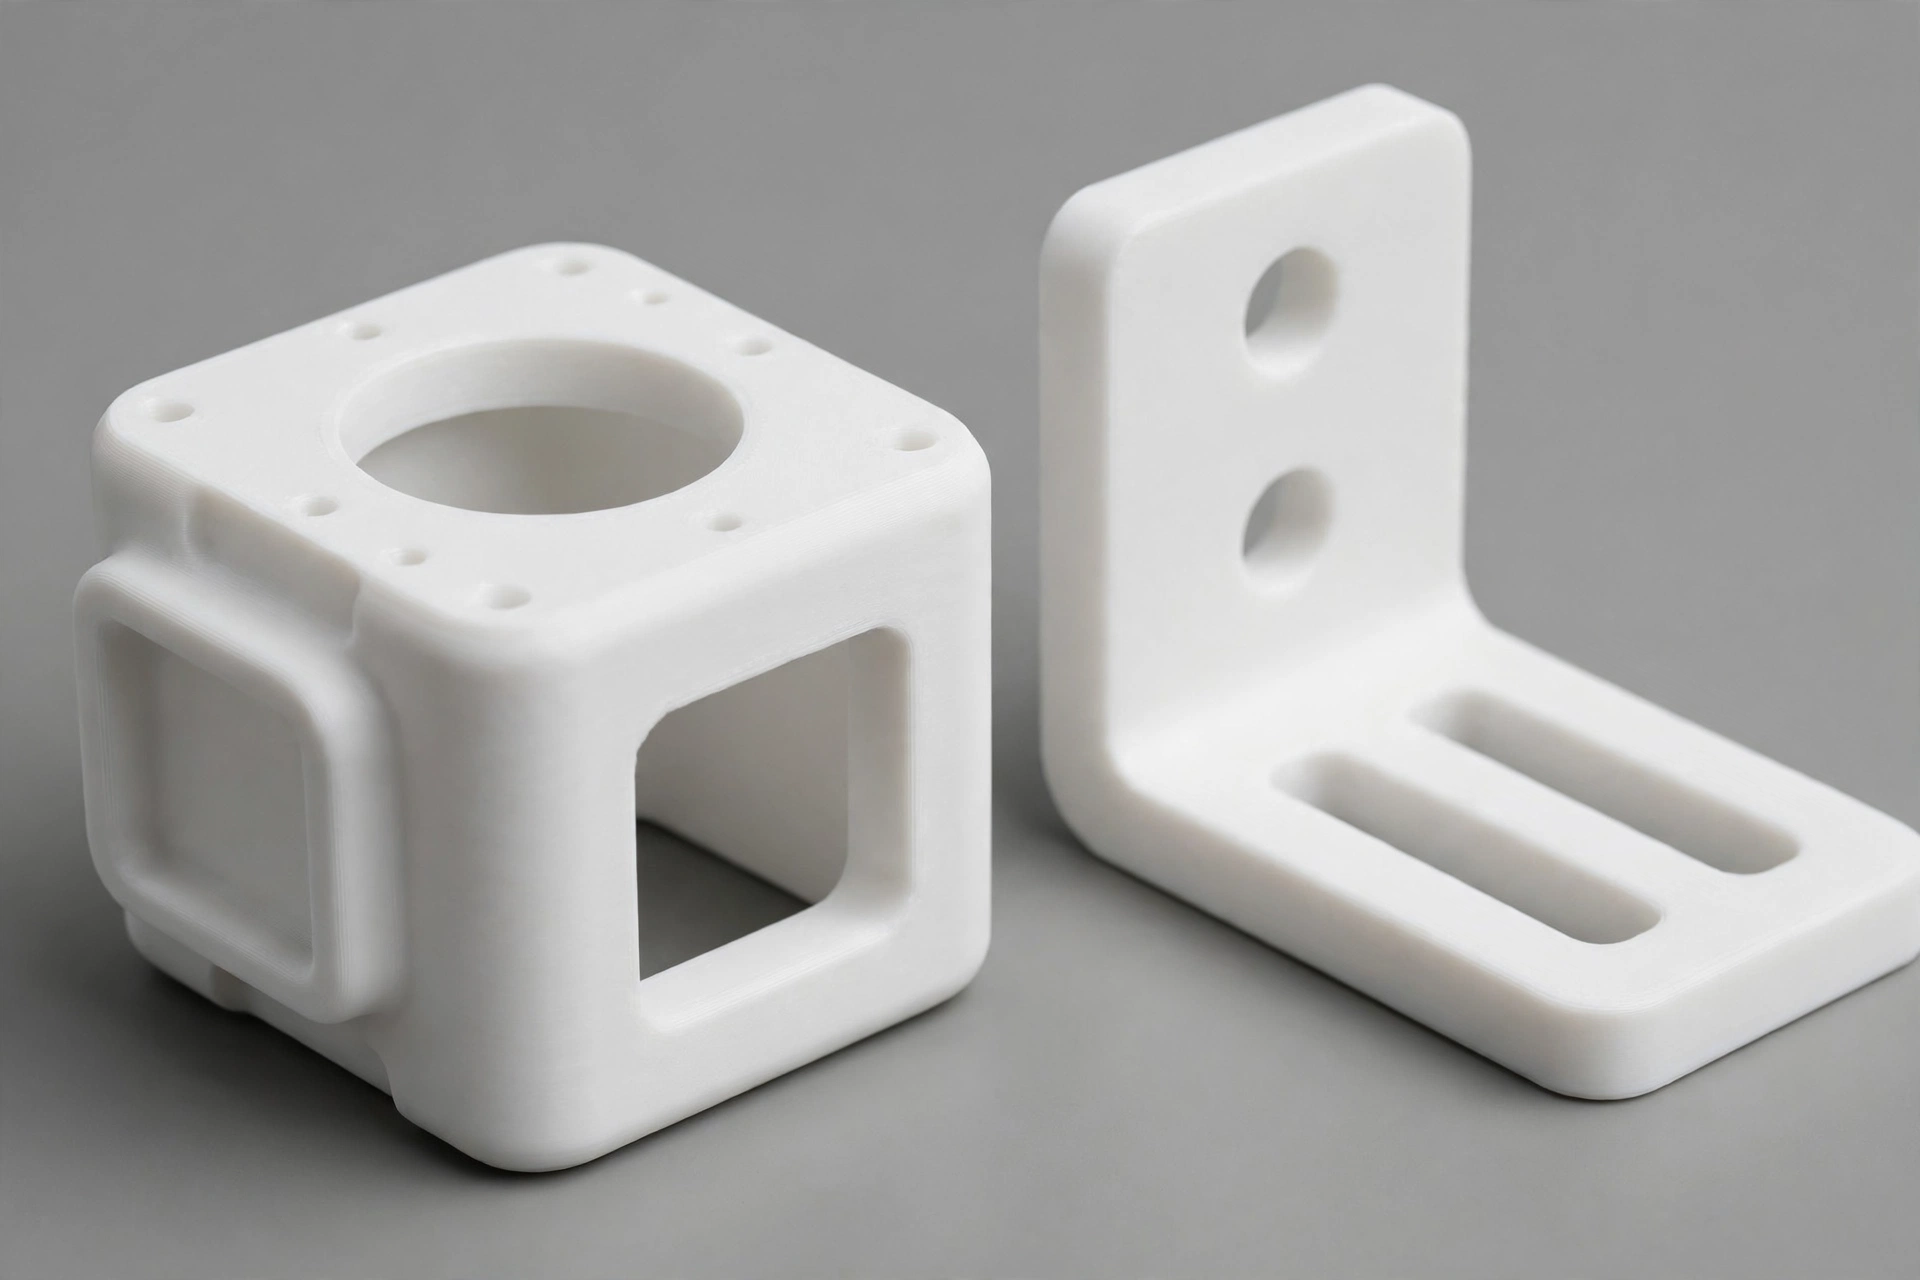
White SLS 3D printed nylon parts after glass bead blasting with uniform smooth matte surface
Bead blasting

Bead blasting to Ra 4 to 8 μm. Standard on all SLS parts before other steps. Removes up to 0.1 mm on critical features

Selective Laser Sintering (SLS) - XC Machining
Dyeing

Dyeing to Ra 4 to 8 μm. Color soaks 0.3 to 0.5 mm deep in black, blue, red, green or yellow. It will not chip

Selective Laser Sintering (SLS) - XC Machining
Painting

Painting to Ra 1.6 to 3.2 μm. Primer and polyurethane or epoxy topcoat, 60 to 120 μm, in RAL or Pantone colors

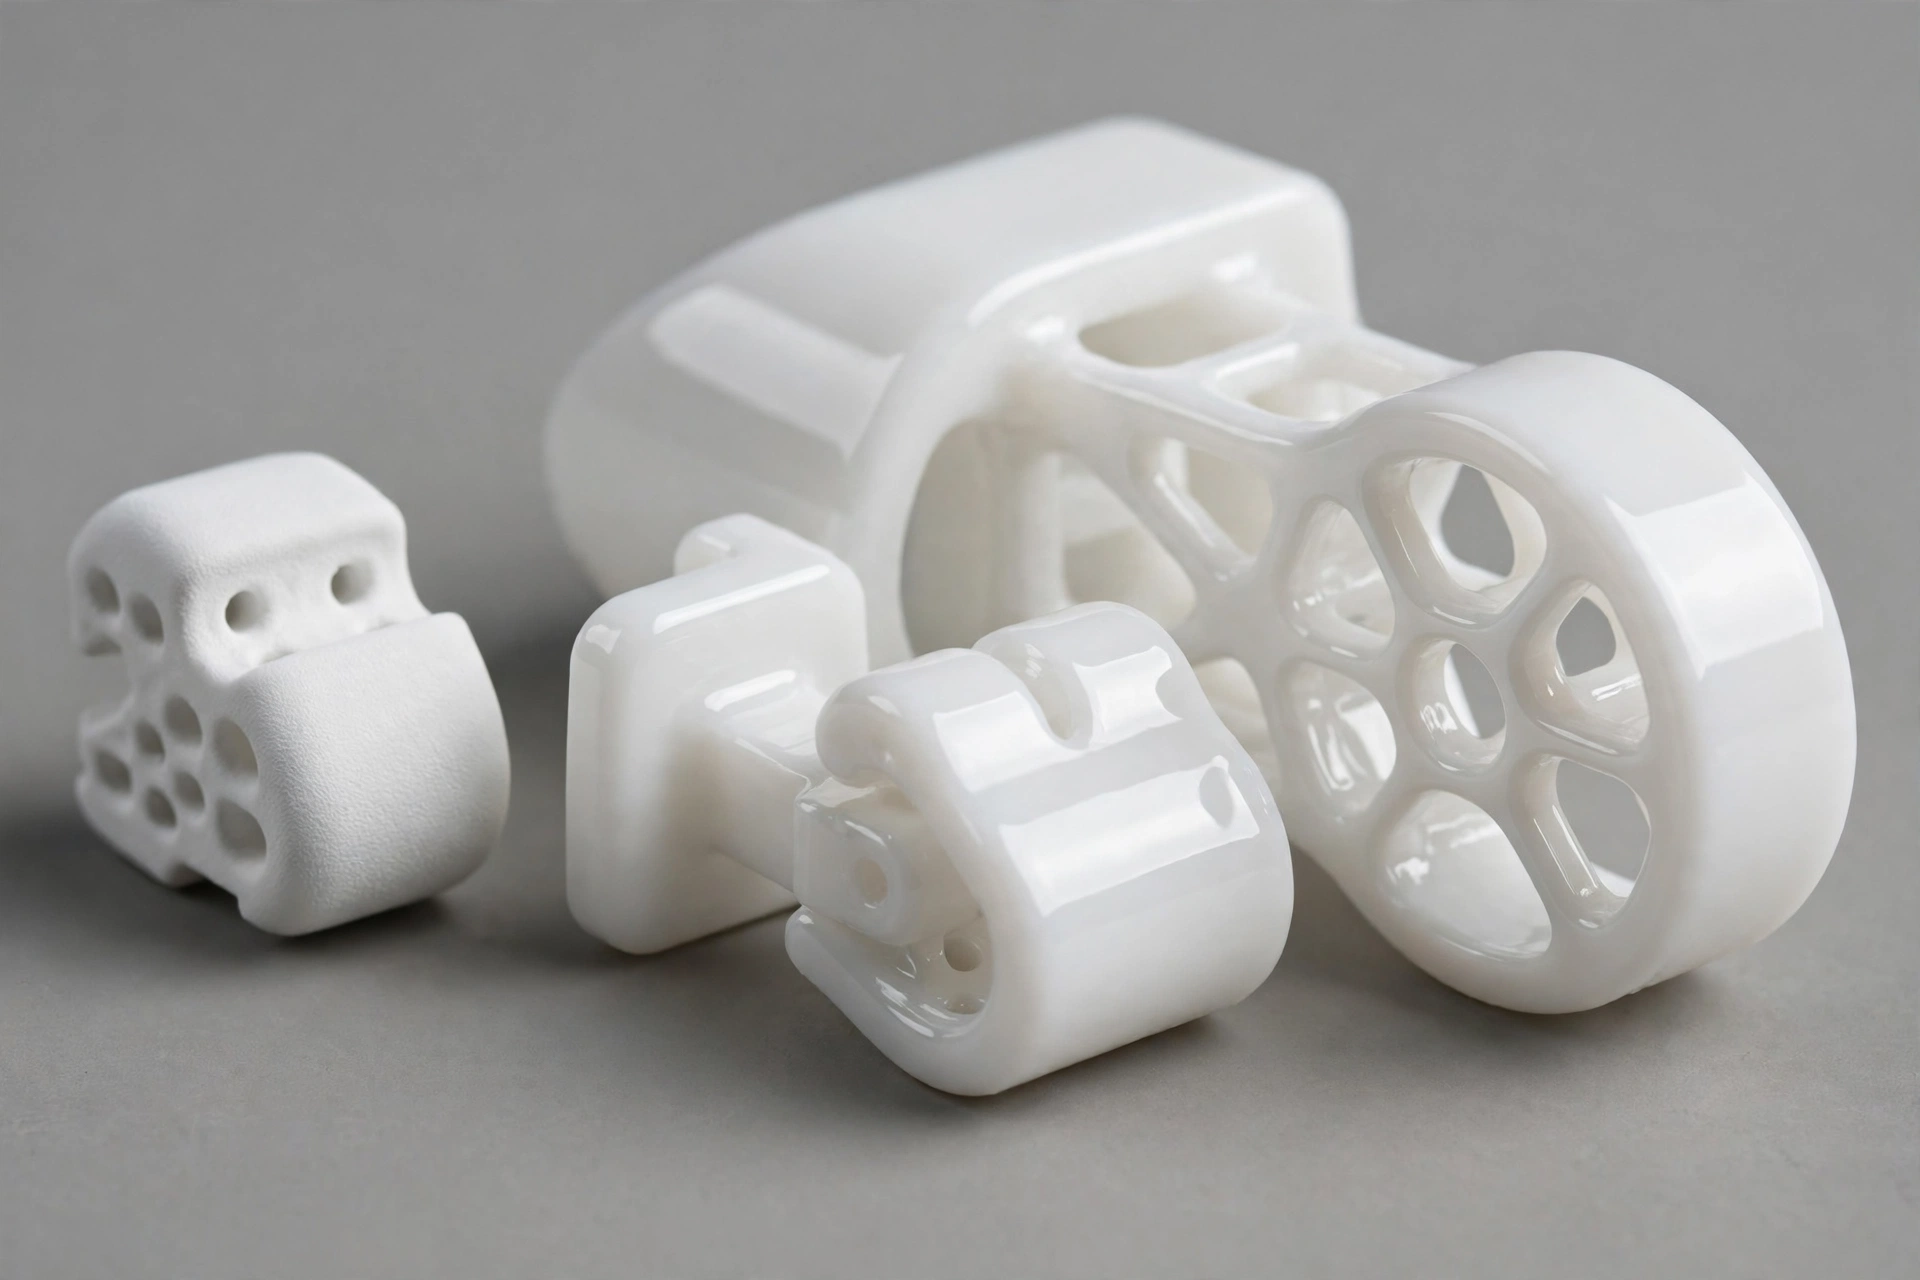
White SLS 3D printed nylon parts after vapor smoothing with glossy sealed surfaces next to a matte bead-blasted part
Vapor smoothing

Vapor smoothing to Ra 1 to 2 μm. Semi-gloss sealed surface for PA11 and PA12. Shifts critical features 0.05 to 0.15 mm

Black parts come two ways. PA12 is dyed after printing, and PA11 Black is pre-pigmented. XC supplies both.

SLS Nylon Powders We Print

Seven nylon grades cover most functional needs. Request the powder datasheet before you design to a strength figure. Our materials page lists every process.

Nylon 12 (PA12)

PA12, also sold as PA 2200, is the durable general purpose grade. It reaches 48 MPa tensile and 18% elongation.

Nylon 12 Glass-Filled (GF)

PA12 GF, or PA 3200 GF, holds 40% glass for stiffness at higher temperature. It reaches 60 MPa tensile.

Nylon 11 EX (PA11)

PA11 is a ductile, bio-based grade sold as Rilsan Invent Natural. It reaches 48 MPa tensile and 40% elongation.

Nylon 12 Carbon-Filled (CF)

Carbon-filled PA12, or PA 602-CF, is a high-performance stiff grade.

Nylon 12 Aluminum-Filled (AF)

Aluminum-filled PA12, or alumide, gives a metallic gray part.

Nylon 12 Mineral-Filled (HST)

Mineral fiber-reinforced PA12, or PA 620-MF, is the heat-resistant grade.

Nylon 12 Flame Retardant (FR)

PA 606-FR meets the FAR 25.853 60-second burn spec. The FAQ lists a UL 94 V-0 rating for flame retardant PA12.

XC also prints TPU, a flexible grade at Shore A 80 to 95 with 350% elongation, and PP, a chemical-resistant semi-flexible grade at 22 MPa. All powders sinter in a nitrogen atmosphere.

SLS 3D printed nylon parts in white, gray and black: gear, bracket, housing and lattice cube in PA12, PA11 and glass-filled nylon

Our Selective Laser Sintering (SLS) Prototype Manufacturing Capabilities

As a leader in precision manufacturing, we offer a wide range of capabilities that cater to both one-off prototyping and low-volume production. We specialize in delivering geometrically complex and highly cosmetic parts, ensuring the highest quality standards. At XC Machining, we pride ourselves on being the go-to manufacturer for all your Selective Laser Sintering (SLS) needs, providing reliable and efficient solutions under one roof.
With 3, 4, and 5-axis CNC machining services, we can produce complex prototypes and parts with precise tolerances. More than 60+ materials are available for you to choose from.

Provides injection molding for prototypes and custom parts, emphasizing expert support, competitive pricing, and faster production cycles.

Get reliable vacuum casting services for high-quality prototypes and production parts at competitive prices. XC Machining offers highly detailed casting parts with consistent quality.

Uses cutting, bending, and forming techniques to produce precision metal components suited for industrial, commercial, and manufacturing applications.

Specialist Industries

XC Machining is a trusted partner for industries demanding complexity, reliability and precision. Our extensive experience in producing millions of high quality components brings unmatched expertise to every project. Our services cover a diverse range of applications to ensure that we meet the unique needs of each sector with great care.
Get In Touch

Bring Your Designs to Life with XC Machining

Experience precision engineering with XC Machining. From detailed prototypes to high-volume production, we’re here to turn your concepts into reality. Contact us today to discuss your project needs!

Get In Touch With Us!
Prompt response guaranteed within 12 hours

SLS 3D Printing FAQs

XC holds ±0.3 mm or ±0.5% of the nominal size, whichever is larger. A 100 mm feature gets ±0.5 mm, and a 20 mm feature gets ±0.3 mm. Z-axis tolerance is the same. Geometry matters, because large flat parts and thin features warp most easily.

No. Unsintered powder surrounds the part and supports overhangs, bridges, channels and undercuts during the build. That removes support cleanup and witness marks. It also lets SLS print internal channels, lattices and moving hinges that SLA and FDM cannot make without support damage. Parts come out of the powder cake ready to clean.

XC prints PA12 at 48 MPa tensile and 18% elongation, and PA11 at 48 MPa and 40% elongation. PA12-GF with 40% glass reaches 60 MPa. A flame retardant PA12 is rated UL 94 V-0. TPU runs Shore A 80 to 95 with 350% elongation, and PP gives 22 MPa with chemical resistance.

Prototype quantities of 1 to 20 parts ship in 2 to 5 business days. Production batches of 50 to 500 or more parts take 5 to 10 days, including build planning and depowdering. Rush delivery of 1 to 3 days covers simple PA12 parts from a pre-scheduled build. The DFM review and quote arrive within 12 hours of upload.

Both are powder bed fusion processes in PA12 with no supports and ±0.3 mm tolerance. MJF uses an inkjet fusing agent and an infrared lamp, which gives a finer surface at Ra 4 to 6 μm and faster builds. SLS runs Ra 6 to 12 μm but offers PA11, TPU, PP and flame retardant grades.

The SLS build volume is 340 × 340 × 600 mm. One part can fill it, or hundreds of small parts can nest inside. Larger parts print in pieces and join with structural adhesive or fasteners. Parts beyond 600 mm suit large-format FDM, which builds up to 914 × 610 × 914 mm.

Choose SLS below 500 units, since injection tooling costs $5,000 to $50,000. Choose it while the design still changes, because SLS has no tooling change cost. It also fits needs of 2 to 5 days, against 25 to 35 days for a mold. Above 1,000 units a year, injection molding wins on price.

CNC Manufacturing Resources