Metal Bending Services
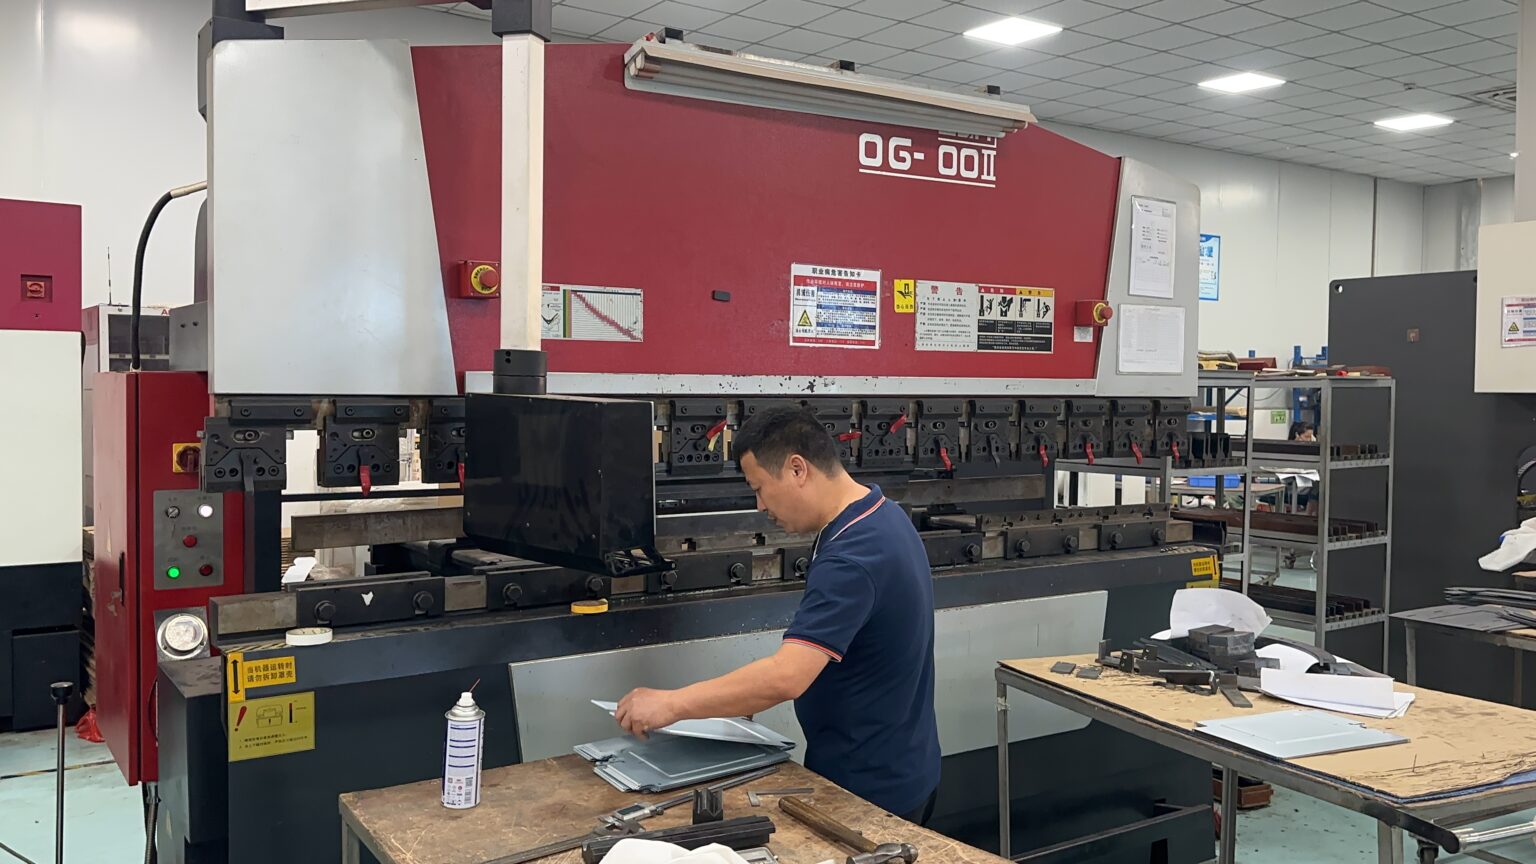
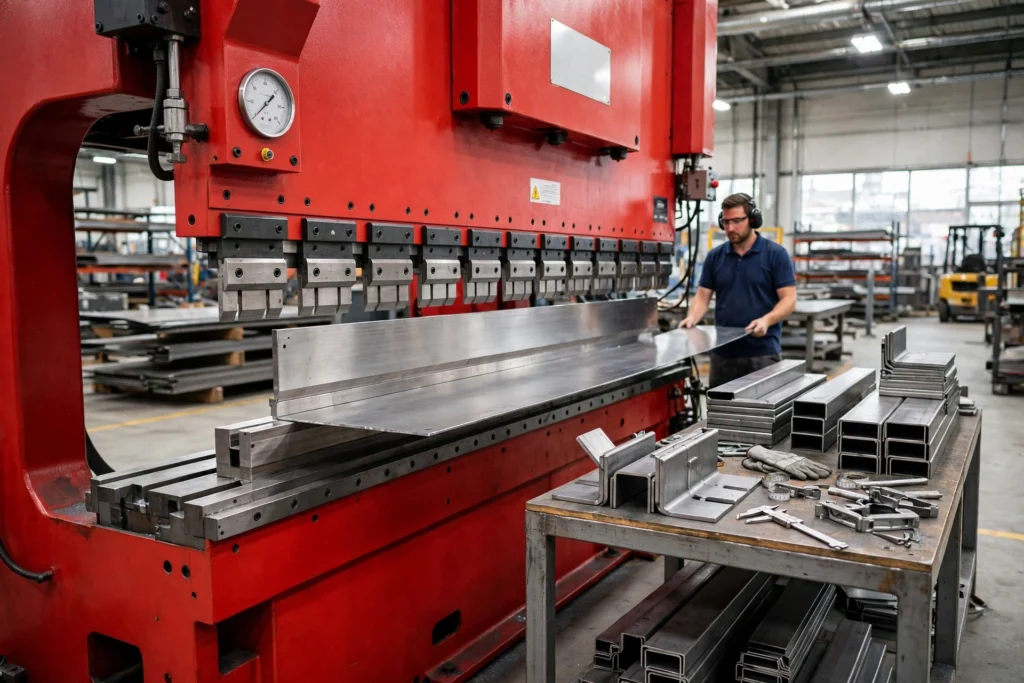
XC Machining provides CNC press brake metal bending for US product teams. We bend steel, stainless steel, aluminum, copper, brass and titanium sheet from 0.5 to 12 mm thick. Presses reach 250 tons across 3200 mm, with ±0.1° angular accuracy and a 1× thickness standard bend radius.
All uploads are secure and confidential.
- All uploads are secure and confidential
What Bending Can Our Press Brakes Do?
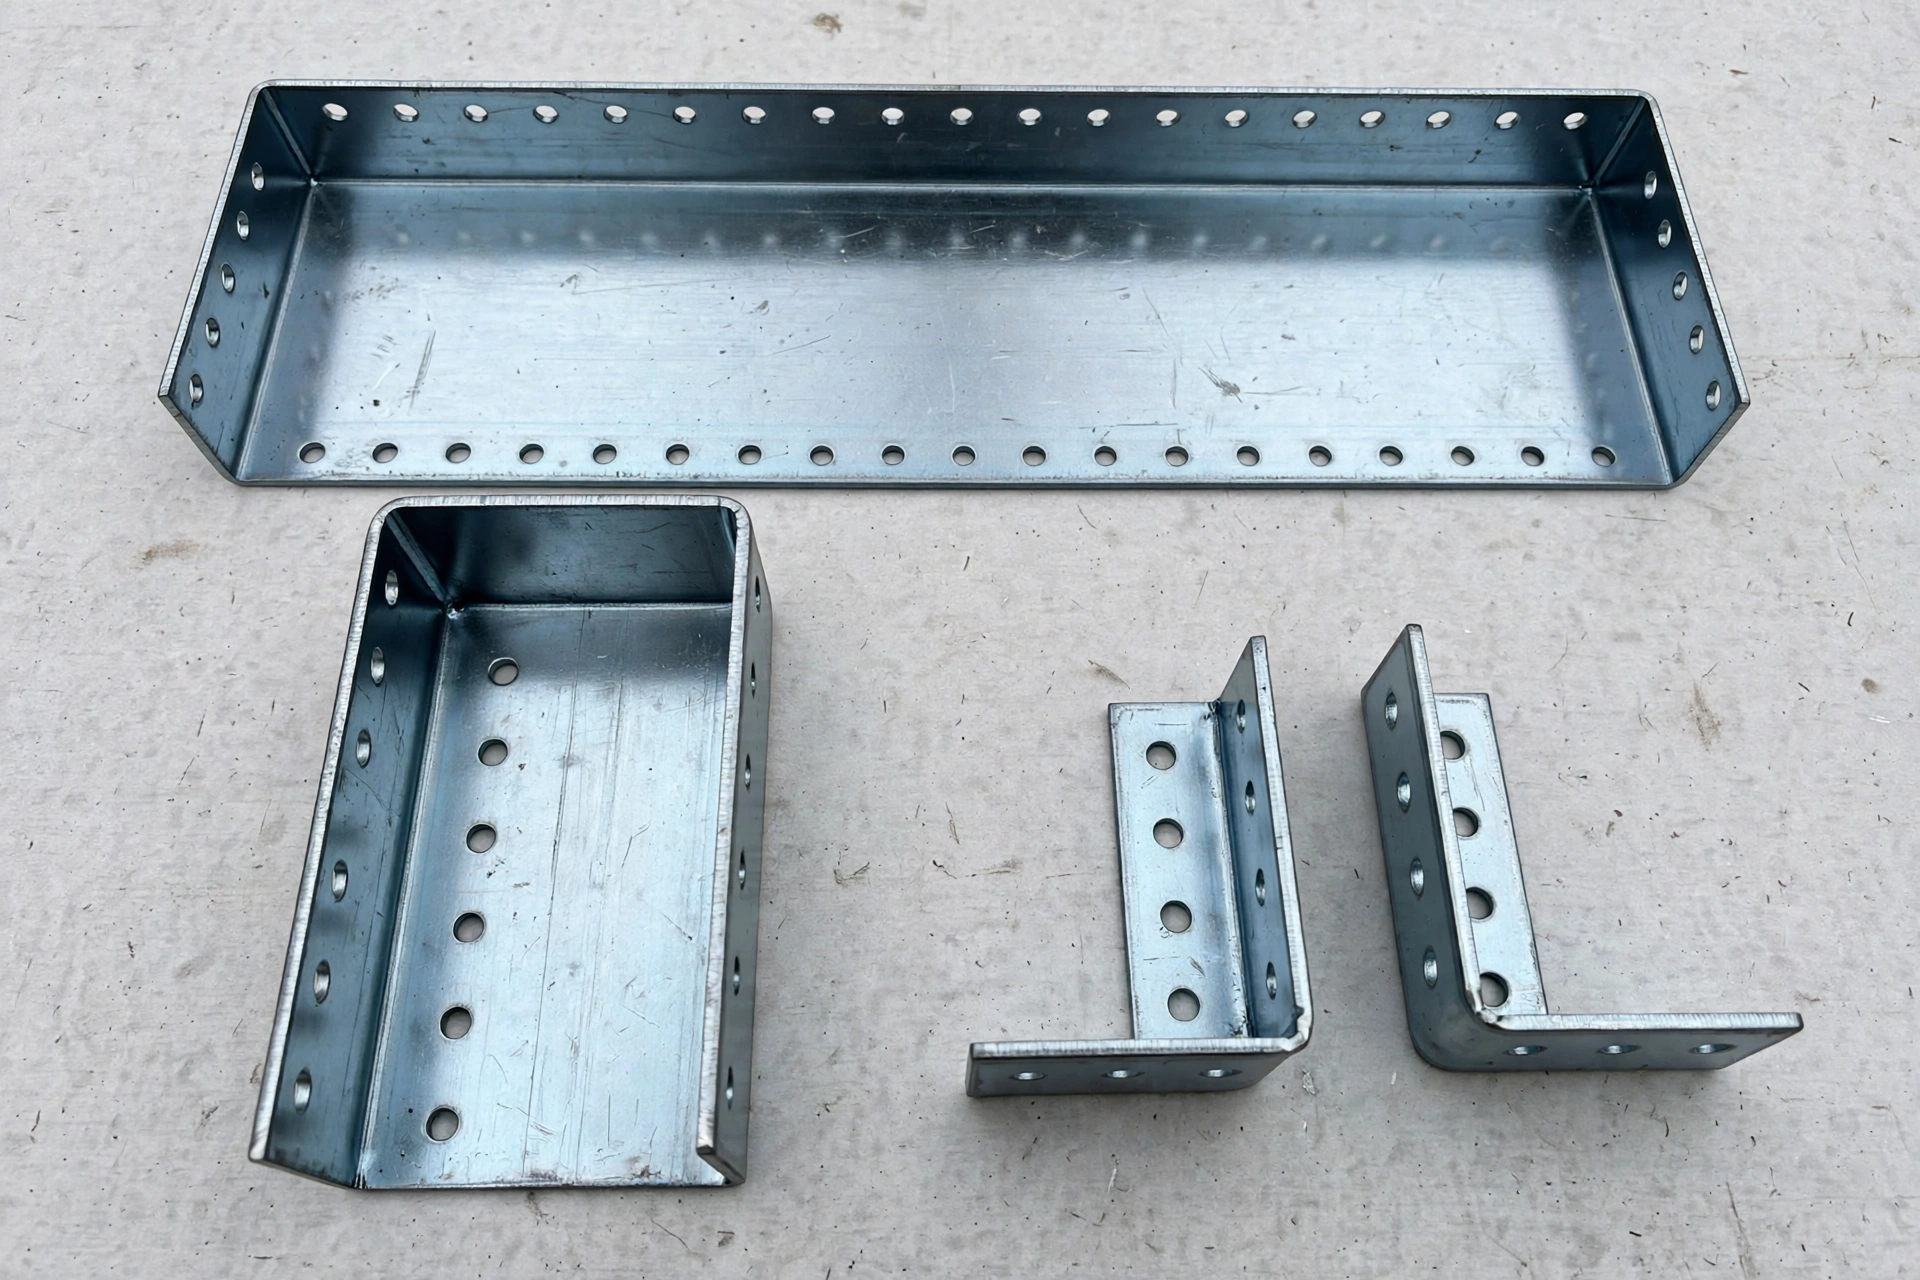
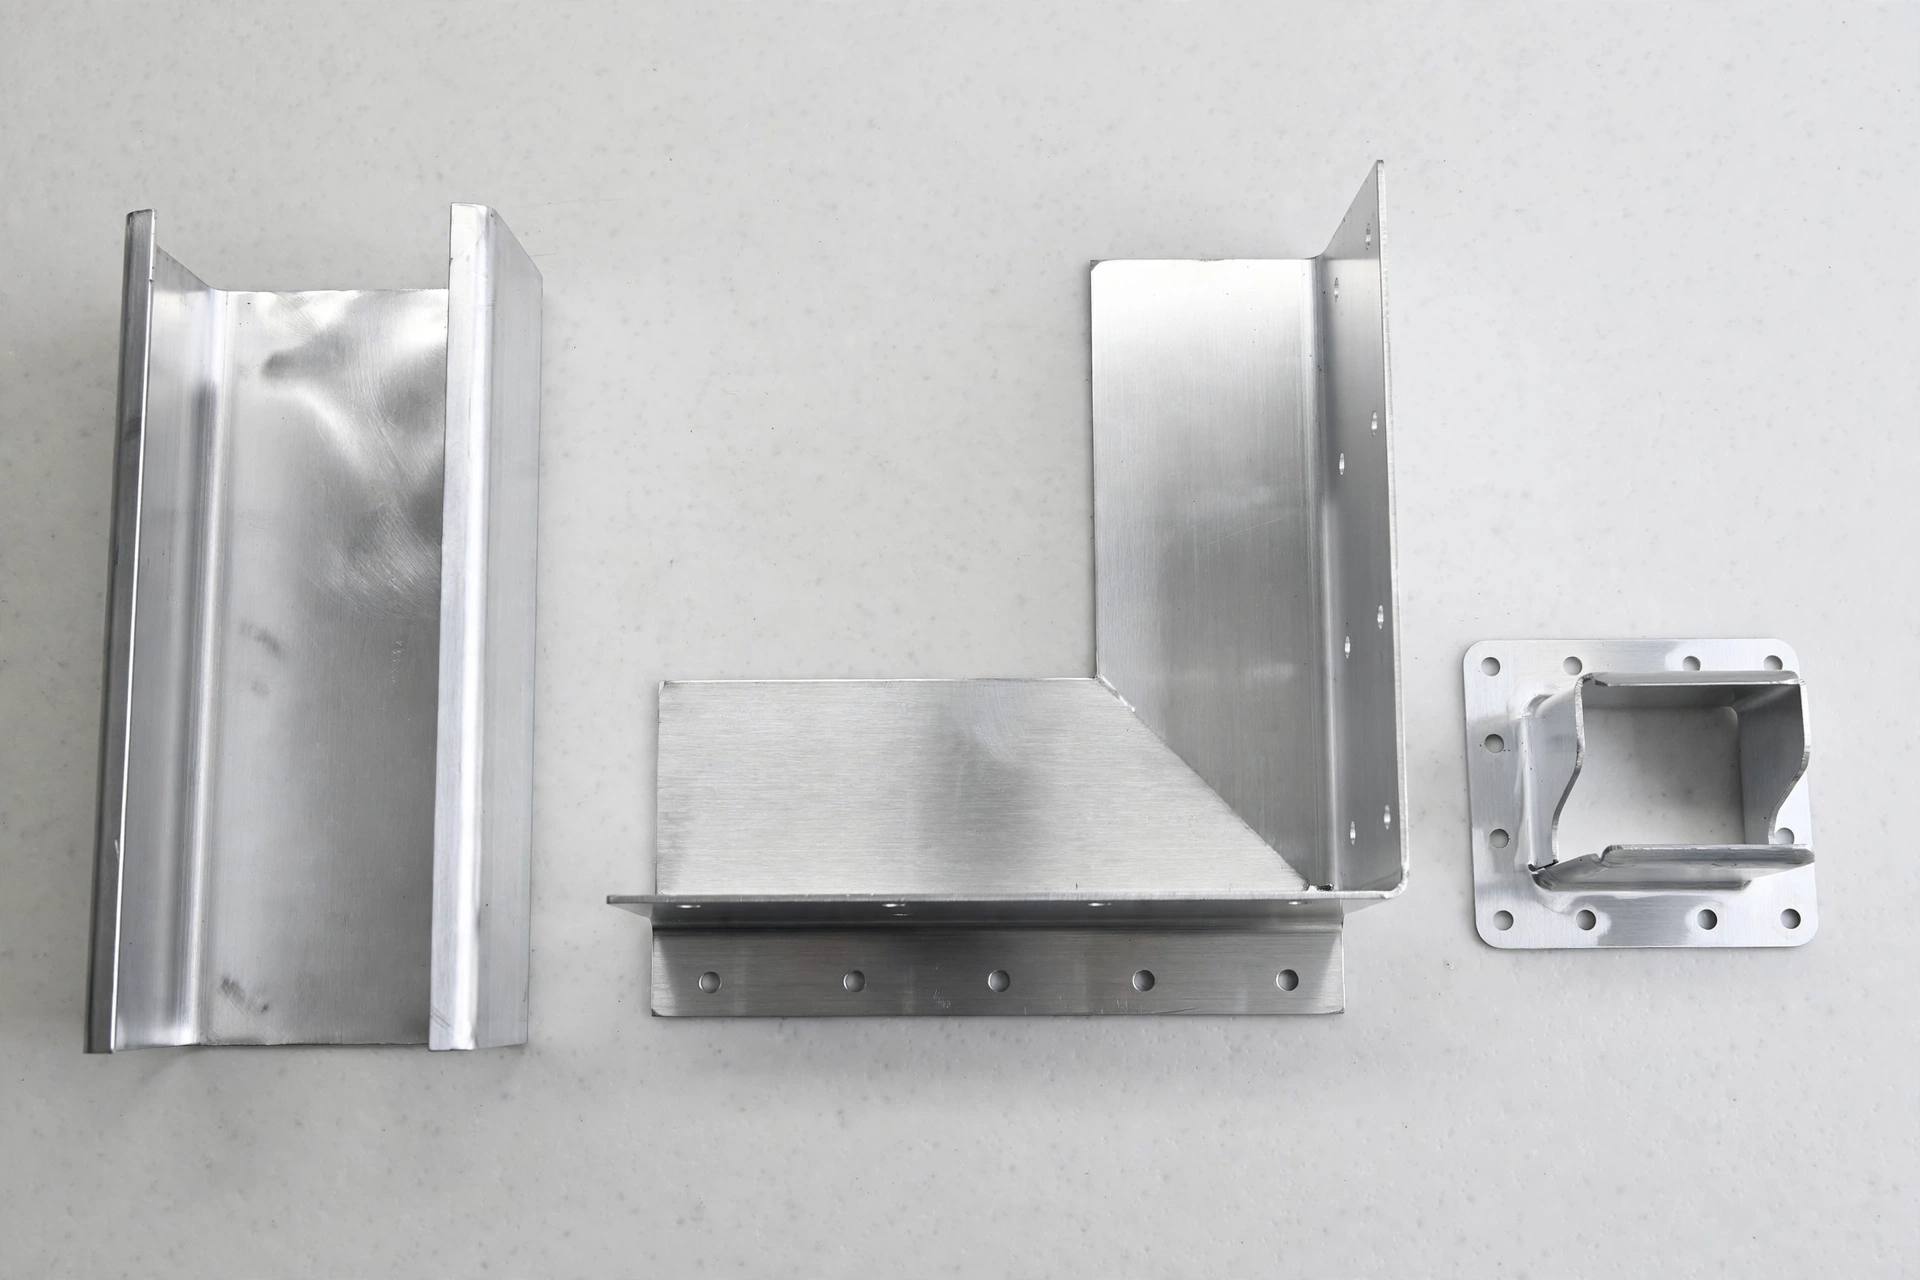
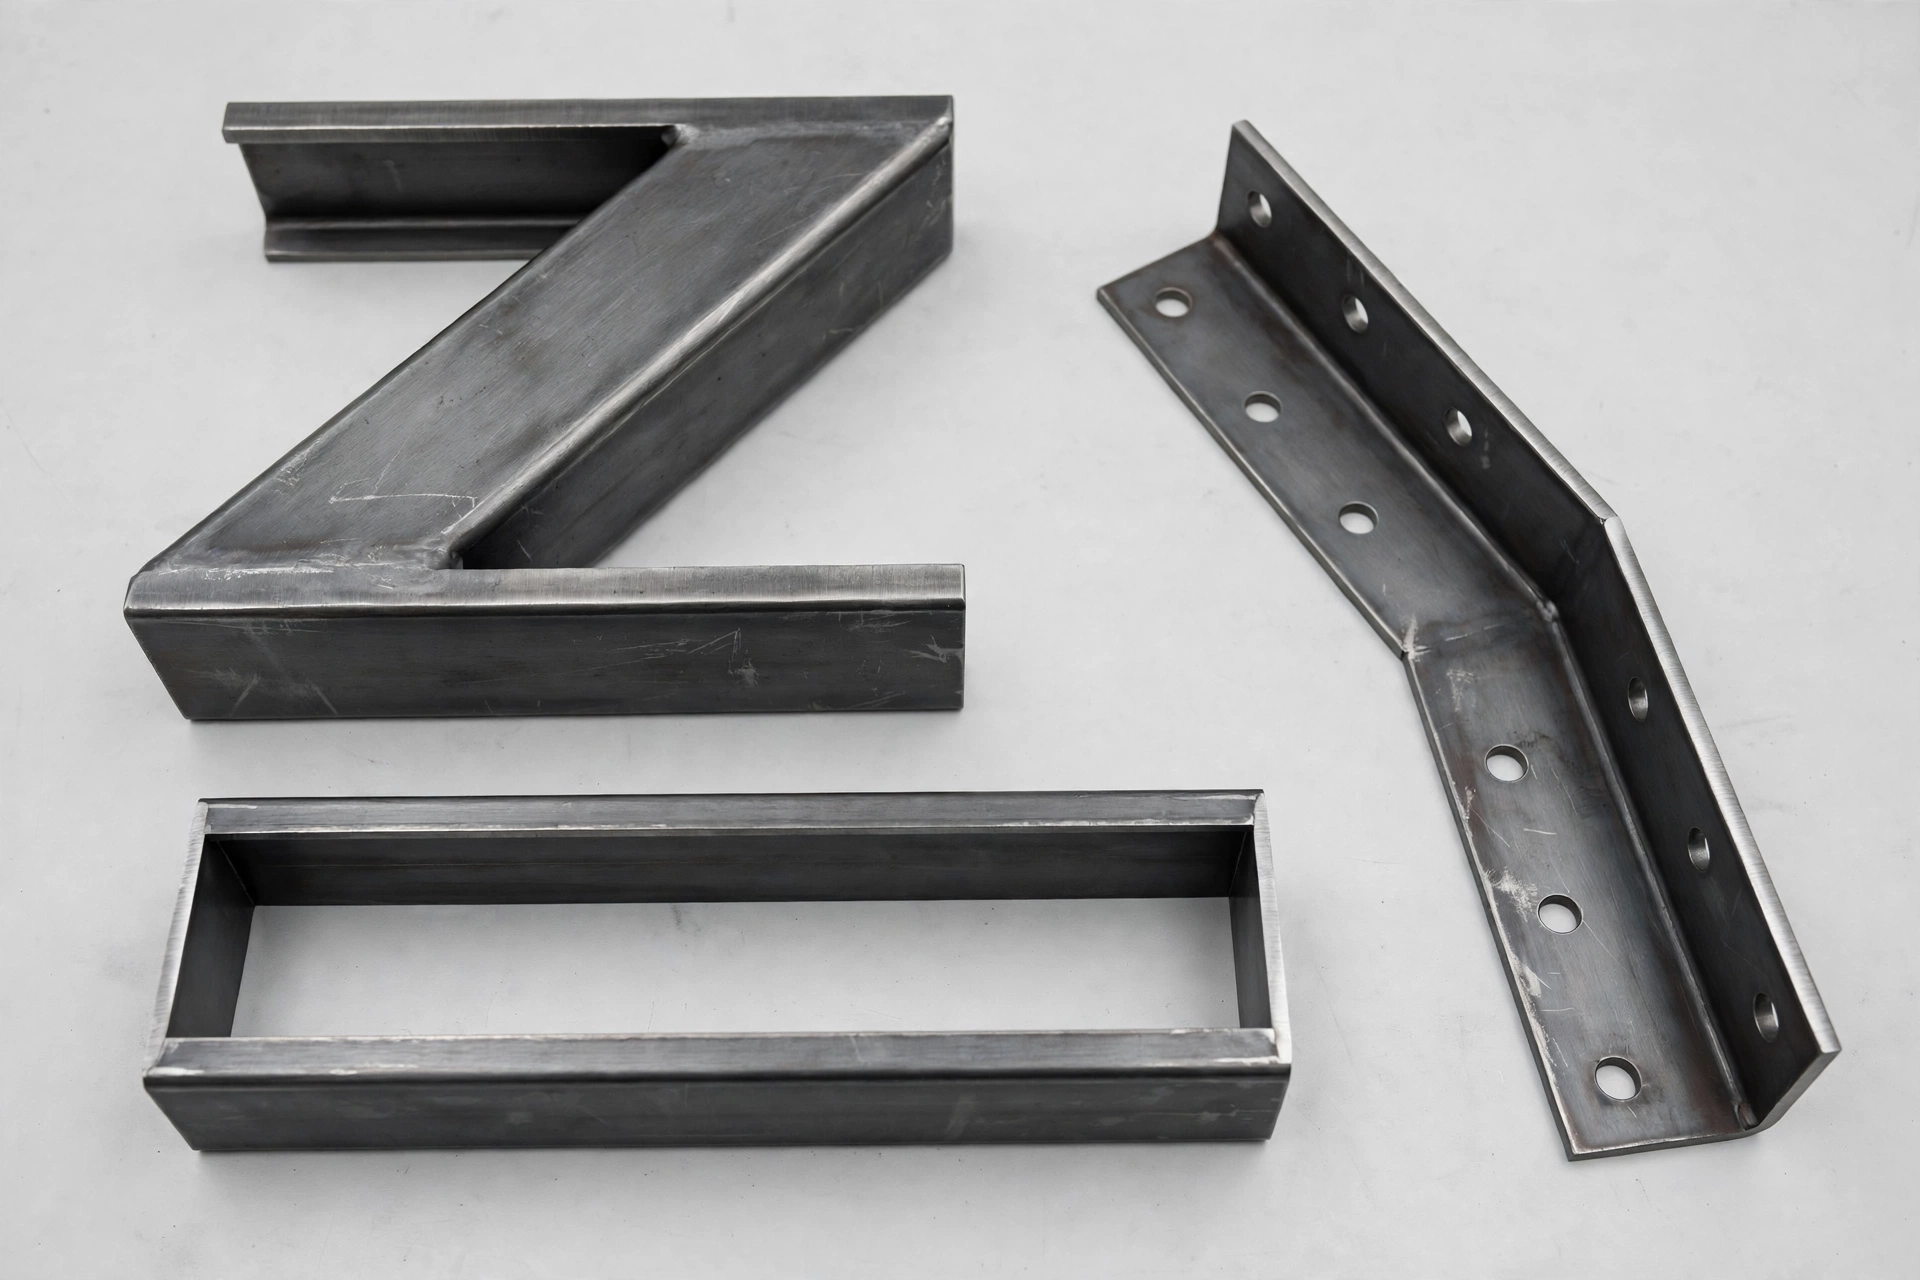
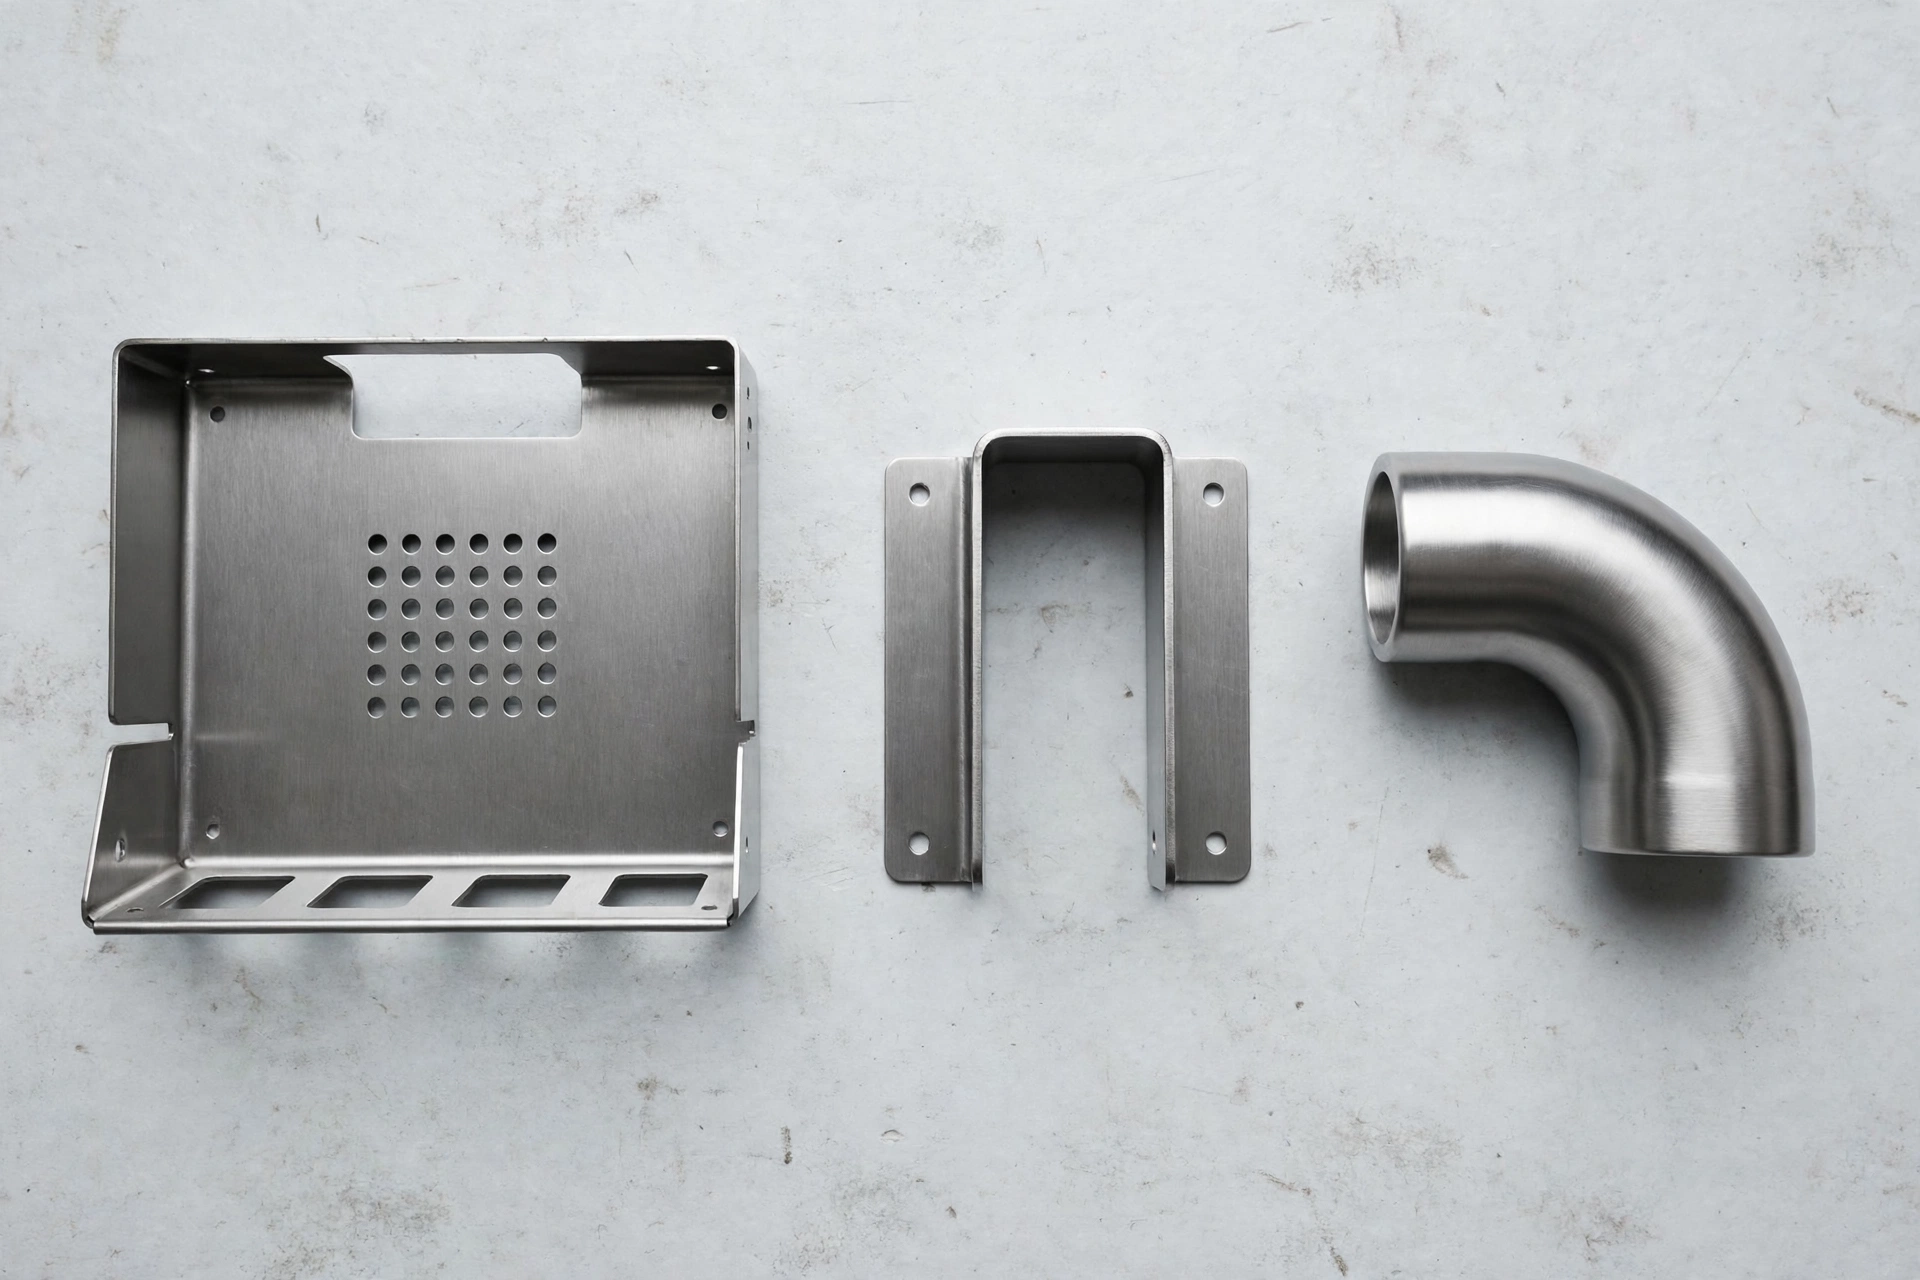
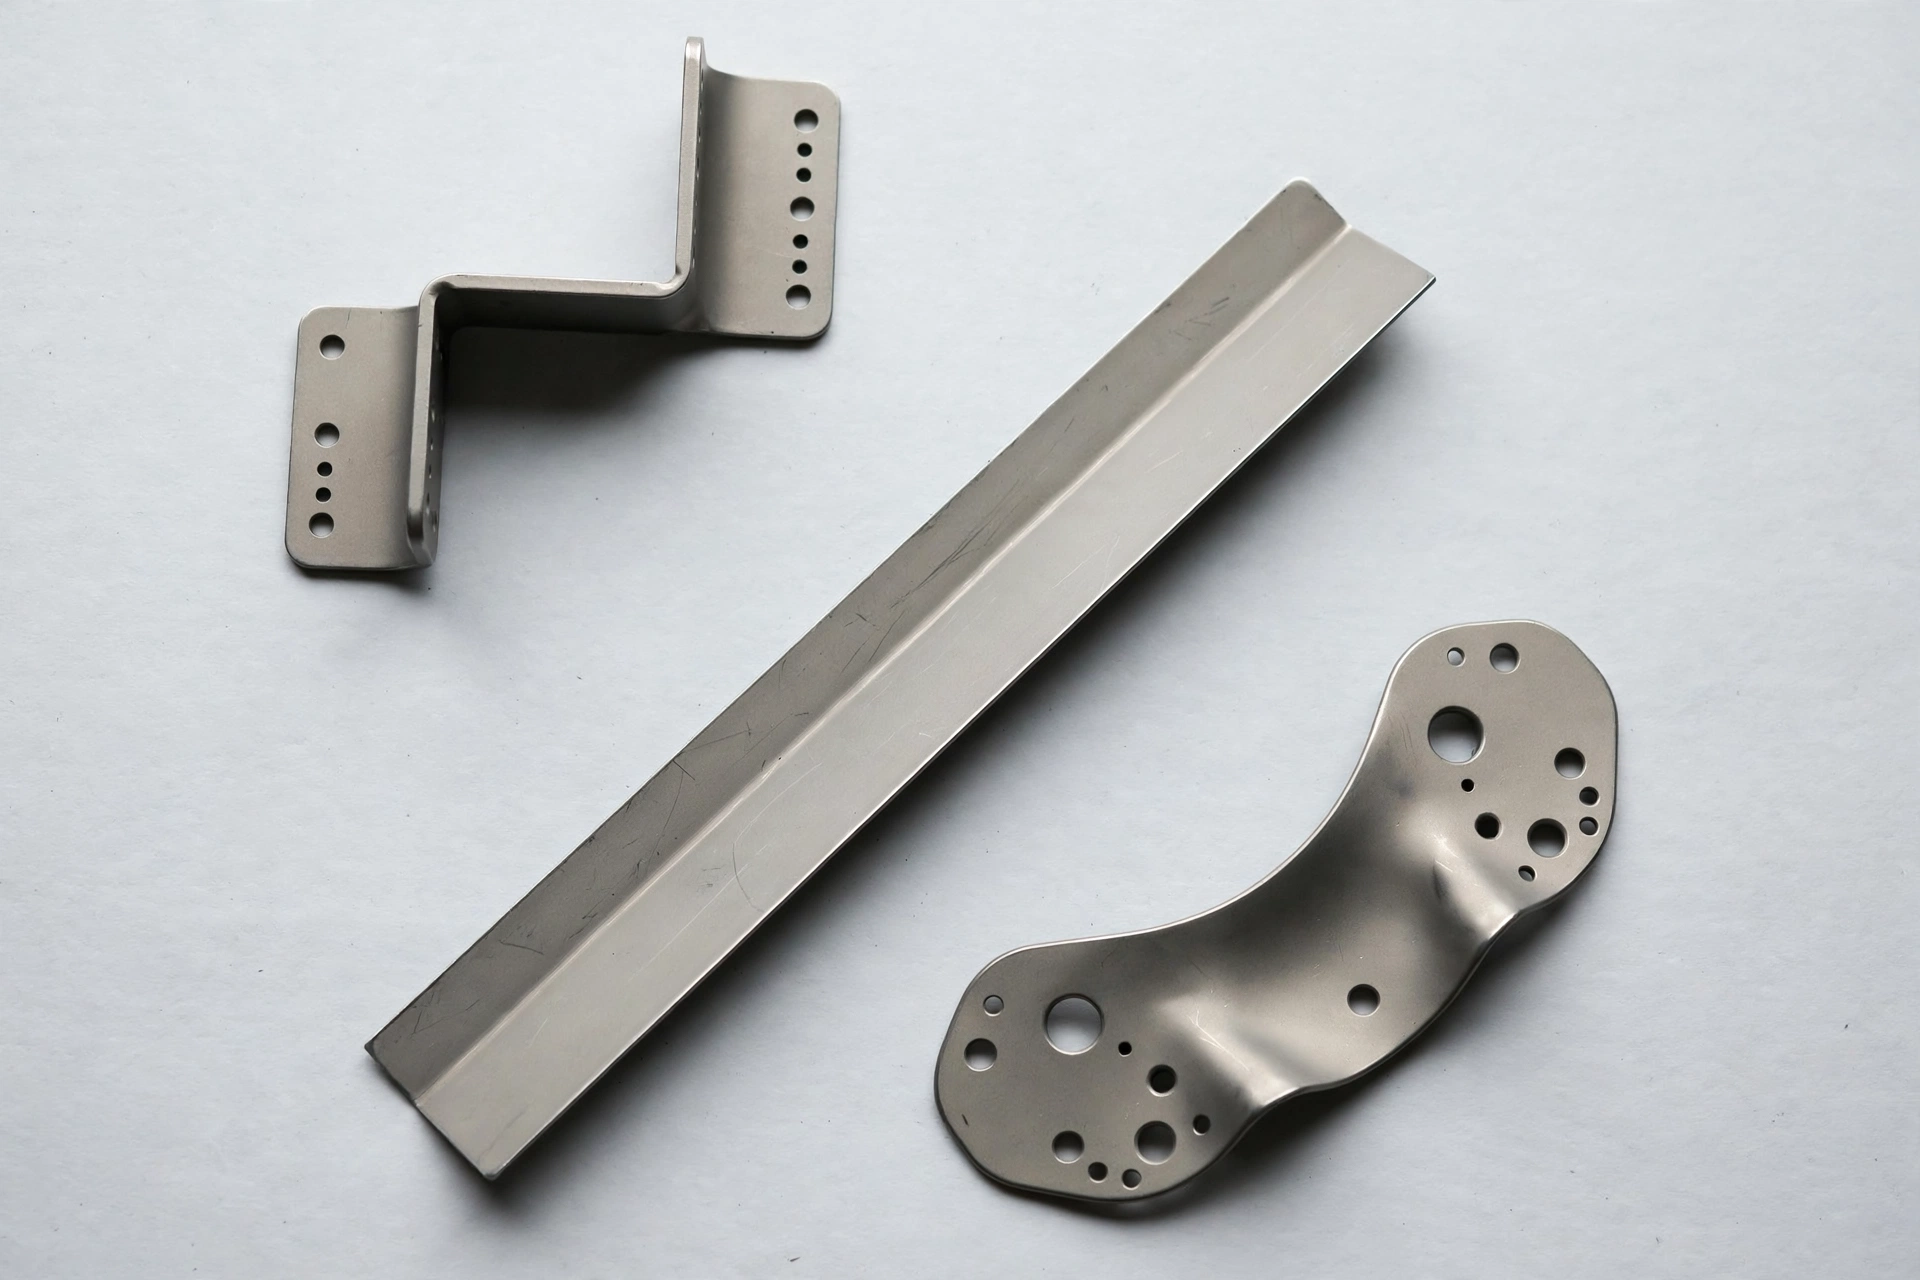
Our CNC press brakes apply up to 250 tons over a 3200 mm working length. They form V-bends, U-bends, Z-bends, hems, offset bends and channels. Angular accuracy is ±0.1° and flange positions hold ±0.4 mm.
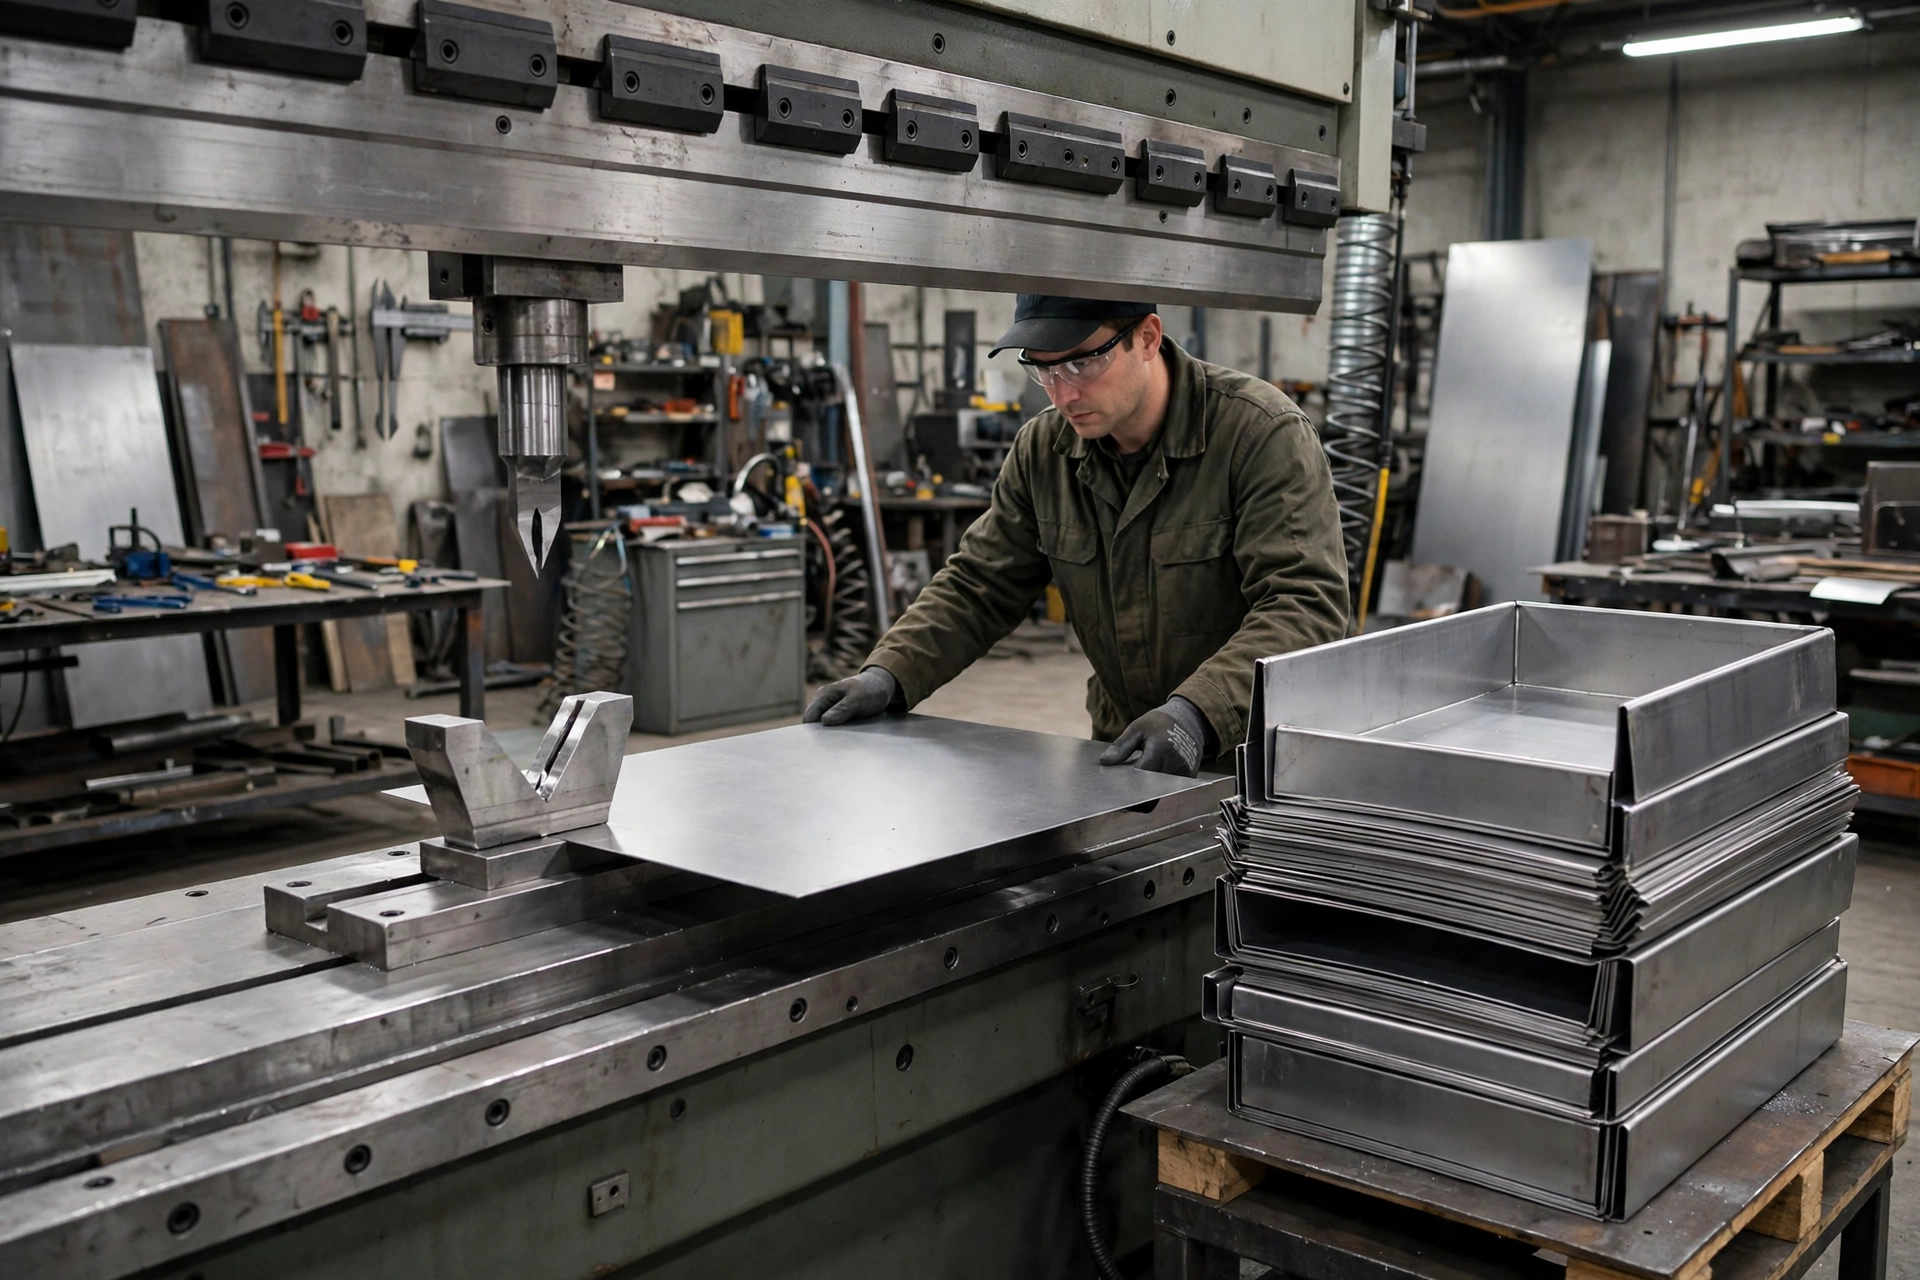
Multi-axis CNC back gauges position the sheet for each bend with ±0.1 mm repeatability. A press brake can make up to 12 sequential bends in one part without re-fixturing. That turns a single flat blank into a finished enclosure, bracket or channel.
Upload a STEP file or a 2D drawing with bend callouts. Engineers calculate the K-factor, bend deductions and flat pattern layout, and DFM feedback arrives within 12 hours.
How Do We Hold Bend Accuracy?
Sheet metal springs back after bending, so we overbend it. The CNC controller sets the overbend angle for each material and thickness. Aluminum 5052 springs back 1 to 3°, and stainless 304 springs back 3 to 5°. The controller adjusts for both automatically.
Why Choose XC for Metal Bending
XC Machining press brakes give ±0.1° angular accuracy on steel, stainless, aluminum, copper, brass and titanium from 0.5 to 12 mm. Cutting, welding and finishing sit in the same ISO 9001:2015 factory in Dongguan.

The brakes run up to 250 tons over 3200 mm, with a CNC back gauge that positions to ±0.1 mm. Up to 12 bends fit in one part. V-dies, U-dies, gooseneck tools and hemming tools are available.

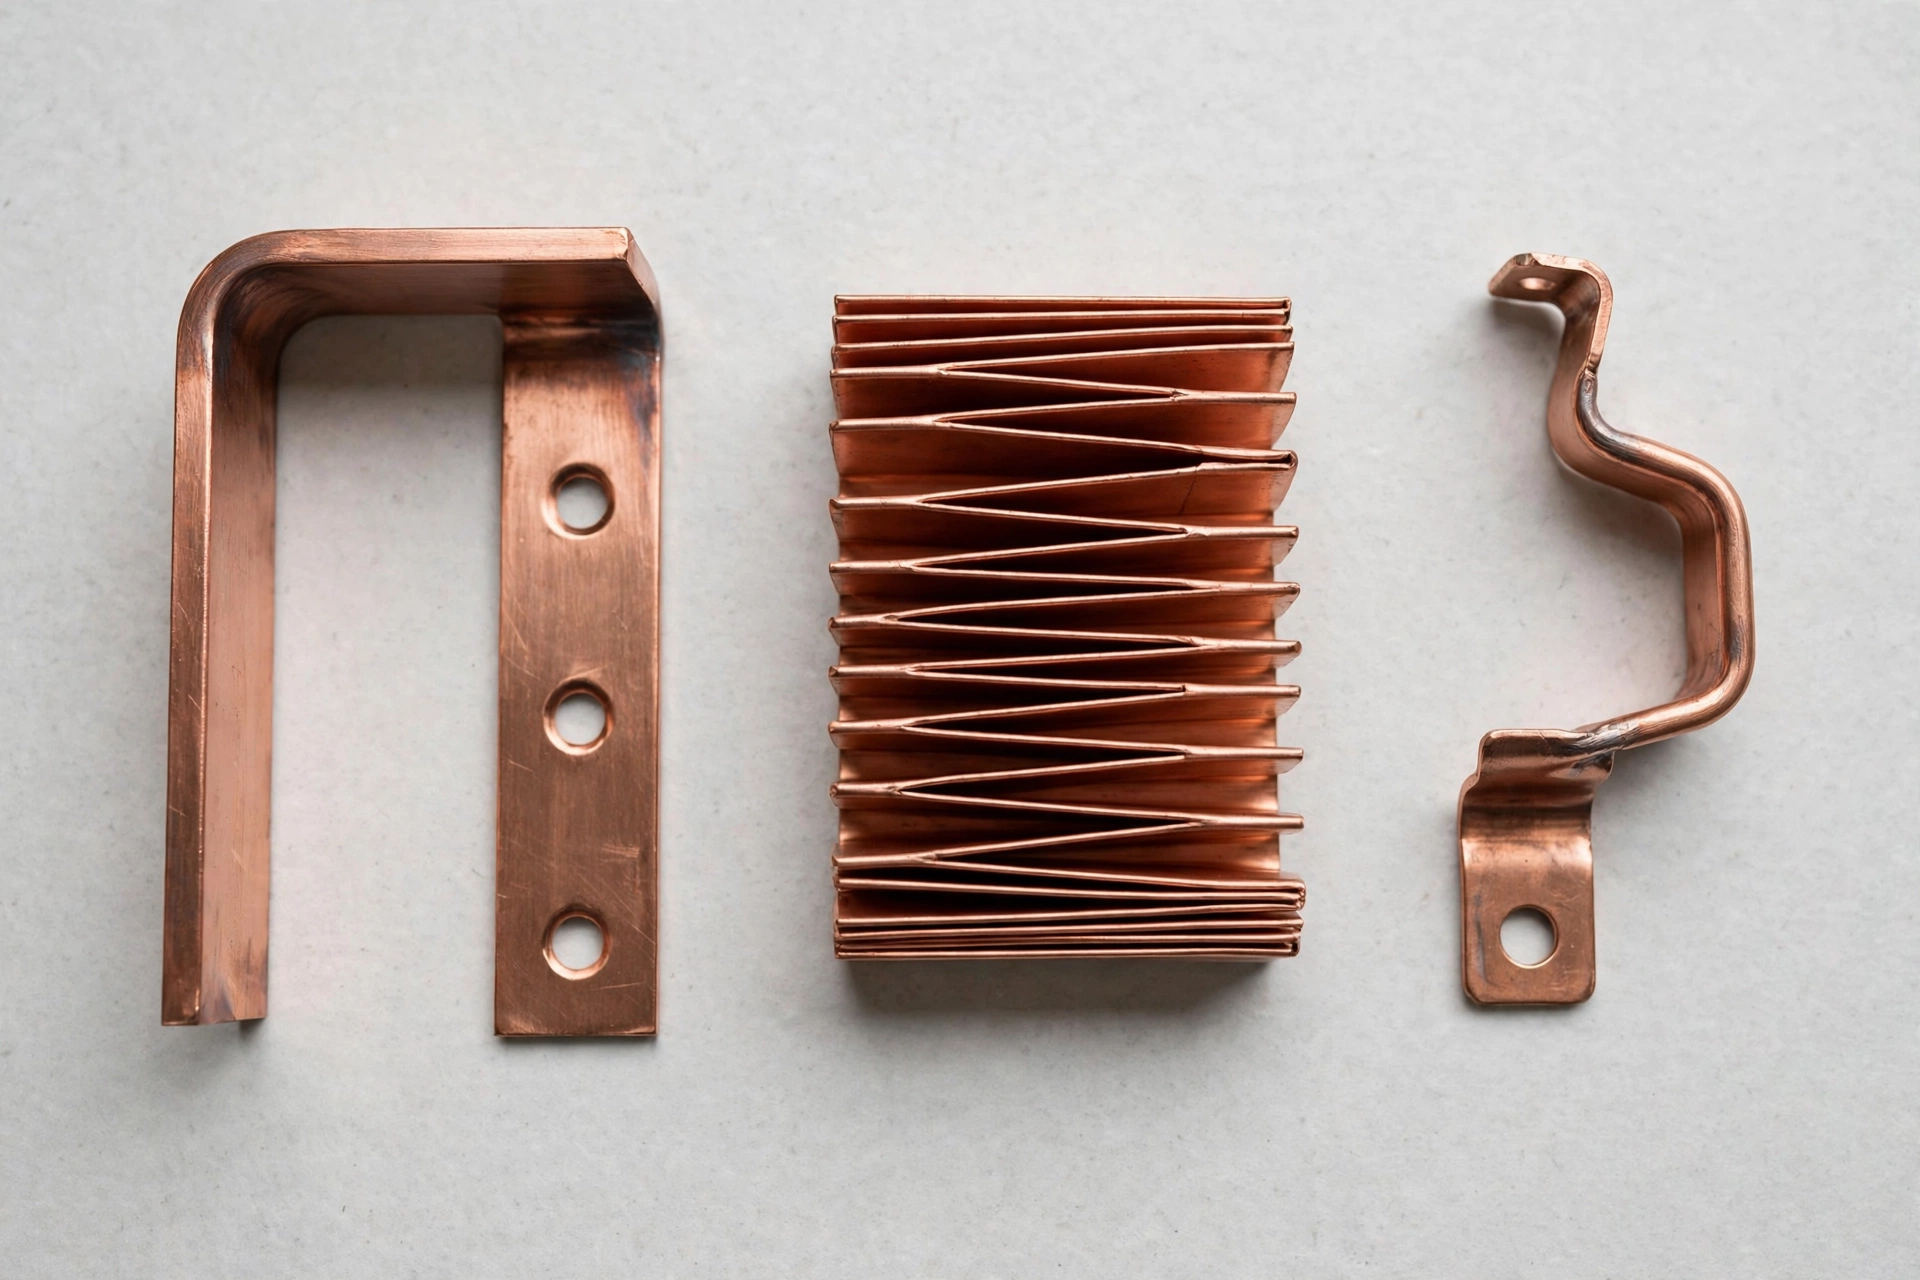
Steel A36 and 1018 bend from 0.5 to 12 mm. Stainless 304, 316 and 430 bend from 0.5 to 6 mm. Aluminum 5052 and 6061 bend from 0.5 to 10 mm. Copper C110 and brass C260 and C360 bend from 0.5 to 3 mm. Spring steel 1095 and 1075 bend from 0.5 to 2 mm, and titanium Grade 2 from 0.5 to 4 mm.

Engineers check minimum bend radius (1× thickness as standard) and minimum flange length (at least 2× thickness plus the bend radius). They check hole-to-bend distance (at least 2× thickness) and the cumulative tolerance on multi-bend parts. Springback compensation is set per material.

Options include deburring and powder coating at 60 to 120 μm. Anodizing comes in Type II or III. Zinc plating runs 5 to 25 μm, brushing Ra 0.4 to 0.8 μm, and painting matches RAL or Pantone colors. Stainless parts can be electropolished.
Metal Bending Tolerances
| Feature | Tolerance | Note |
| Bend angle | ±1° to ±2° | Depends on material elasticity and tooling precision |
| Bend radius | ±0.25 mm (±0.010 in) | Springback can shift the actual radius slightly |
| Bend position (flange length) | ±0.4 to ±0.8 mm (±0.016 to ±0.032 in) | Tighter values need CNC-controlled press brakes |
| Flat pattern accuracy | ±0.25 to ±0.5 mm (±0.010 to ±0.020 in) | Applies to the laser or punch cut before bending |
| Bend-to-hole distance | ±0.5 mm (±0.020 in) | Holes near bends can deform without allowance |
| Hole deformation near a bend | Keep the hole edge at least 2× thickness from the bend | Prevents ovaling and distortion |
| Material springback | Varies by material | Aluminum springs back less than stainless steel |
| Minimum flange length | At least 2× material thickness | Shorter flanges may not form or can crack |
| Cumulative tolerance (multiple bends) | ±0.8 to ±1.5 mm total | Matters for folded enclosures and box shapes |
How a Part Goes From File to Bent
Each step below uses data from XC’s press brake and DFM setup.
| Step | What happens | Detail |
| 1. Upload | Send a STEP file or 2D drawing with bend callouts | Feedback within 12 hours |
| 2. Flat pattern | Engineers set the K-factor, bend deductions and layout | Flat pattern accuracy ±0.25 to ±0.5 mm |
| 3. Cutting | The blank is laser cut or punched | Holes sit at least 2× thickness from bends |
| 4. Bending | The CNC back gauge positions each bend | Up to 12 bends per part, ±0.1 mm repeatability |
| 5. Springback | The controller overbends to the target angle | Set per material and thickness |
| 6. Finishing | Deburring comes first, then any coating | Deburring is standard on production orders |
Parts that need welded seams move on to sheet metal fabrication without leaving the factory.
Finishes for Bent Metal Parts
A finish hides bend marks and protects the part. The list below covers what XC applies after bending. Our surface finishing page covers each in depth.
Visible tool marks at Ra 3.2 to 6.3 μm. It suits internal structural parts that need no cosmetic look.
Removes sharp edges from bend lines to Ra 1.6 to 3.2 μm for safe handling and assembly fit. It is standard on production orders.
A directional satin grain at Ra 0.4 to 0.8 μm on aluminum and stainless. It masks bend marks on decorative enclosures and panels.
A 60 to 120 μm polymer layer in RAL or Pantone colors. Salt spray resistance runs 500 to 1,000 hours, with UV resistance.
Removes 5 to 15 μm from stainless parts for a smooth Ra 0.2 to 0.4 μm finish and better corrosion resistance.
Type II or III on aluminum, with a 5 to 80 μm oxide layer and color options. It keeps the bent geometry.
A 5 to 25 μm layer on steel parts.
A coat matched to RAL or Pantone colors.
A uniform matte texture that reduces visible marks and prepares the surface for coating.
Smooths accessible surfaces to a satin or reflective look.
Nickel, chrome, zinc or gold layers for corrosion resistance, conductivity or wear.
Our Metal Bending Prototype Manufacturing Capabilities
Provides injection molding for prototypes and custom parts, emphasizing expert support, competitive pricing, and faster production cycles.
Get reliable vacuum casting services for high-quality prototypes and production parts at competitive prices. XC Machining offers highly detailed casting parts with consistent quality.
Uses cutting, bending, and forming techniques to produce precision metal components suited for industrial, commercial, and manufacturing applications.
Specialist Industries
Metals We Bend
Each tab lists the thickness range we bend for that metal. Strength values come from the live material tabs.
Aluminum bends from 0.5 to 10 mm and springs back less than stainless. That makes it forgiving for housings, brackets and enclosures. Color is silver. Yield strength runs 230 to 570 MPa. Bending grades are 5052, 6061 and 3003.
Carbon steel bends the thickest, from 0.5 to 12 mm, with the lowest springback at 0.5 to 2°. It forms brackets, frames and structural parts. Color is reddish brown. Yield strength runs 200 to 900 MPa and tensile strength 350 to 1,100 MPa. Grades are A36 and 1018.
Stainless bends from 0.5 to 6 mm and springs back the most, 3 to 5°, so overbend control matters. It forms food equipment, medical parts and marine fittings. Color is silver gray. Yield strength runs 170 to 1,170 MPa and tensile strength 485 to 1,310 MPa. Grades are 304, 316 and 430.
Titanium Grade 2 bends from 0.5 to 4 mm. It serves aerospace and medical sheet parts. Yield strength runs 170 to 900 MPa and tensile strength 240 to 1,000 MPa.
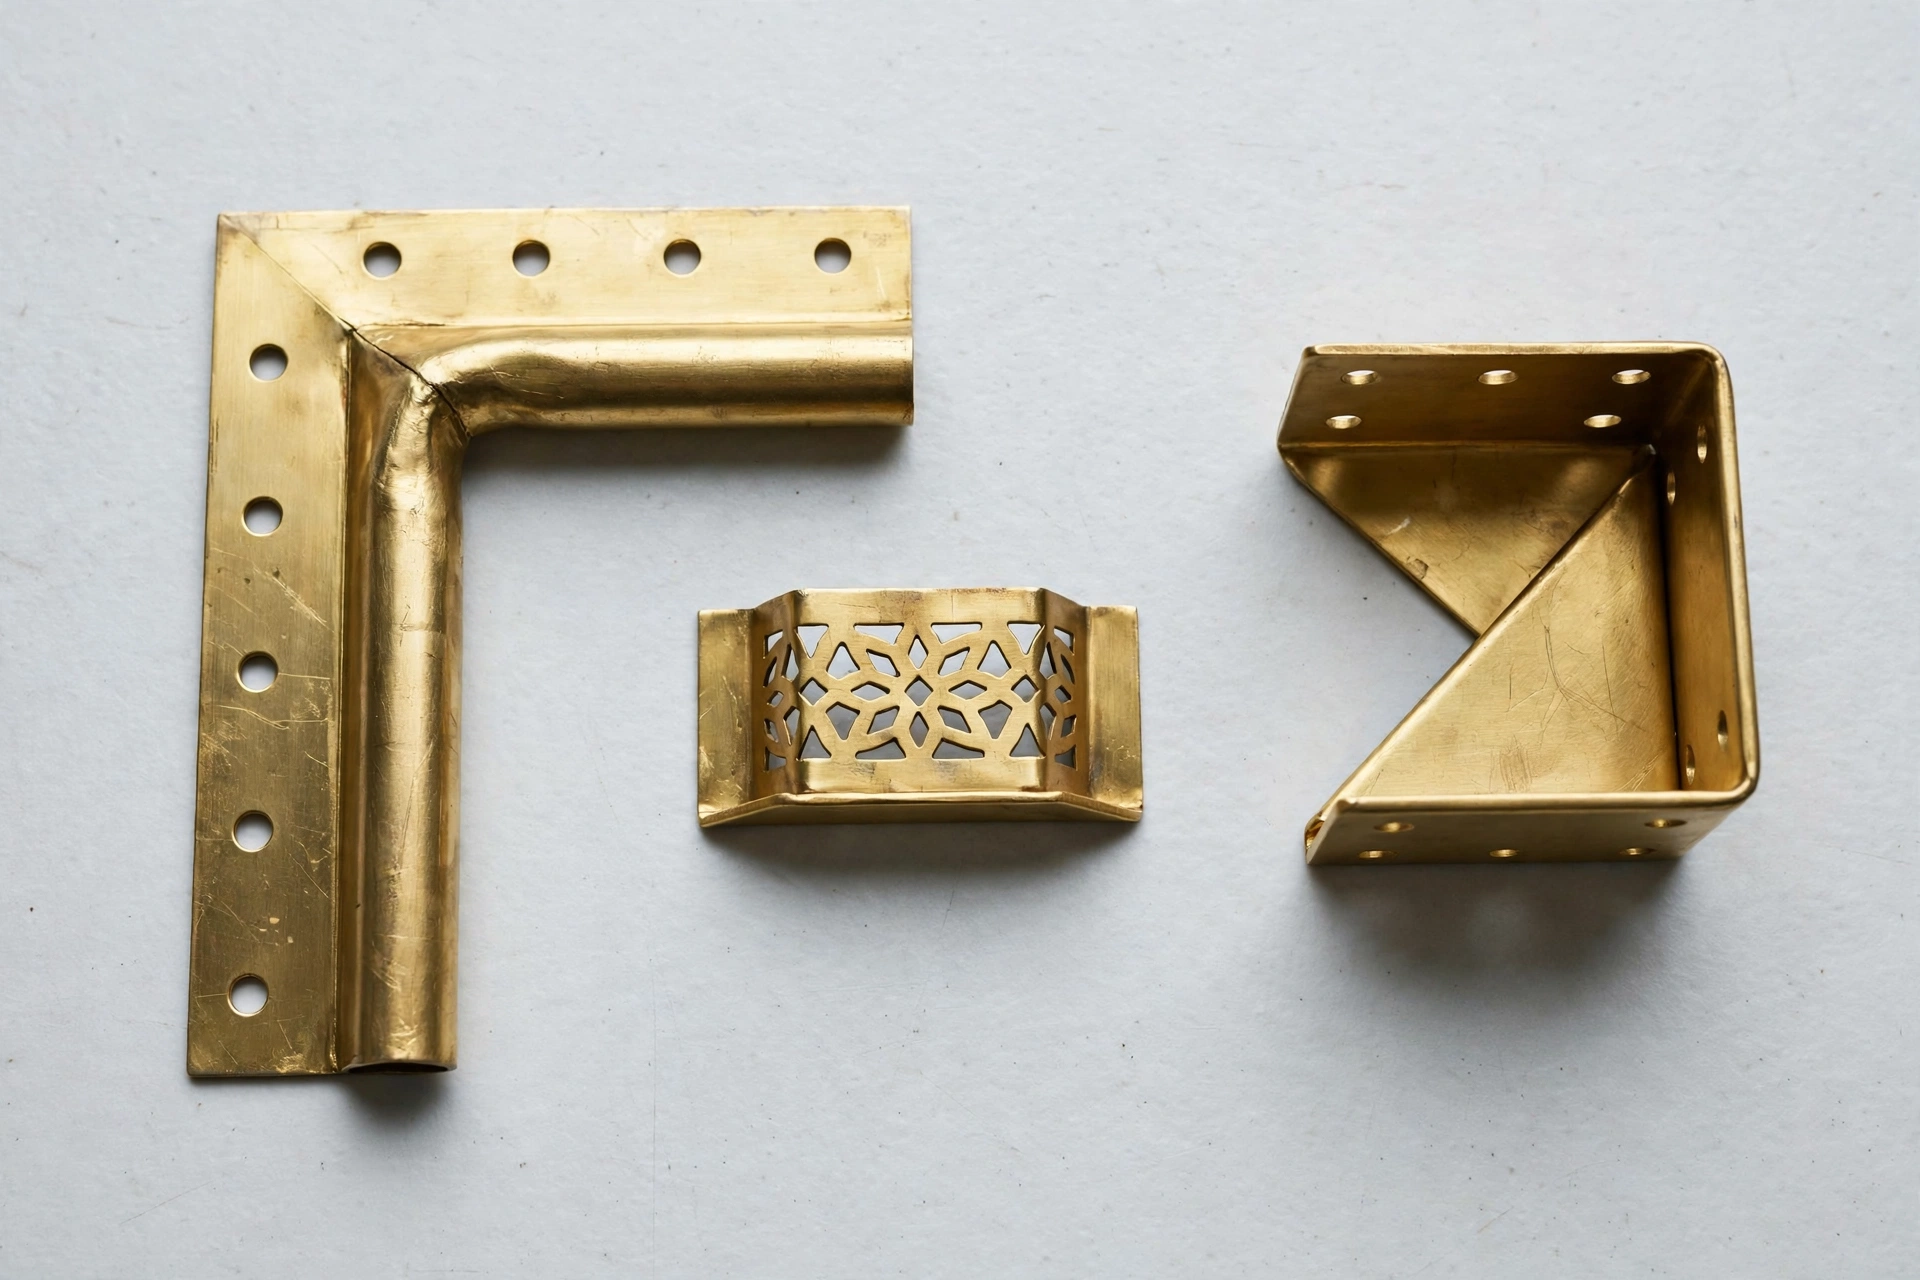
Brass bends from 0.5 to 3 mm and takes a clean fold for connectors, plates and decorative parts. Color is golden yellow. Yield strength runs 75 to 450 MPa and tensile strength 300 to 600 MPa. Grades are C260 and C360.
Metals and Grades for Bending
5052, 6061, 3003
304, 316, 430
A36, 1018, 1020
G90, G60
1095, 1075
C110, C122
C260, C360
Grade 2, Grade 5 (Ti-6Al-4V)
Bring Your Designs to Life with XC Machining
Experience precision engineering with XC Machining. From detailed prototypes to high-volume production, we’re here to turn your concepts into reality. Contact us today to discuss your project needs!
- 50+ CNC machines in-house
- 60+ materials in stock
- 120+ countries shipped
- 15+ DFM engineers on staff
- All uploads are secure and confidential
Metal Bending FAQs
What is CNC press brake metal bending?
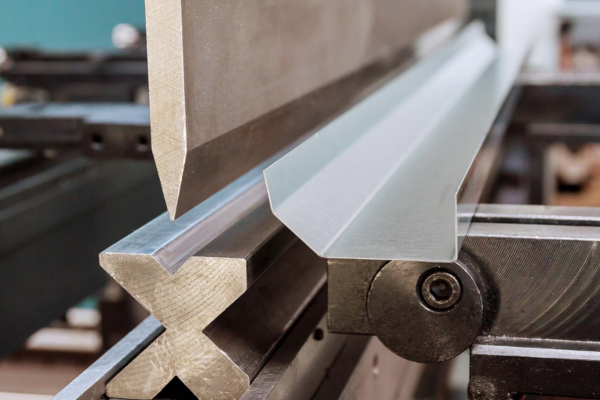
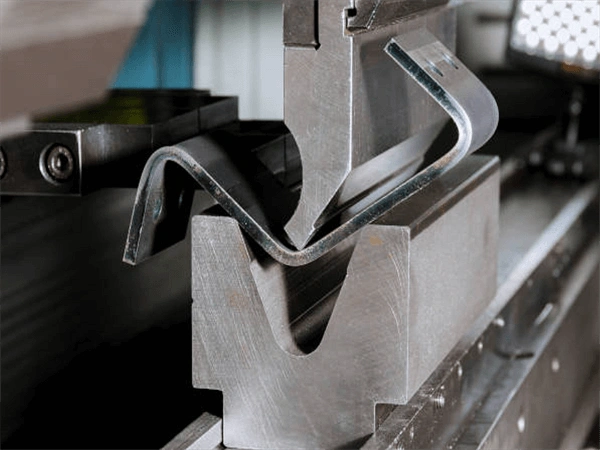
CNC press brake bending clamps sheet metal between a bottom V-die and a top punch to form precise angles. XC Machining press brakes apply up to 250 tons over a 3200 mm working length. A CNC back gauge positions the sheet to ±0.1 mm, so bend locations repeat across a production run.
What materials can XC Machining CNC bend?
Steel A36 and 1018 bends from 0.5 to 12 mm. Stainless 304, 316 and 430 bends from 0.5 to 6 mm, and aluminum 5052, 6061 and 3003 from 0.5 to 10 mm. Copper C110 and brass C260 and C360 bend from 0.5 to 3 mm. Spring steel 1095 bends to 2 mm and titanium Grade 2 to 4 mm.
What are the limitations of metal bending?
Material thicker than 12 mm needs a heavier press brake. Hardened spring steel can crack at tight radii, so its minimum radius is 2× thickness. Cumulative tolerance grows with each bend, reaching ±0.8 to ±1.5 mm on parts with four or more bends. Holes must sit at least 2× thickness from a bend.
What is springback and how is it compensated?
Springback is the elastic recovery after bending, when the metal partly returns toward flat. Aluminum 5052 springs back 1 to 3°, stainless 304 springs back 3 to 5° and mild steel springs back 0.5 to 2°. Our CNC press brakes overbend automatically, using the material, thickness and bend radius to calculate the angle.