Home - Insert Molding

Insert Molding Services

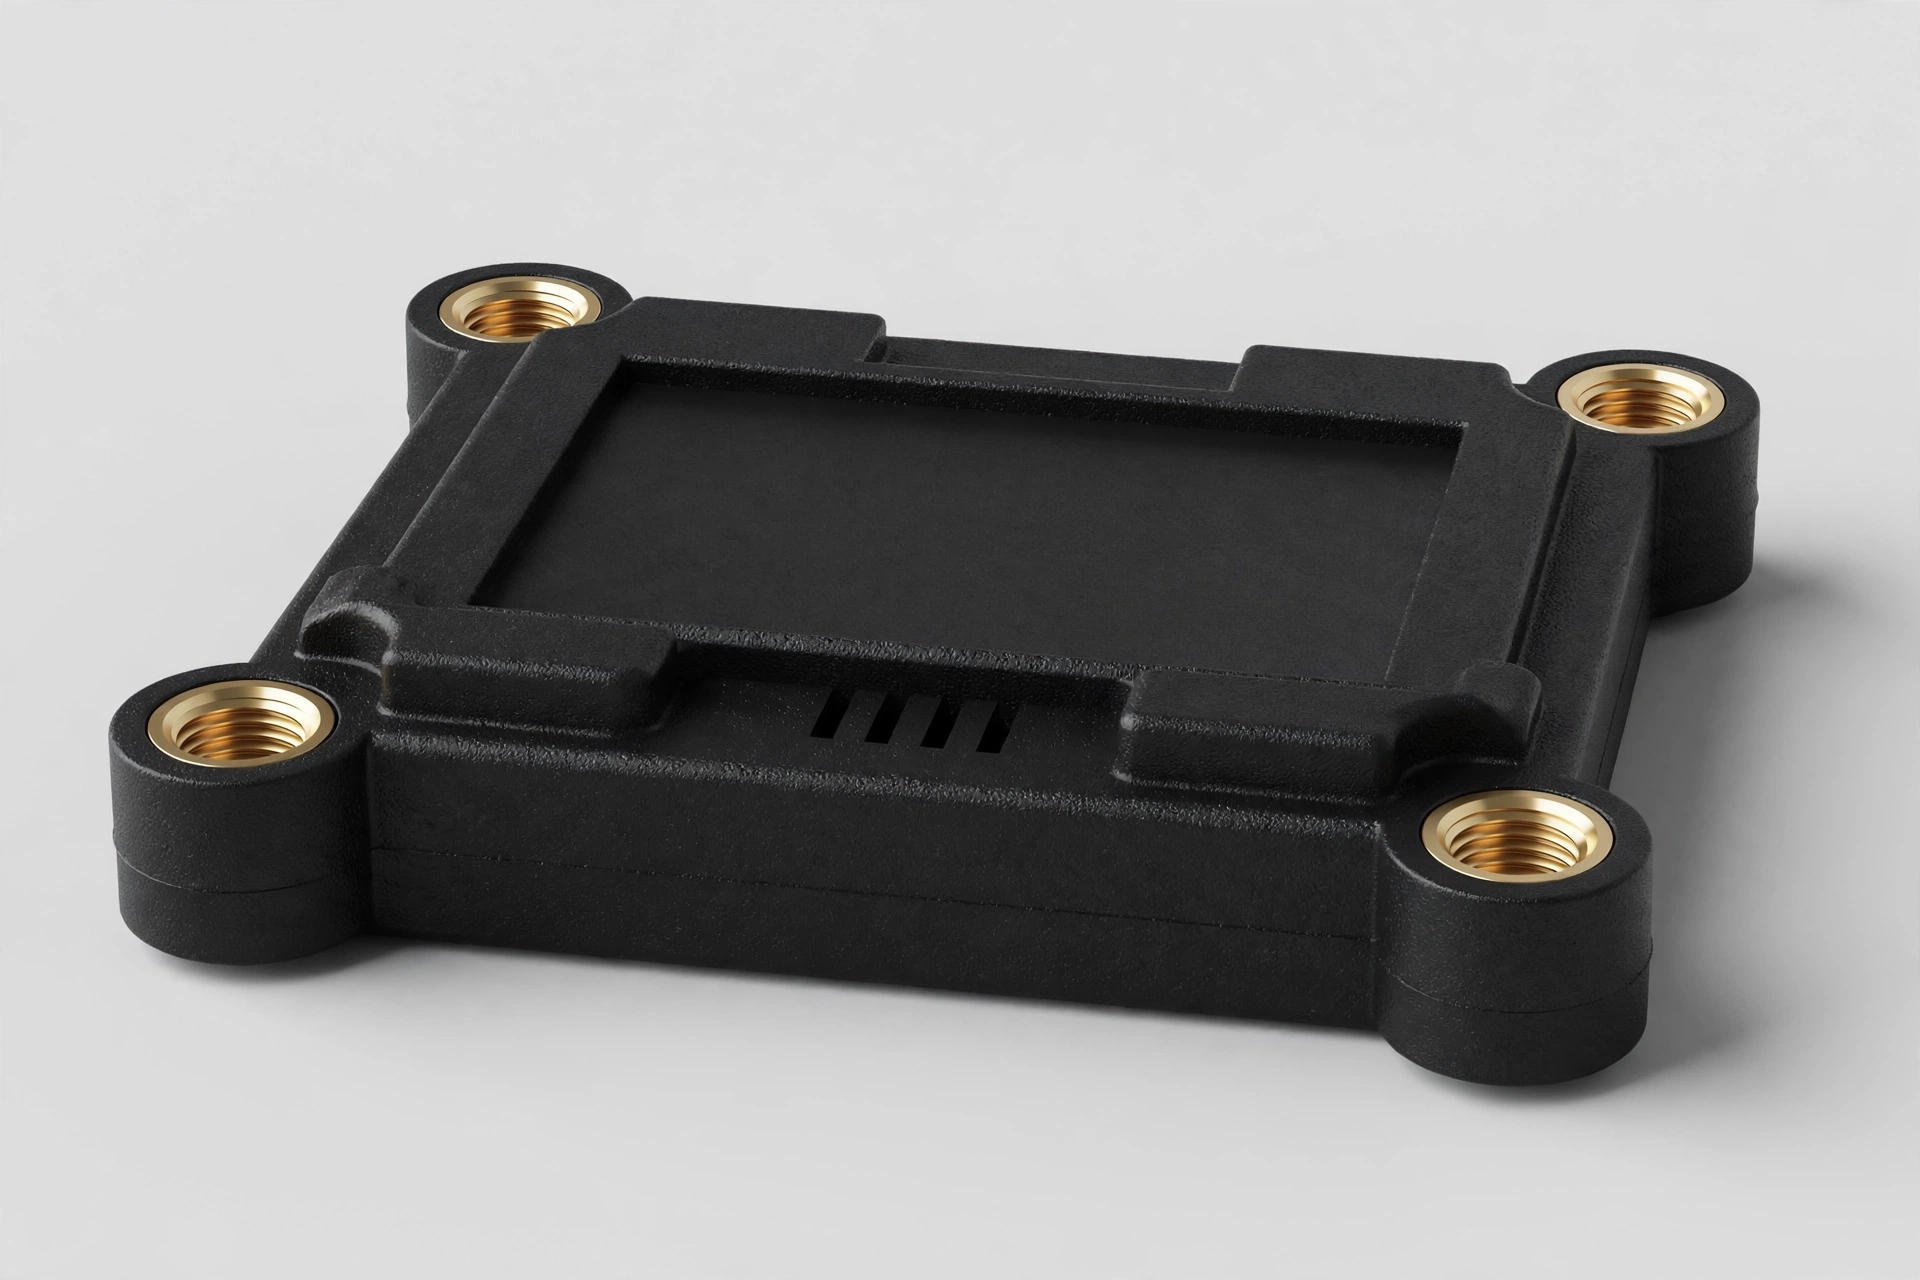
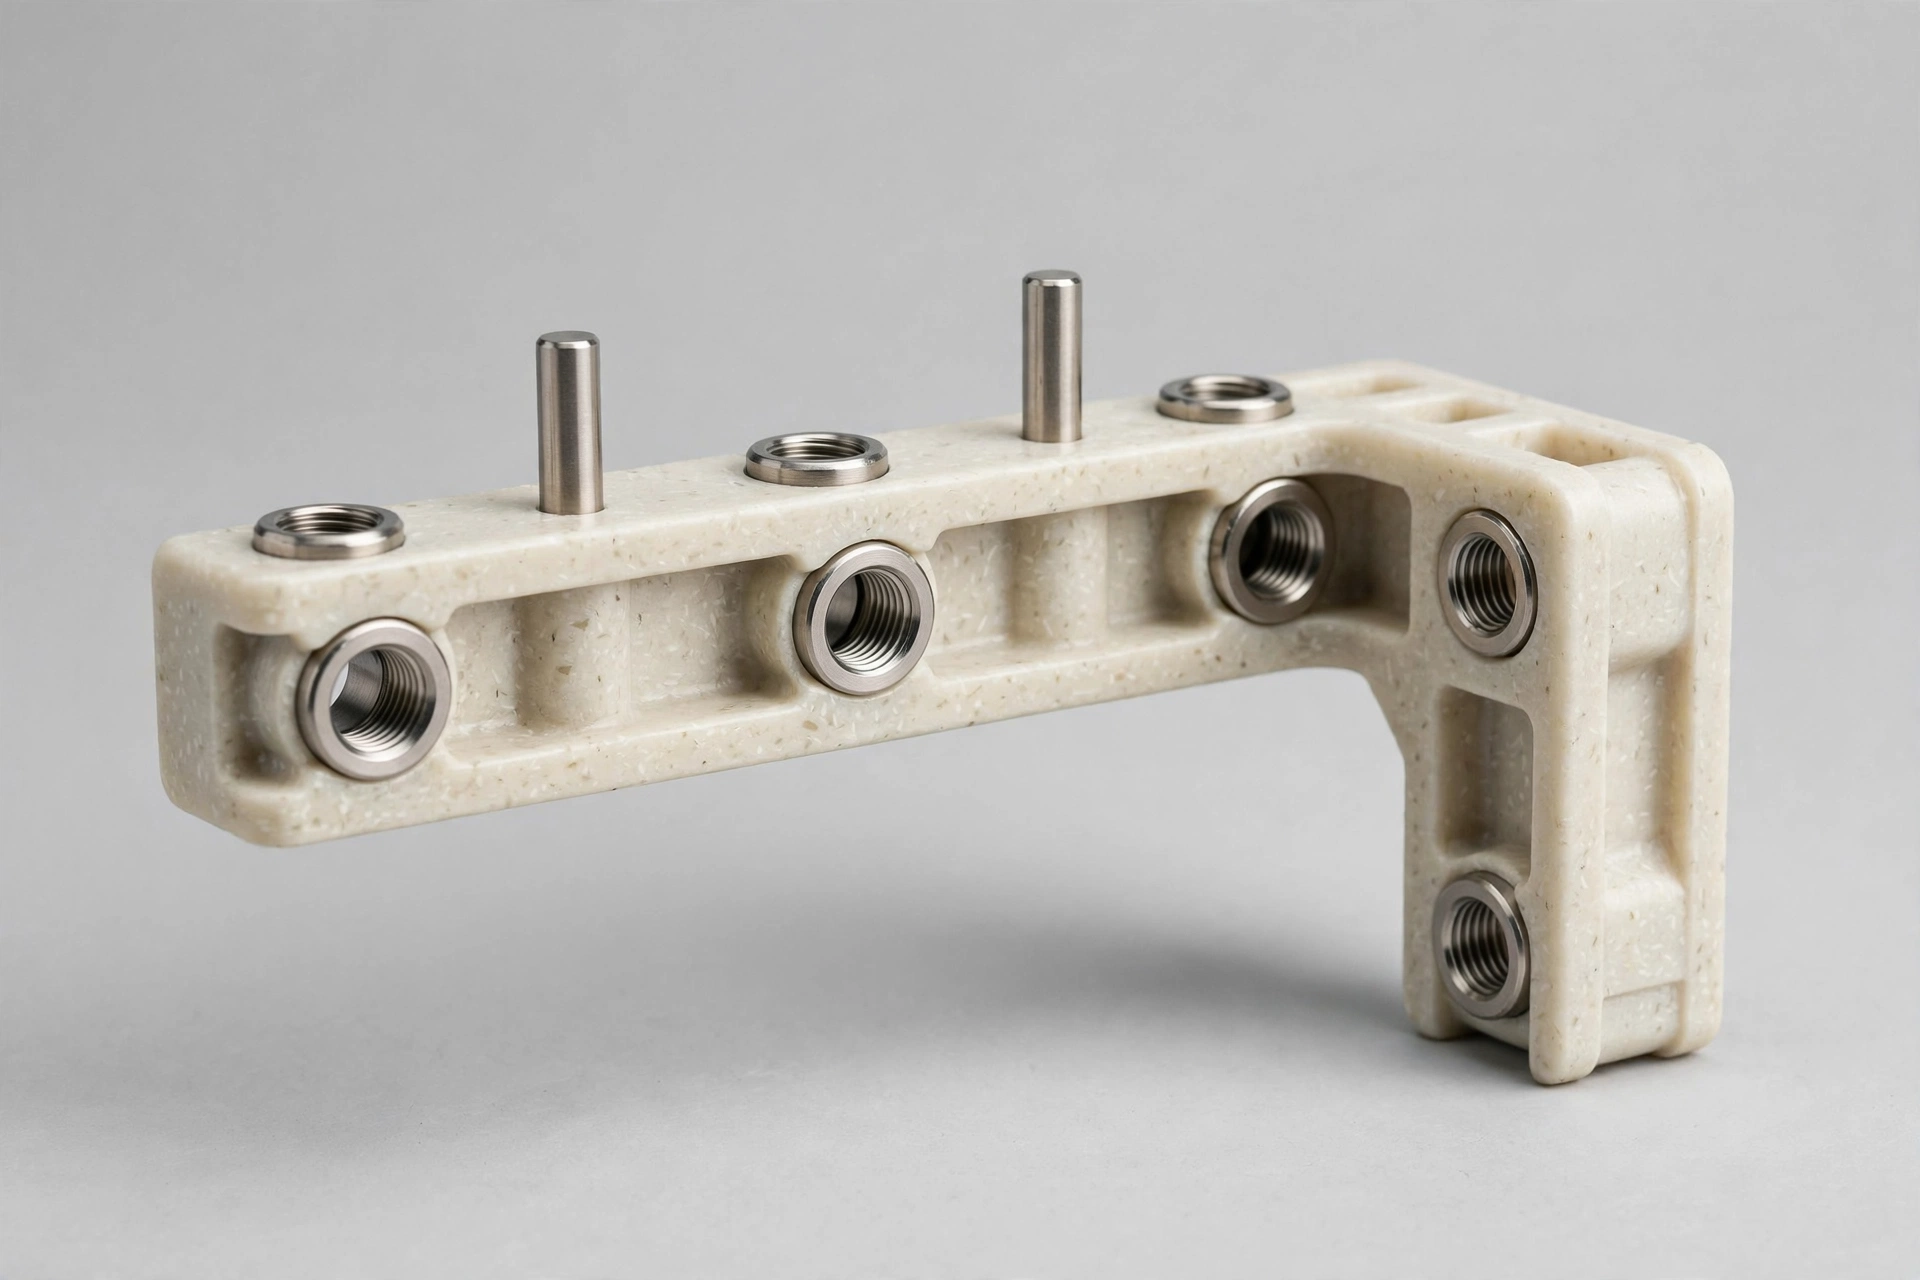
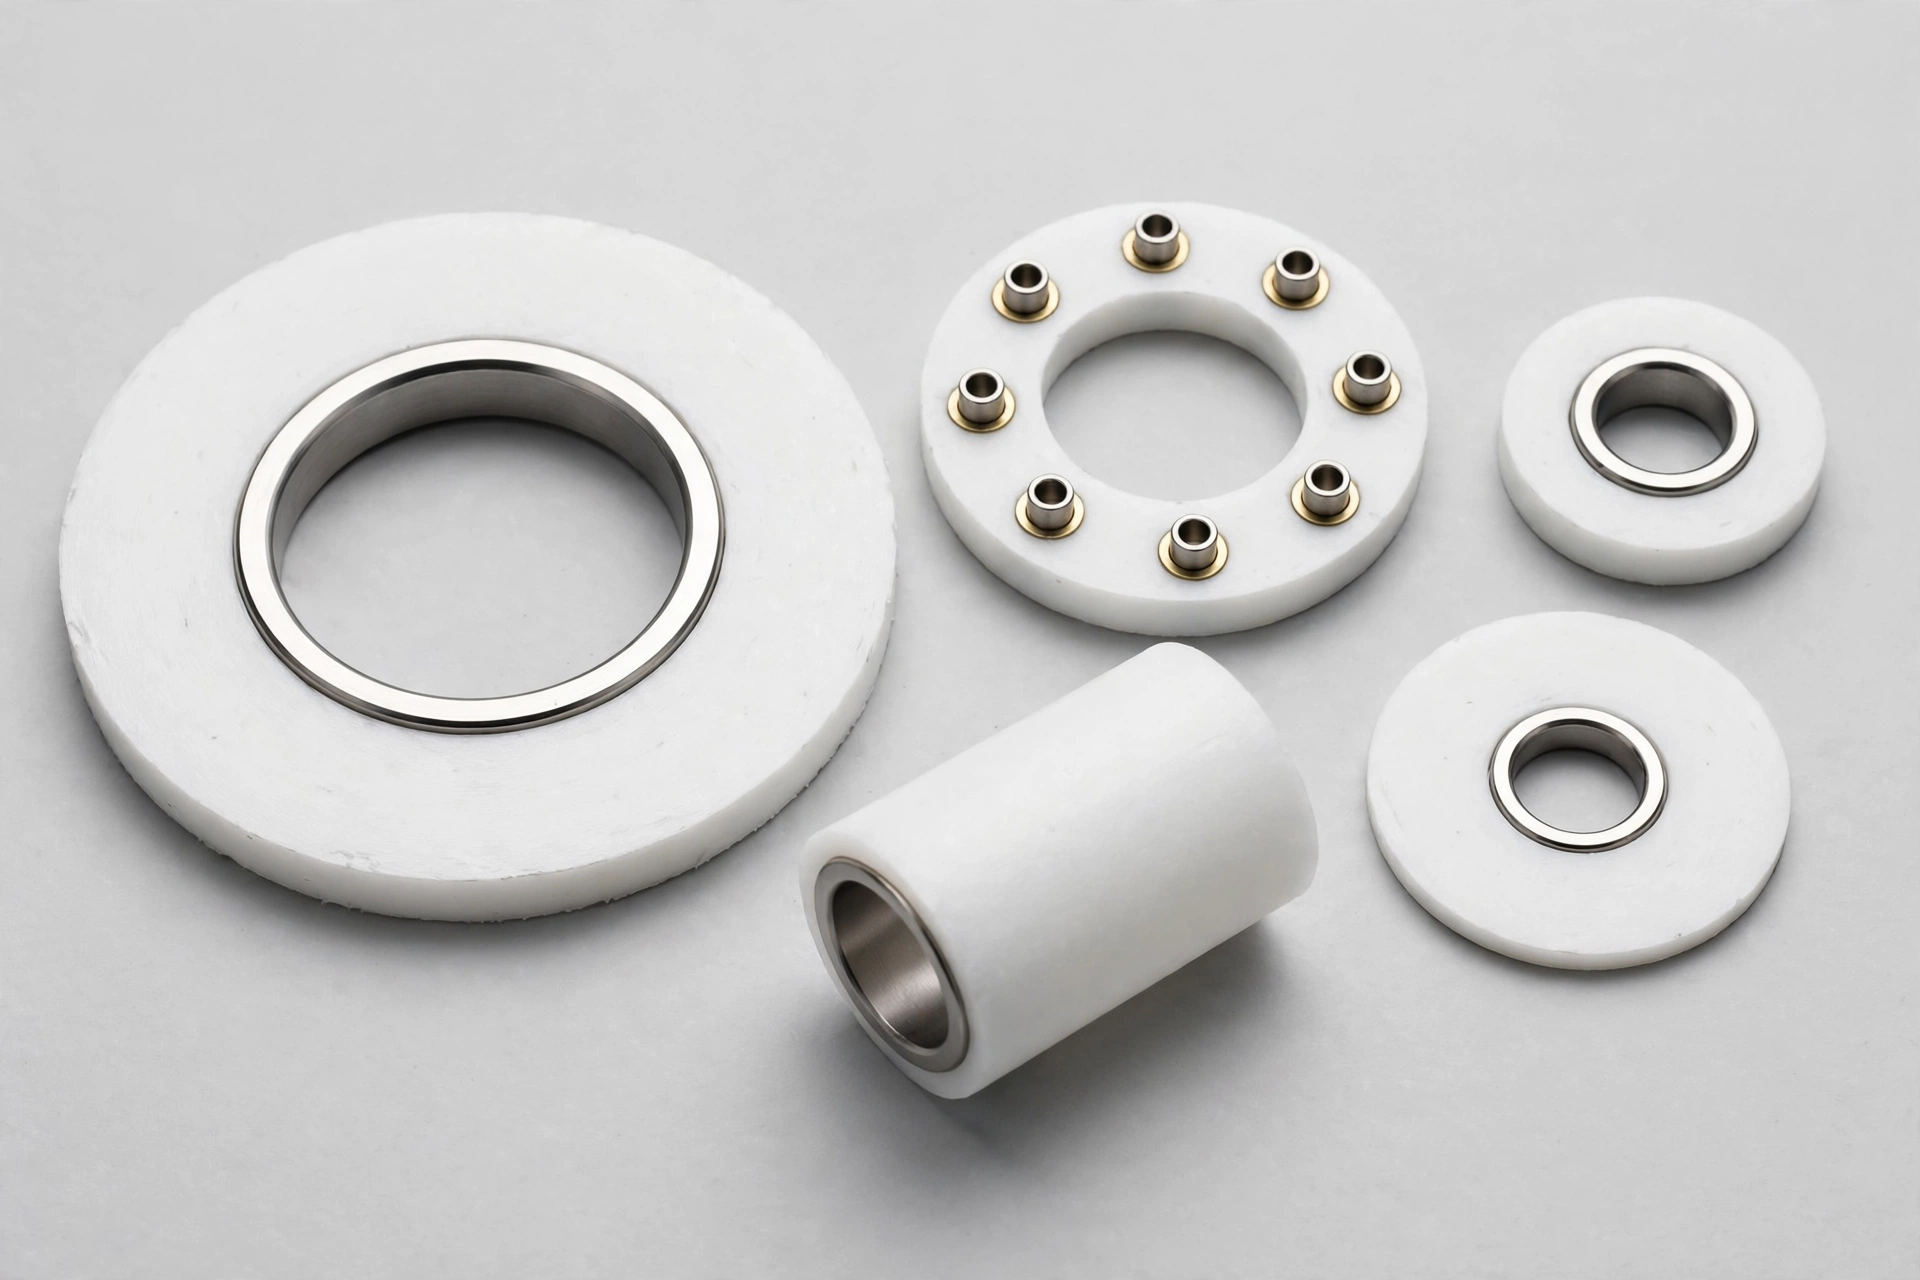
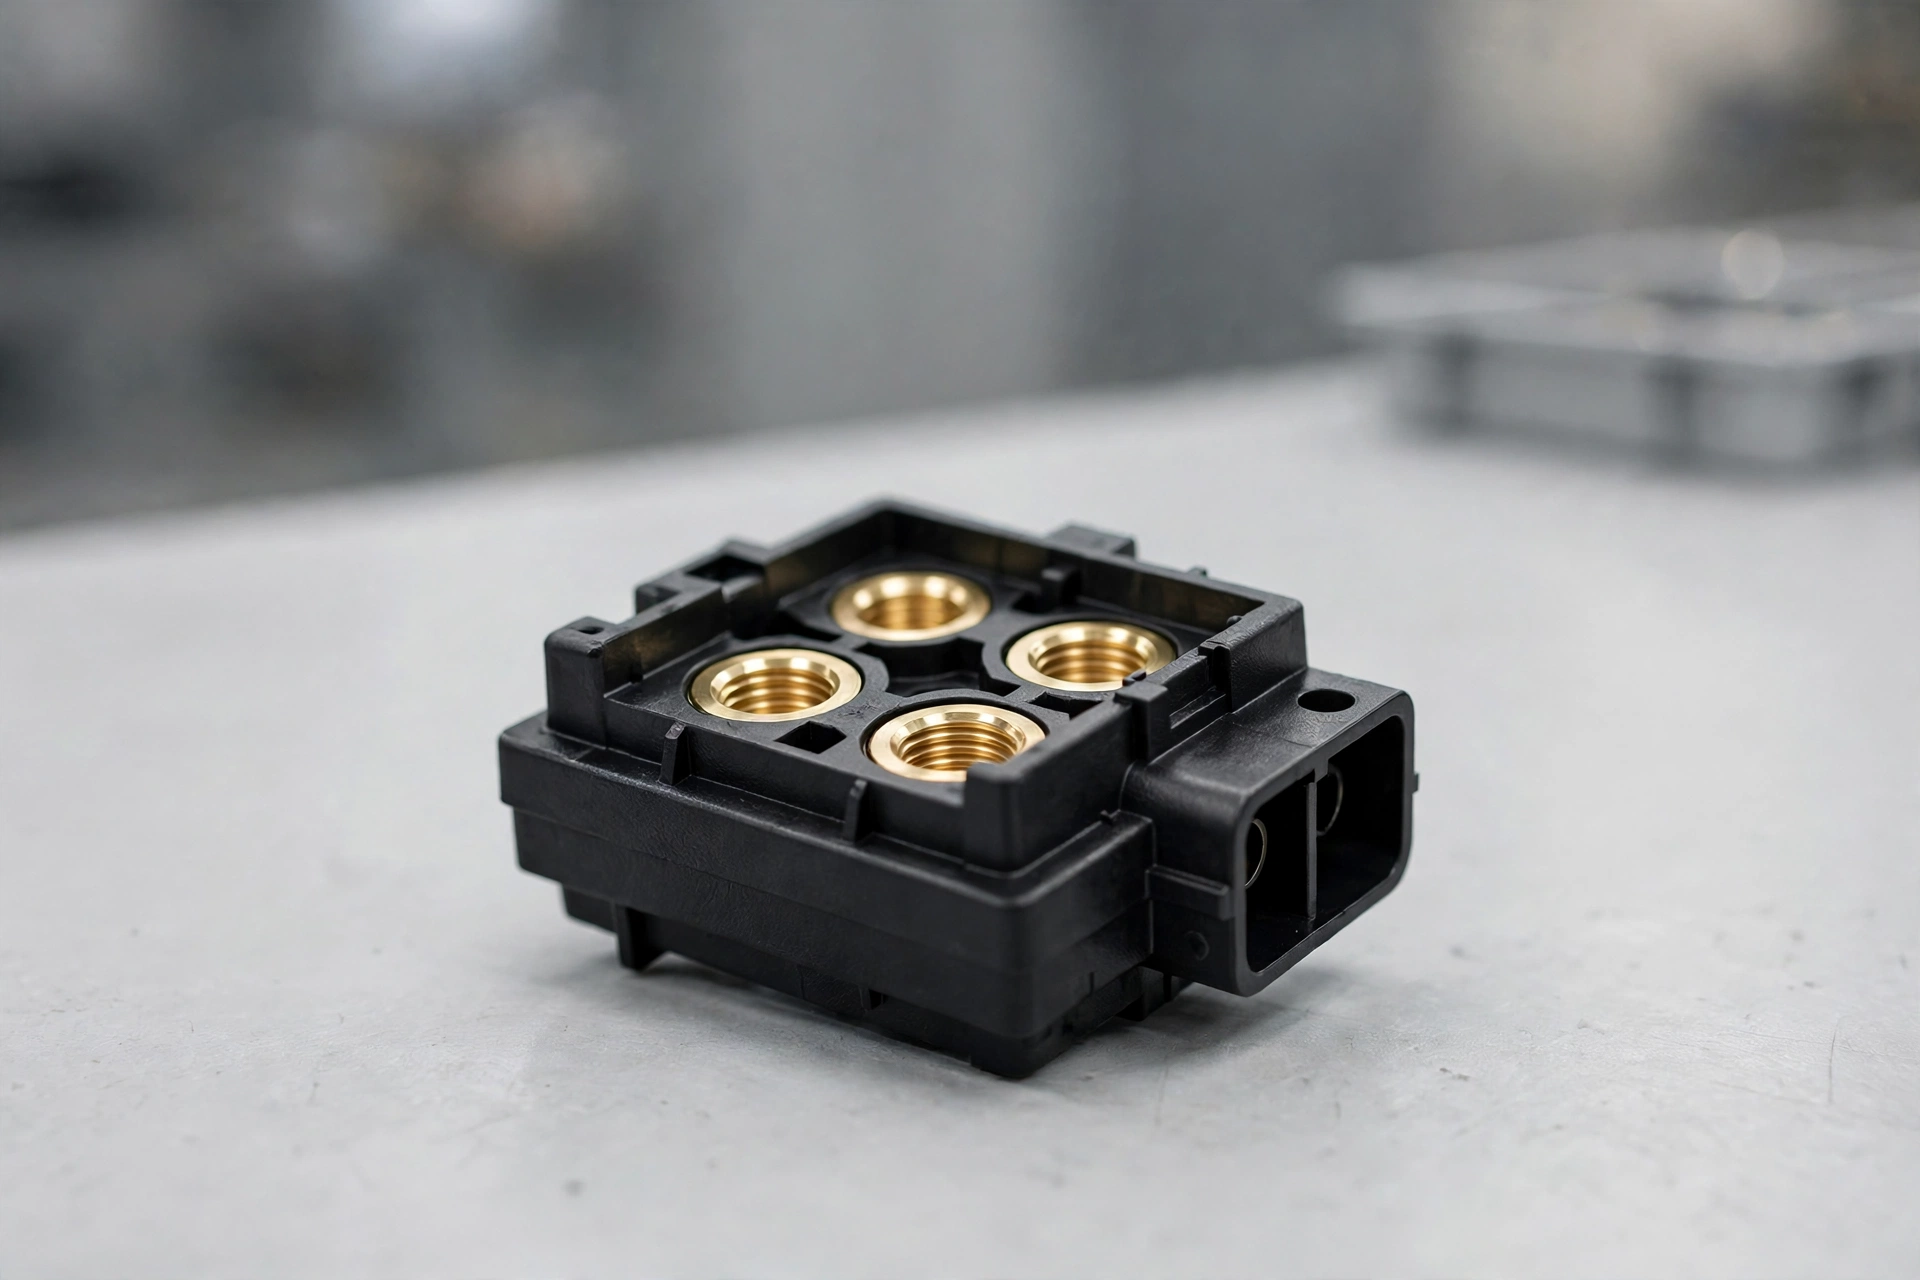
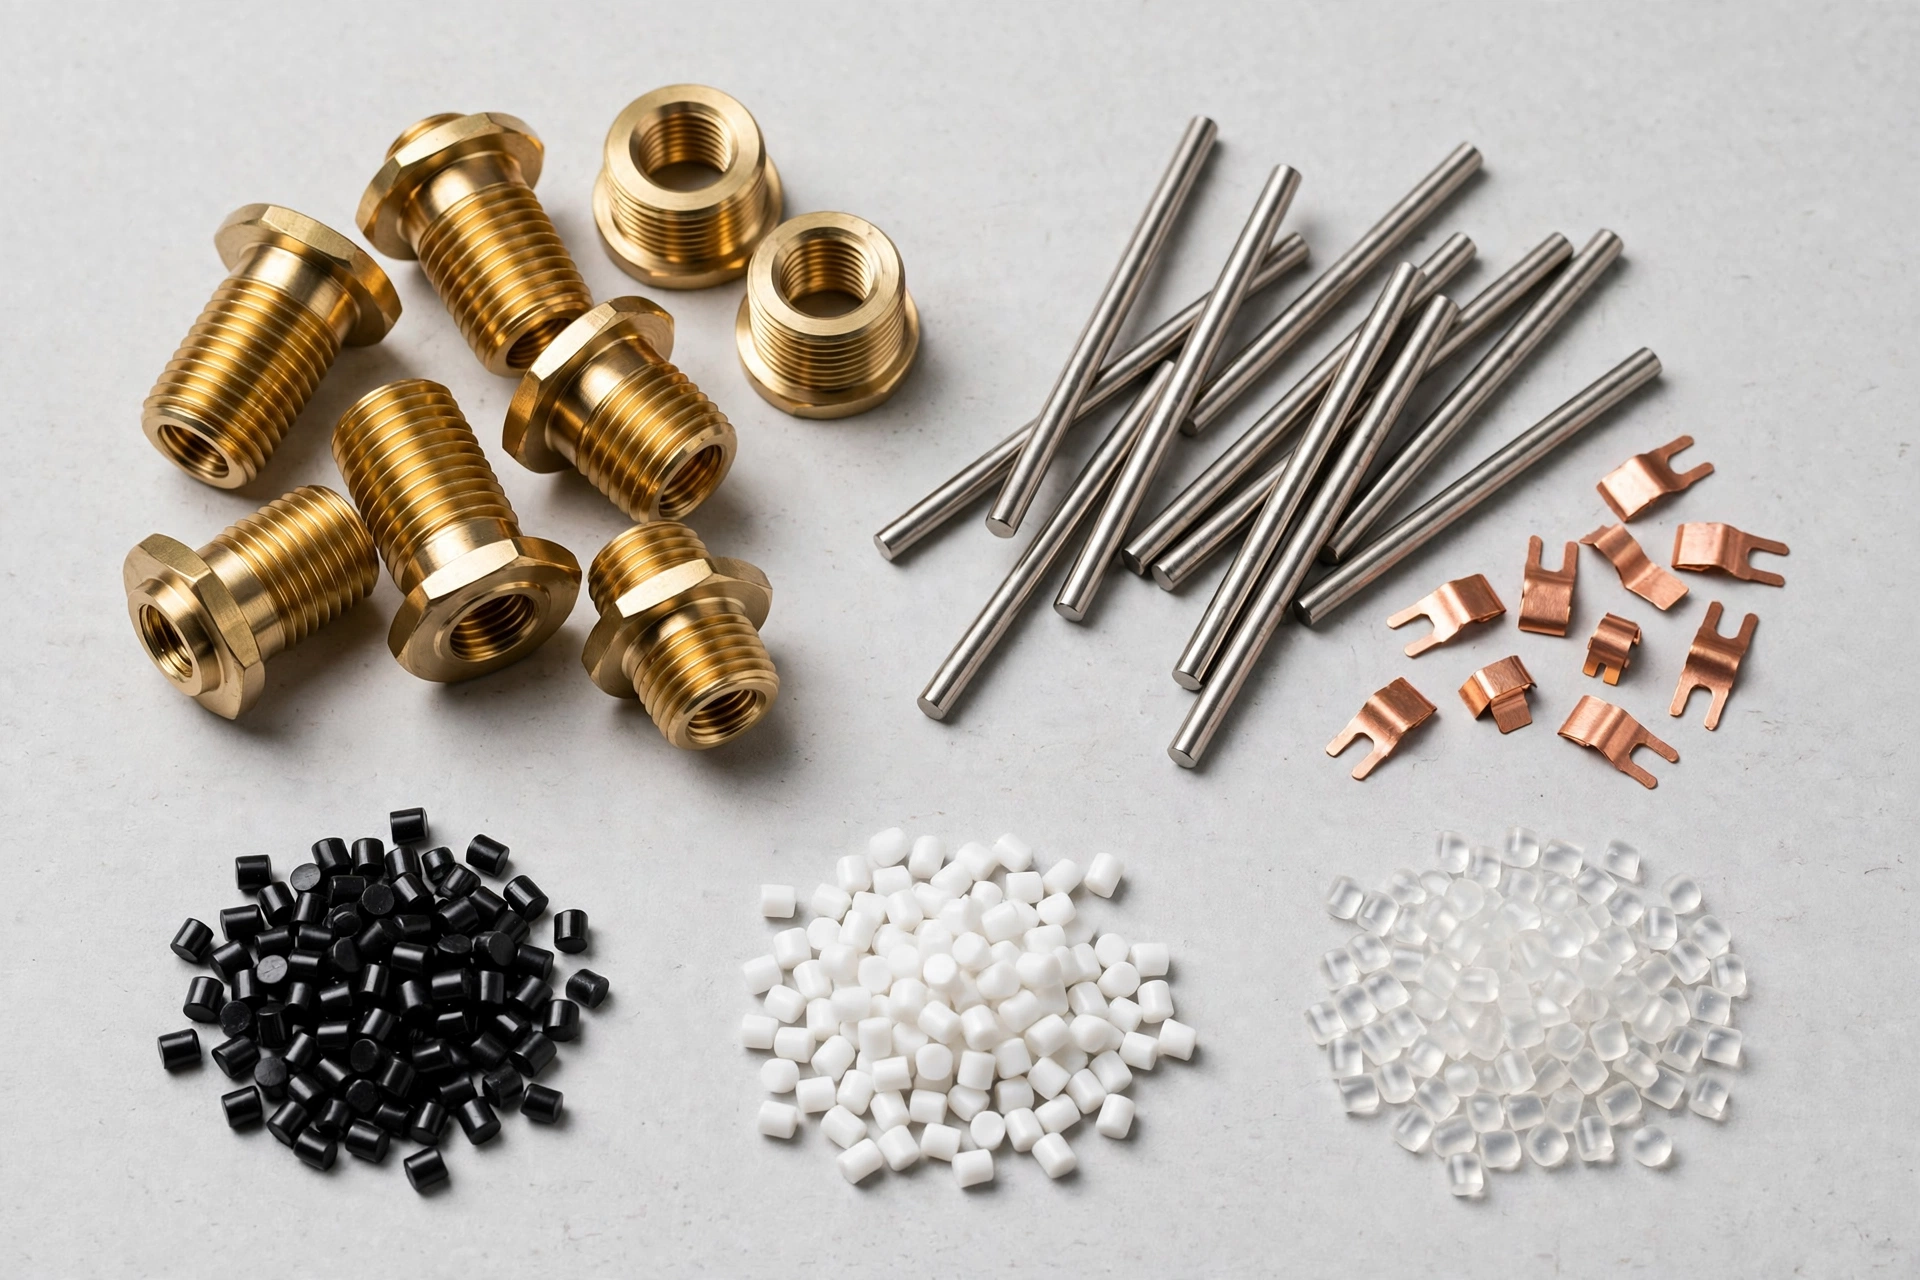
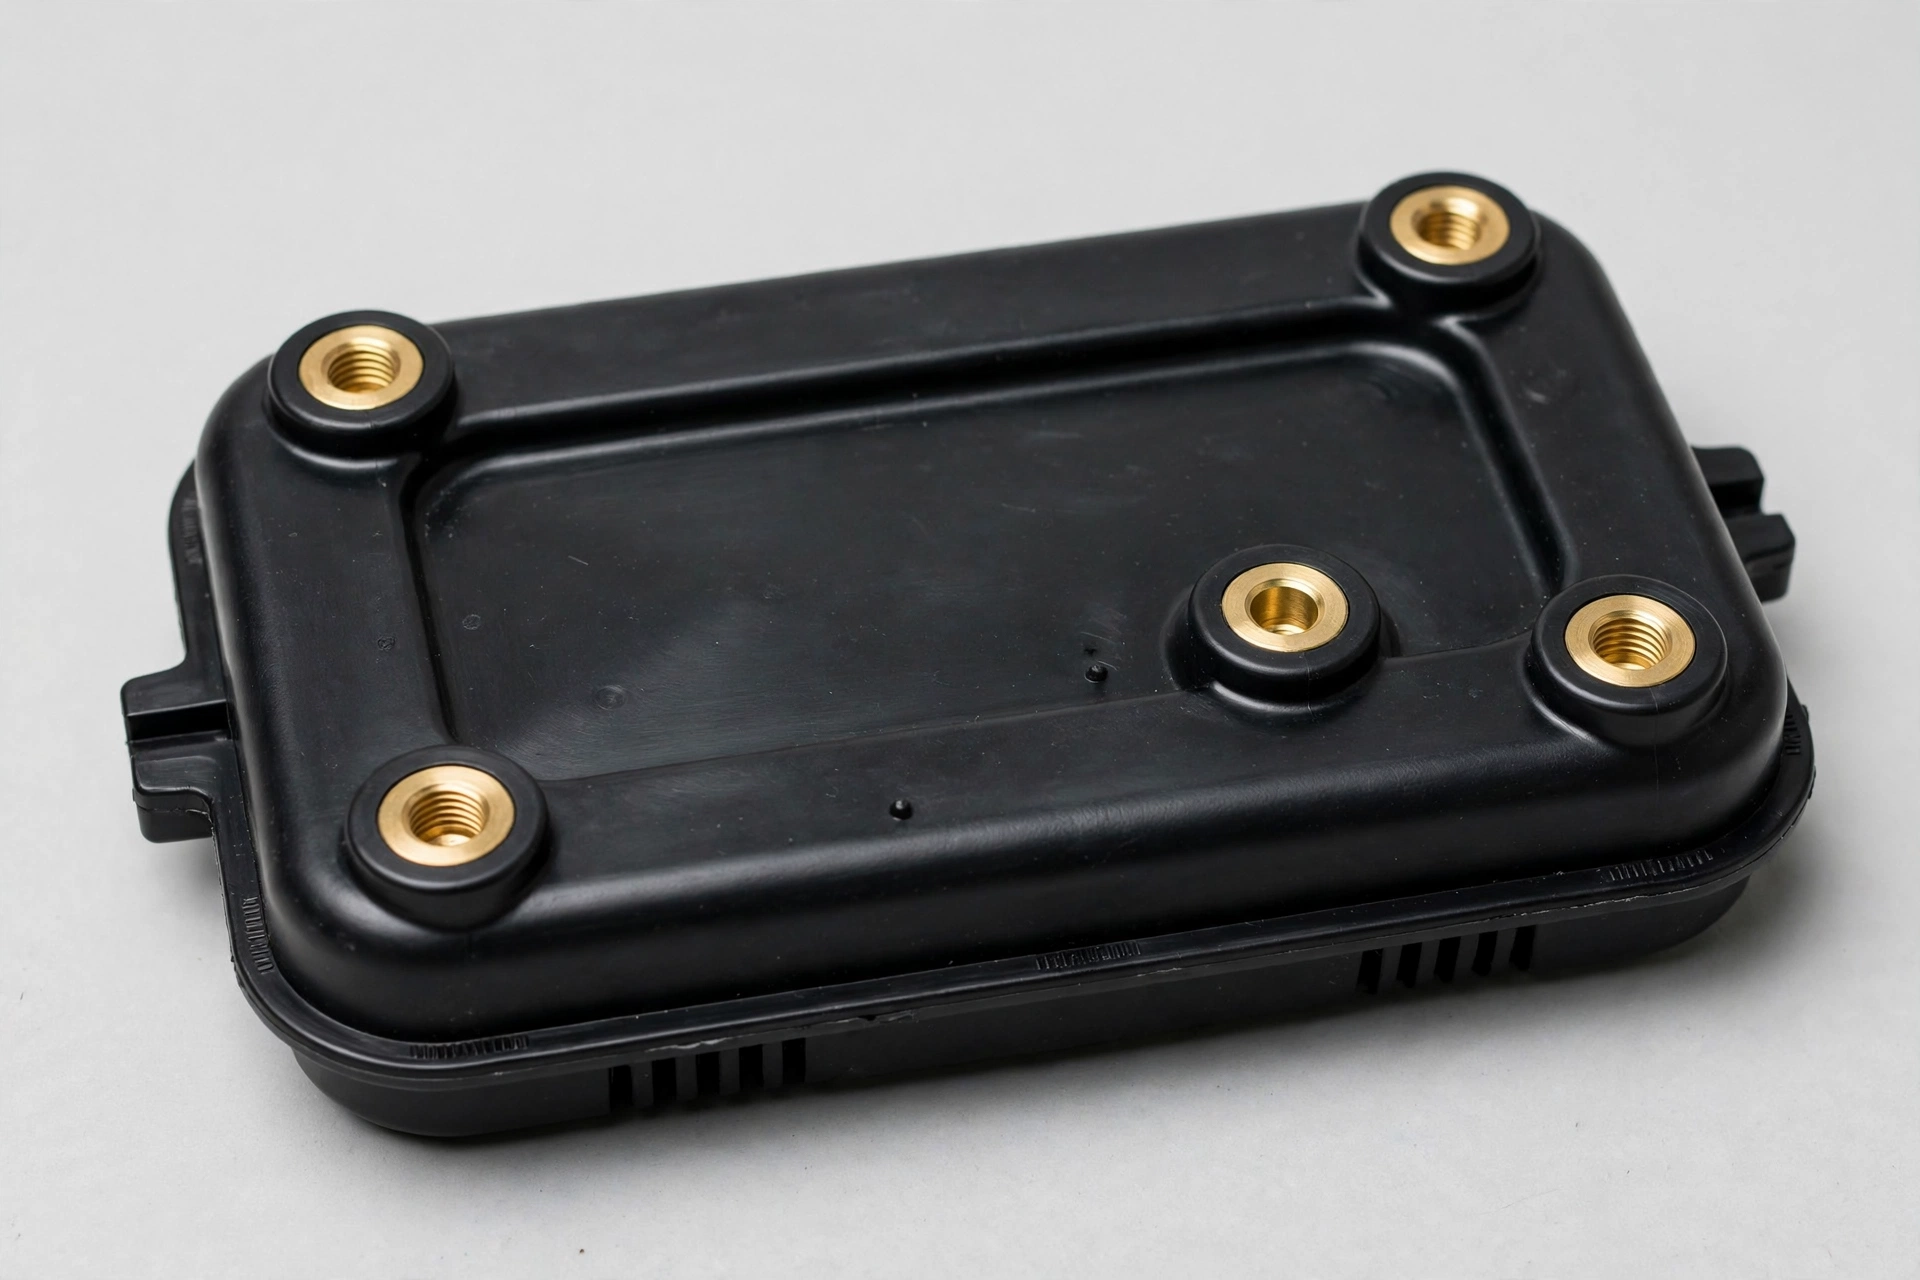
XC Machining provides insert molding services for US product teams. We mold threaded brass inserts, stainless steel pins, copper electrical contacts, aluminum bushings and magnets directly inside injection molded plastic. Insert positional accuracy reaches ±0.020 mm on vertical presses from 55 to 500 tons, with on-press insert verification before every shot.

All uploads are secure and confidential.

Insert Molding - XC Machining

Why Choose XC as Your Insert Molding Partner

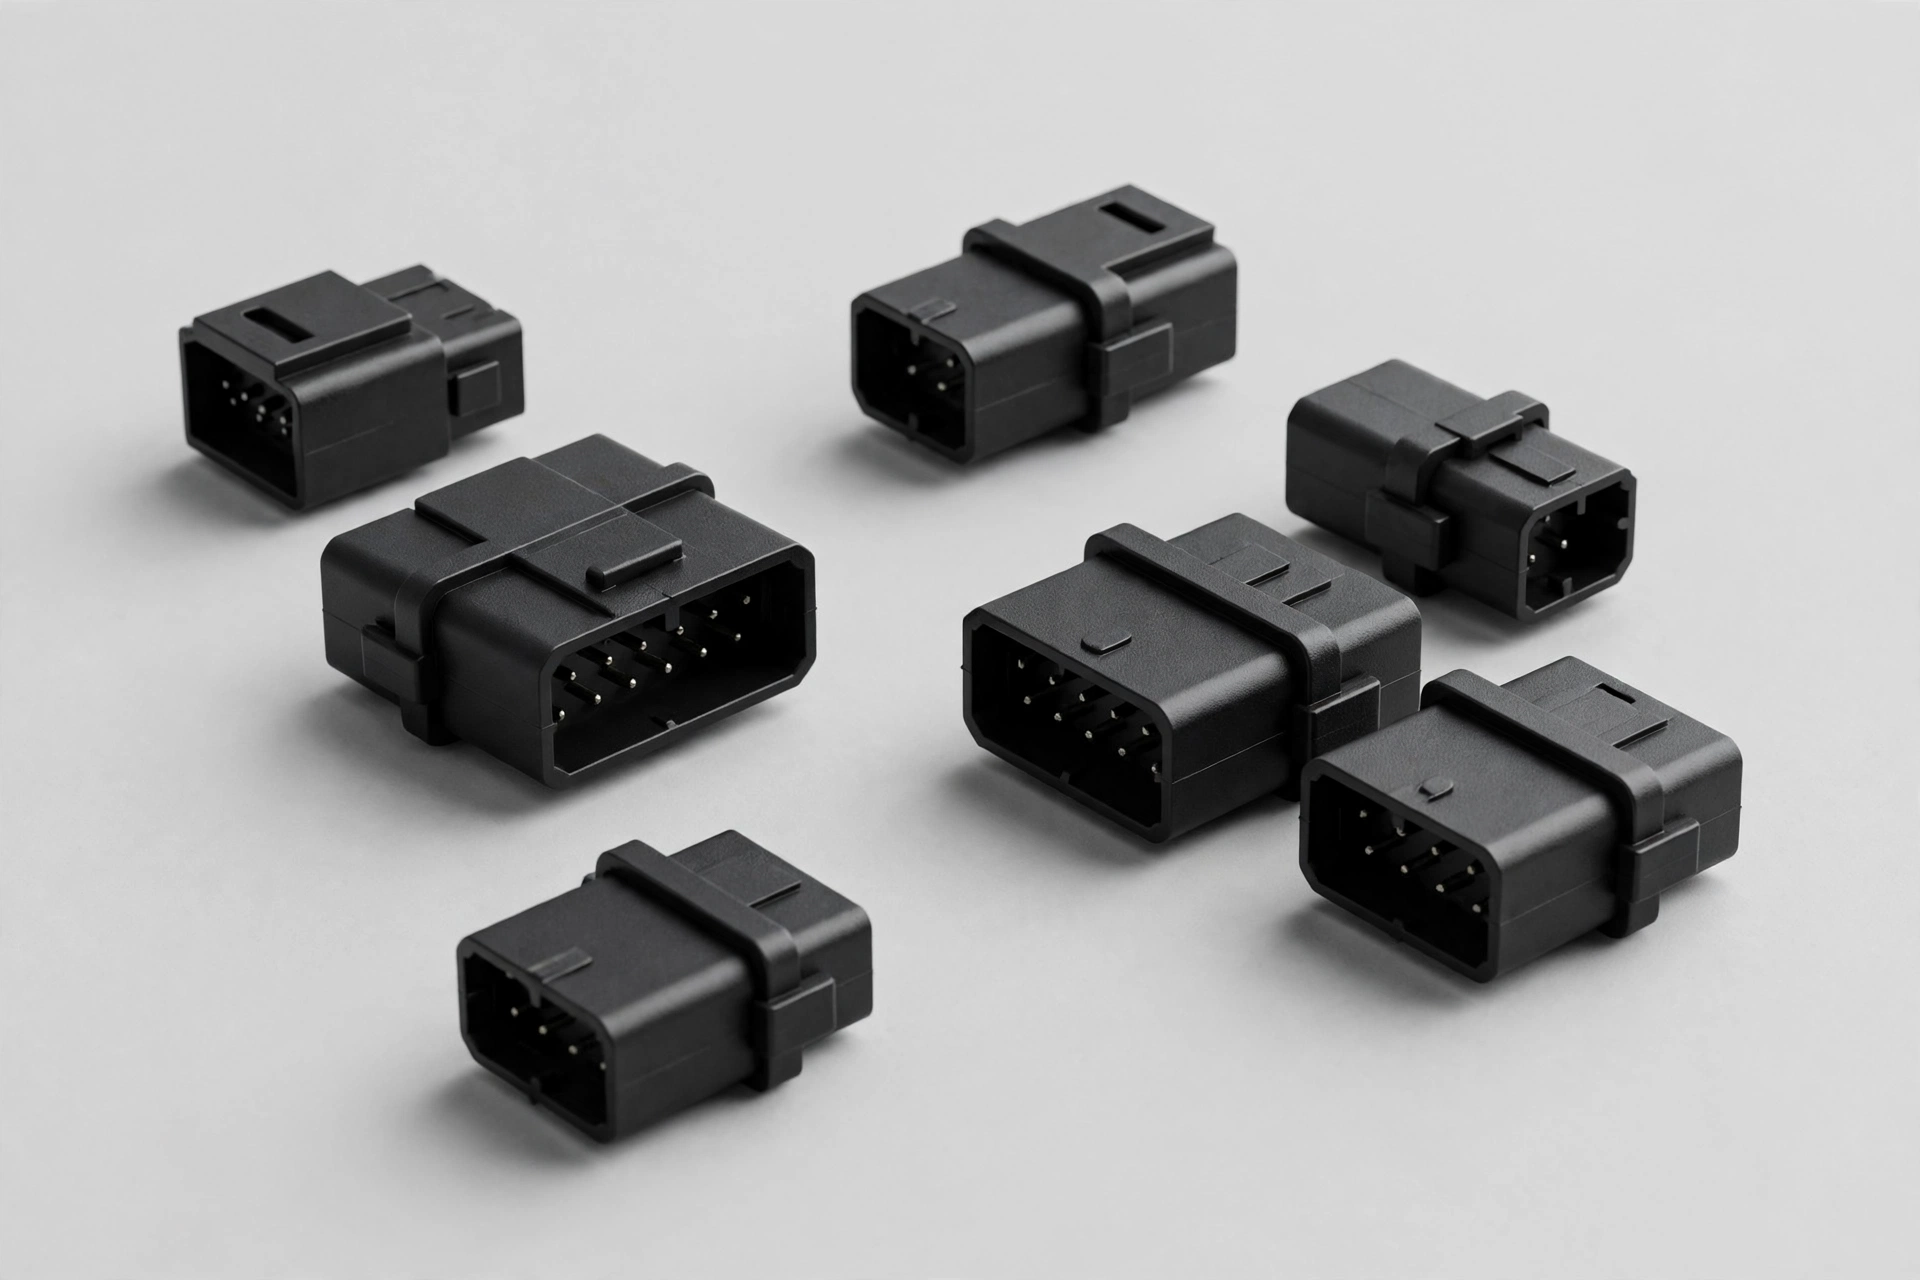
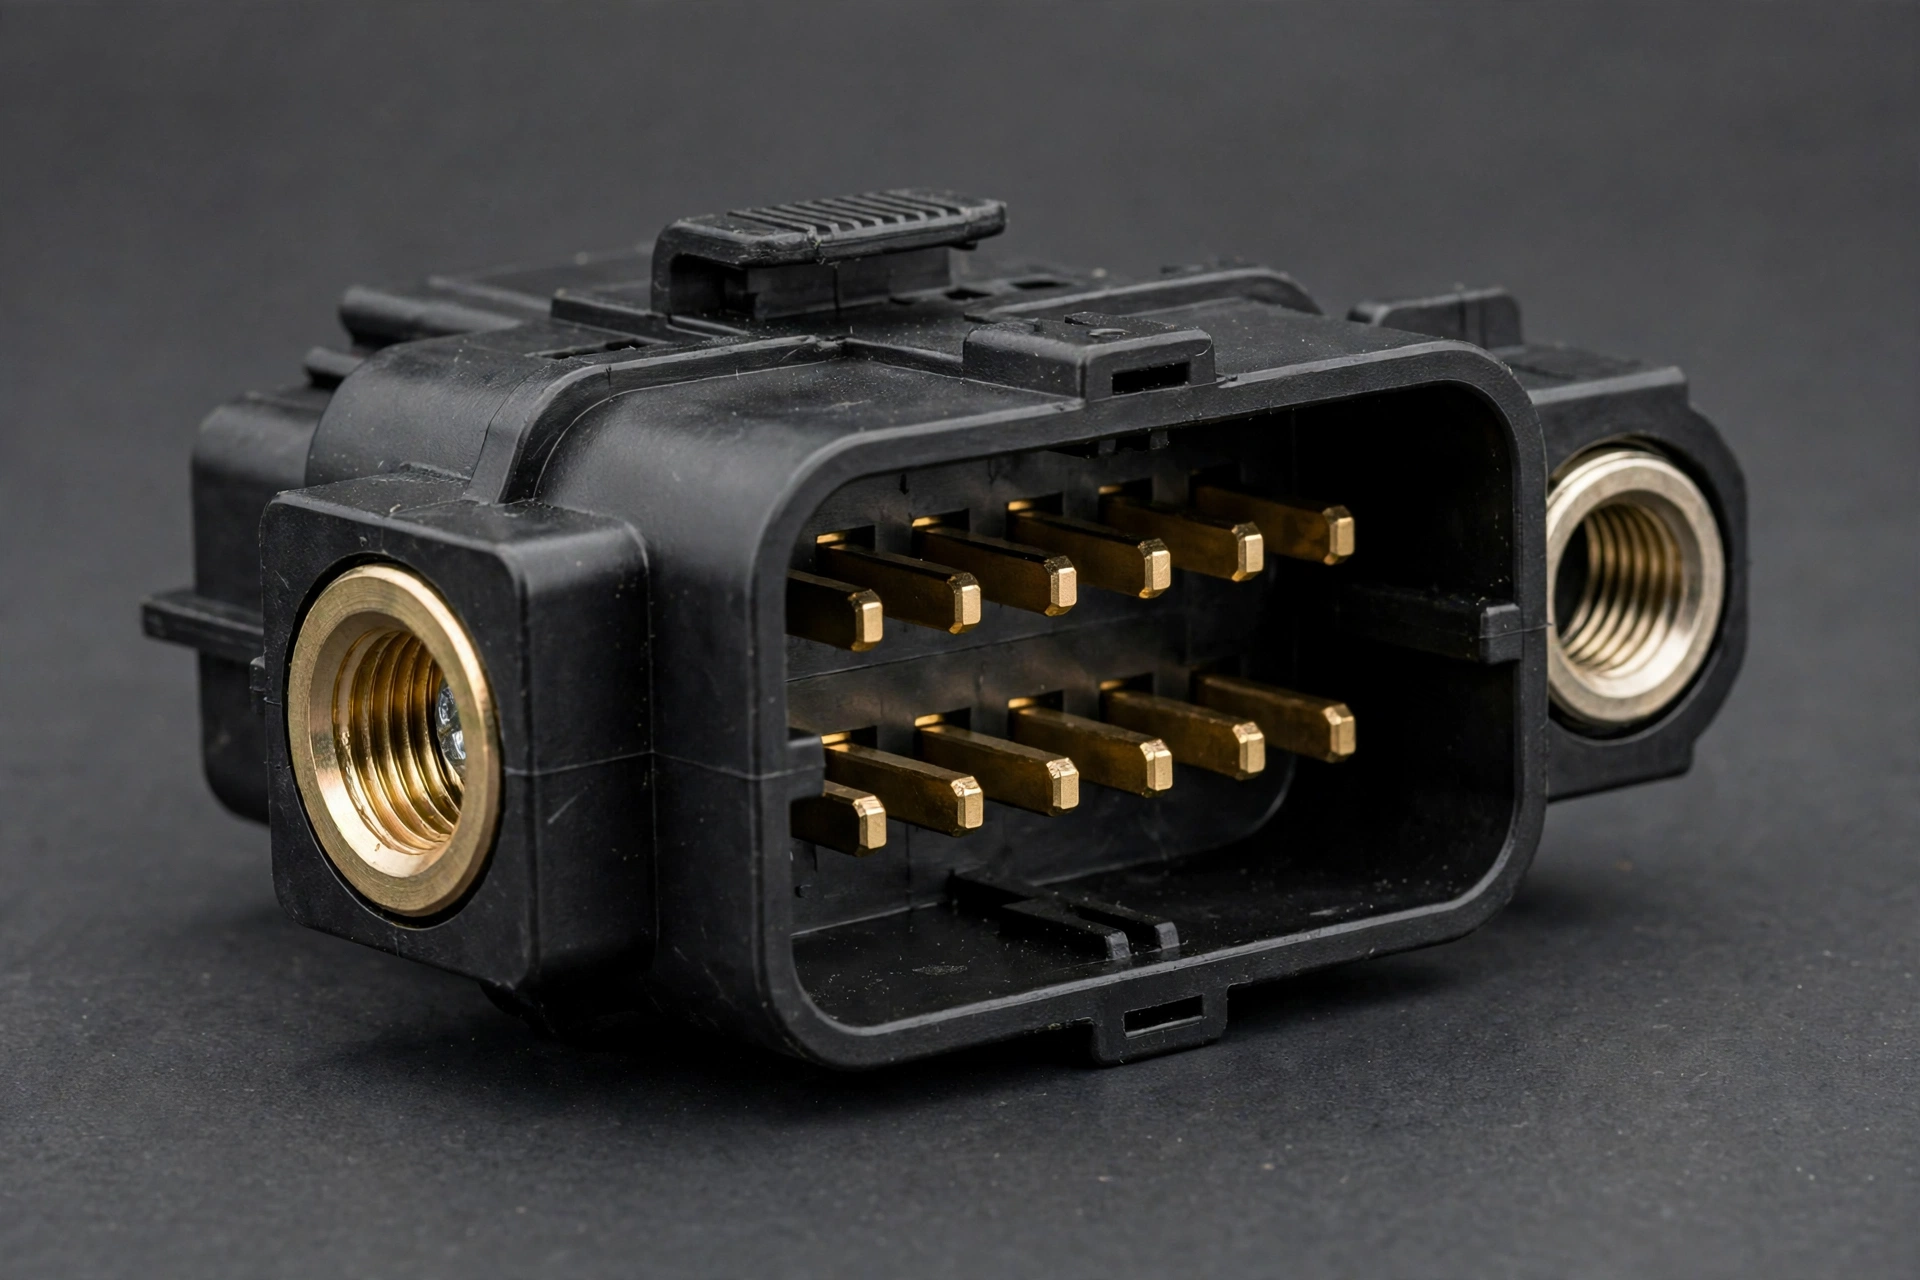
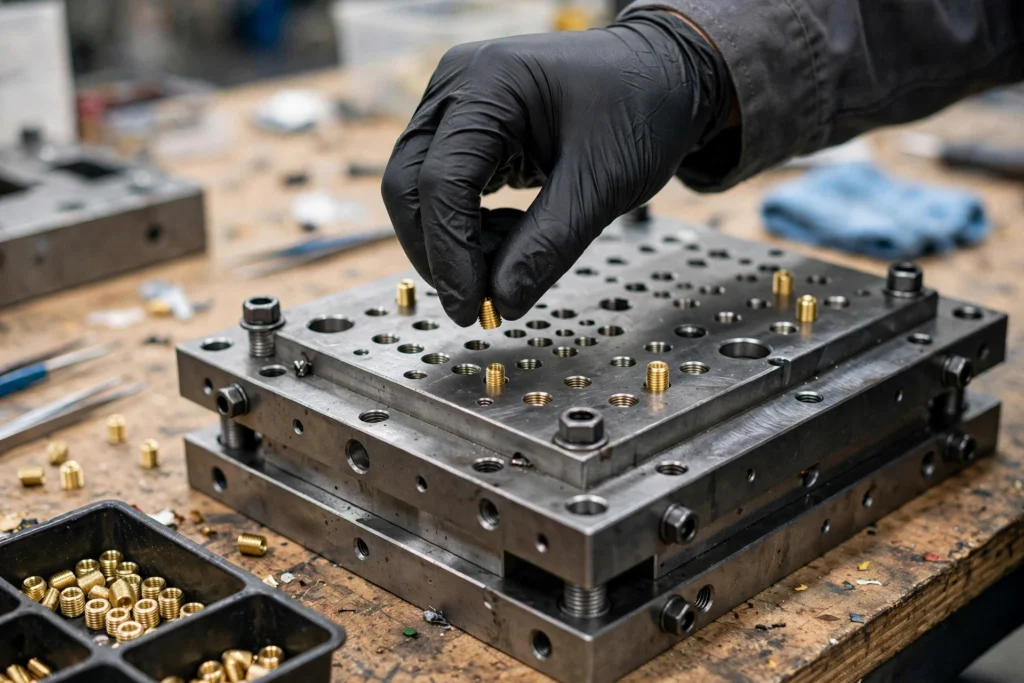
Our insert molding services serve automotive wire harness connectors and medical device housings with embedded contacts. They also serve consumer electronics with threaded fastening points and industrial sensor enclosures with sealed terminals. We make the metal inserts in house by CNC turning and stamping. Then we load them into vertical injection molds by hand or with robotic pick-and-place.

Insert Molding - XC Machining

Production Volumes for Insert Molding

Our insert molding services make parts from 50 prototype units to 500,000+ annual parts. Vertical presses from 55 to 500 tons run single-cavity prototype molds up to 64-cavity production molds. Aluminum prototype tooling ships in 15 days. P20 or H13 steel production tooling ships in 25 to 35 days.

Cycle times run from 20 to 90 seconds per shot. Multi-cavity molds (2 to 64 cavities) multiply the output of each cycle. A 4-cavity mold on a 45-second cycle can reach 7,600+ parts per day on one press, running around the clock.

Insert Molding or Post-Assembly: Which Fits?

Both routes put metal in a plastic part. Our insert molding services cover the first route. The table compares them on the points that decide cost and strength. Our engineers confirm the choice in DFM review.

PointInsert moldingPost-assembly (press-fit, glue, ultrasonic)
Steps after moldingNone. Metal and plastic form one part in a single cycleExtra operation for every insert
Time per part20 to 90 seconds per shot2 to 5 minutes for multi-step assembly
Pull-out force200 to 500 N (knurled brass in glass-filled nylon)30% to 50% lower, by XC’s estimate
Cost at volume20% to 40% lower above 5,000 partsLower tooling cost at small quantities
Best forHigh volume parts that need permanent metal-to-plastic bondsPrototypes and low volume parts

Below a few thousand parts, a post-installed insert can cost less than a mold. For a plain plastic part with no metal, see our injection molding page.

Insert Molding Quality and Capability

XC Machining runs the whole insert molding job under one ISO 9001:2015 certified roof. We machine your metal inserts, design and build the mold, load inserts with vision-verified placement and mold the finished assembly. No insert molding step leaves our building.

Insert Molding - XC Machining
CNC-Machined Inserts In House

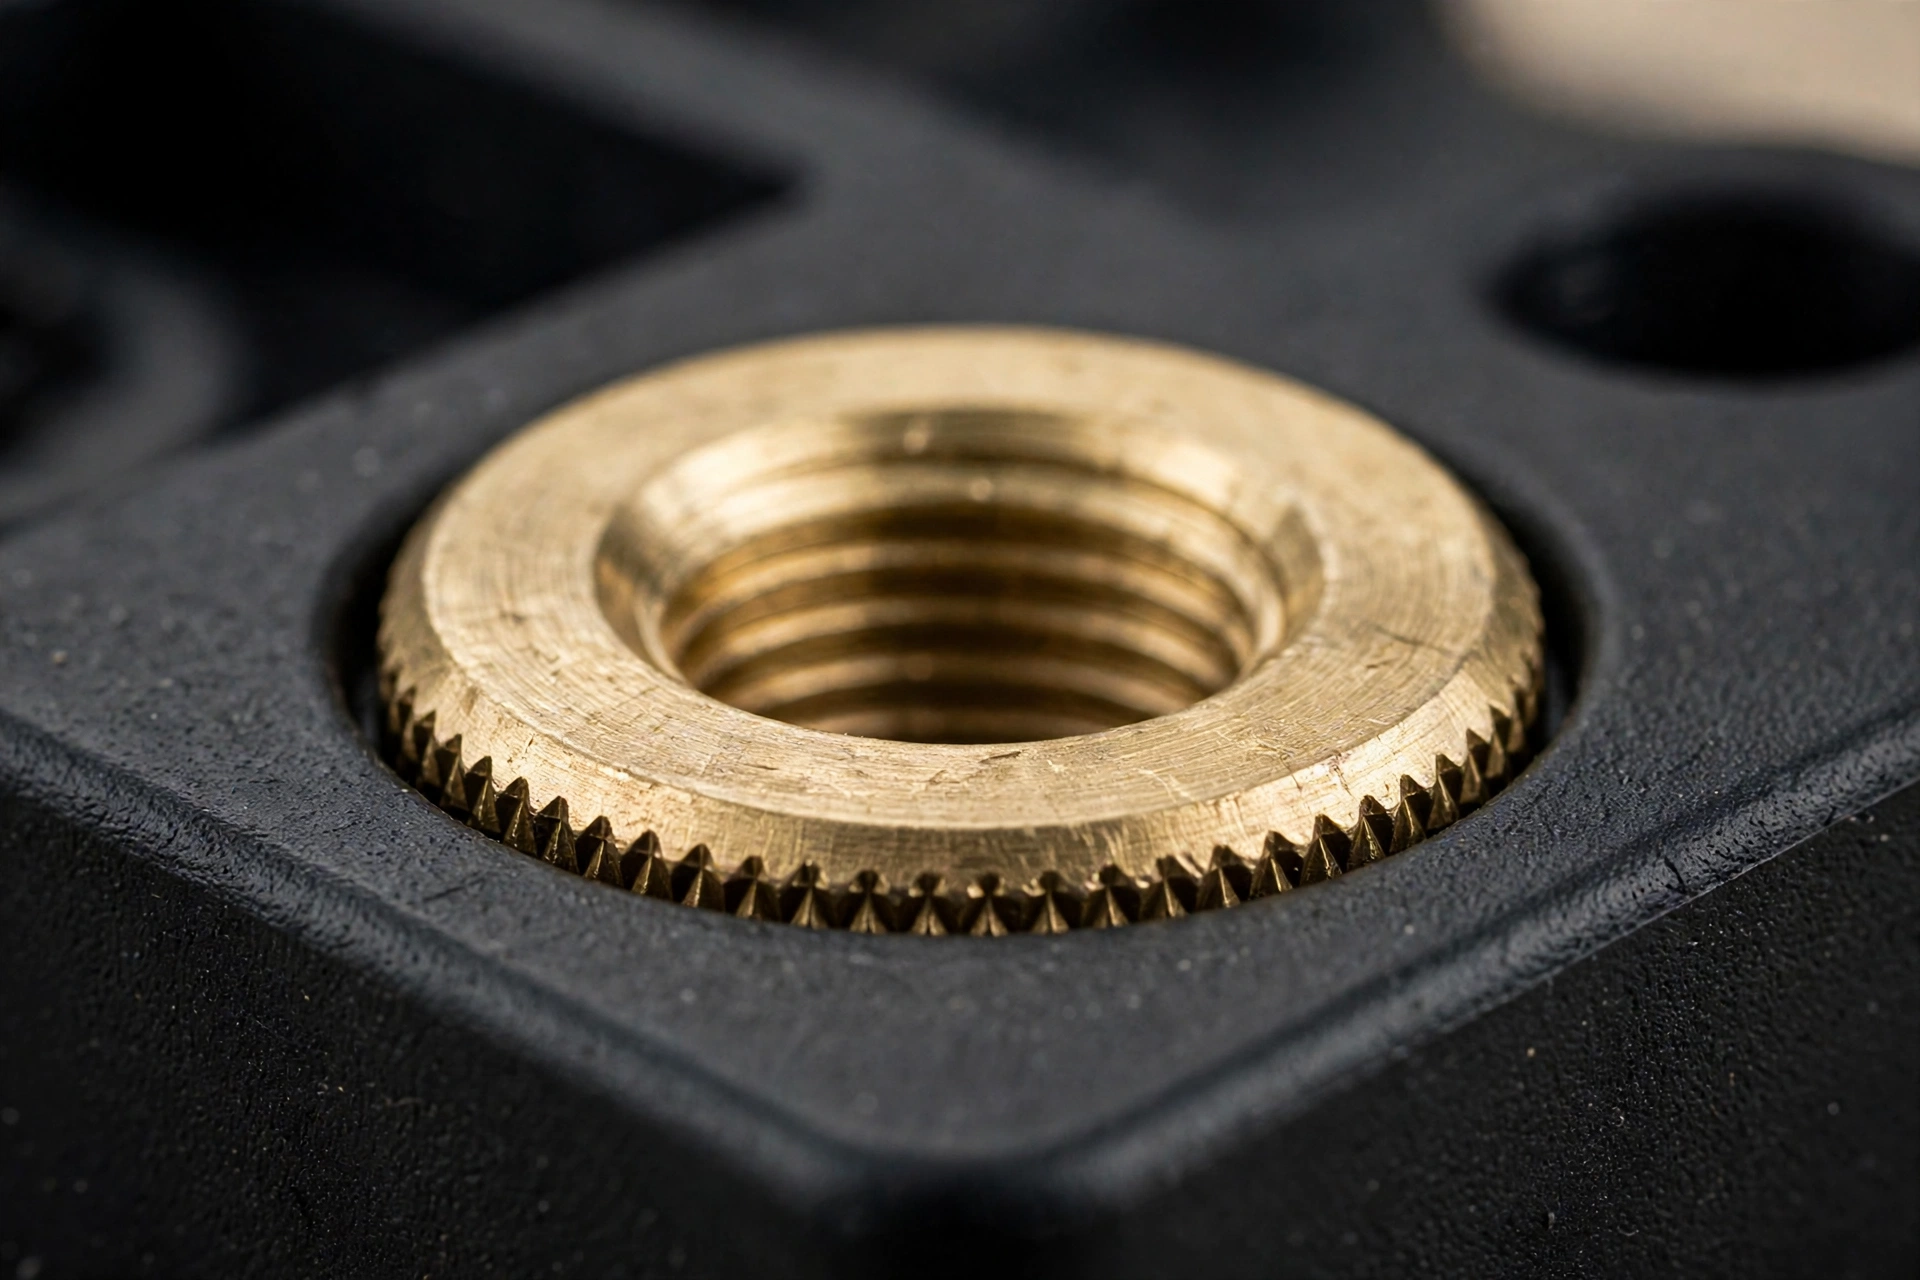
We turn and stamp your metal inserts on site. They include threaded brass inserts (M2 to M12), stainless steel dowel pins, copper bus bar terminals and aluminum standoffs. Diamond knurling (0.5 to 1.0 mm pitch), cross-hatch texture and circumferential grooves raise pull-out resistance. Customer-supplied inserts are also accepted after incoming dimensional inspection. Our CNC turning team makes the round parts.

Insert Molding - XC Machining
40+ Insert Molding Resins

Resins include ABS (general purpose), PC (impact and transparent) and PC/ABS. Glass-filled Nylon 6/66 serves structural parts, PBT electrical parts and POM low-friction parts. PP is low cost, PPS handles heat and PEEK gives extreme performance. TPU and TPE add flexible zones. Insert metal sets the limit. Brass and steel inserts tolerate high-temperature resins. Aluminum inserts need lower melt-temperature plastics.

Insert Molding - XC Machining
Insert Molding DFM Review

Our mold engineers check every design for six points. They check insert-to-wall clearance (minimum 0.5 mm of plastic around every insert surface) and draft angle around encapsulated inserts (minimum 1°). They check the resin flow path, knurl pattern, gate position relative to the insert and thermal expansion mismatch between metal and plastic. A free DFM report arrives within 12 hours.

Insert Molding - XC Machining
Insert Molding Surface Finishes

Mold cavity finishes follow SPI standards. A-1 mirror polish (Ra 0.012 μm) suits transparent housings that show inserts. B-1 to B-3 semi-gloss (Ra 0.05 to 0.1 μm) suits functional parts. C-1 to C-3 stone finish (Ra 0.35 to 1.0 μm) suits industrial parts. D-1 to D-3 textures (Ra 0.8 to 3.2 μm) with Mold-Tech or VDI patterns suit grip surfaces.
Insert Molding Tolerances

XC Machining holds the tolerances below. Standard values suit most parts. Tight values need a DFM review and may add cost.

Molded part dimensionStandard tolerance (mm)Tight tolerance (mm)
Hole diameter (non-critical)±0.100±0.025
Insert location (to edge)±0.100±0.050
Insert concentricity±0.050±0.025
Flatness of insert seating area±0.050±0.025
Insert positional accuracy±0.050±0.020
Wall thickness (nominal)±0.100±0.050
Shaft or boss diameter±0.100±0.050
Mold parting line flash±0.050±0.025

Resins and Metal Inserts We Mold

Insert molding services join a metal or pre-formed insert and a thermoplastic in one molding cycle. Operating temperature, chemical resistance and bond strength with the insert decide the resin.

Thermoplastics

Resins include ABS, PC, PC/ABS, Nylon PA6 and PA66, PBT, POM, PE, PP, PVC and TPE/TPU. Typical uses follow.

  • ABS — consumer electronics housings and automotive interior panels
  • PC — transparent medical device housings and LED light covers
  • Nylon PA66 (glass-filled) — structural automotive connectors and high-load brackets
  • PBT — electrical connectors and sensor housings
  • POM (Delrin) — gear assemblies with metal shaft inserts and low-friction mechanisms

Metal Inserts

  • Brass (C360, C260) — the most common insert material. It machines well and resists corrosion, for threaded inserts, press-fit pins and electrical contacts.
  • Stainless steel (304, 316) — higher strength and corrosion resistance for medical, food-grade and outdoor use.
  • Carbon steel (1018, 1045) — low cost inserts for structural parts where corrosion resistance is not critical.
  • Aluminum (6061, 7075, 2024) — light inserts. Less common, because thermal expansion differs from most resins.
  • Copper (C110) — high electrical or thermal conductivity for electronic assemblies.
Our materials page lists the wider range.

Insert Molding - XC Machining

Surface Finishes for Insert Molded Parts

We apply mold cavity and post-molding finishes. Cosmetic needs, grip and insert visibility decide the finish. Our surface finishing page lists related options.

Insert Molding - XC Machining
As-molded (SPI B-1 to B-3, Ra 0.05 to 0.1 μm)

parts leave the mold ready to use. It costs the least when accuracy matters more than looks.

Insert Molding - XC Machining
Textured (Mold-Tech or VDI, Ra 0.8 to 12.5 μm)

etched into the cavity for leather grain, stipple or wood grain. It improves grip, hides sink marks near inserts and reduces fingerprints.

Insert Molding - XC Machining
Matte (SPI C-1 to C-3, Ra 0.35 to 1.0 μm)

stone-polished cavities give a uniform non-reflective surface for industrial panels and medical housings.

Insert Molding - XC Machining
Polished (SPI A-1 to A-3, Ra 0.012 to 0.025 μm)

diamond-polished cavities give mirror parts for optics, cosmetic electronics and clear housings.

Insert Molding - XC Machining
Bead blasting (Ra 1.6 to 3.2 μm)

glass beads give a satin matte surface on connectors and enclosures.

Insert Molding - XC Machining
Transition blending

smooths the boundary between insert and plastic at the parting line, by gate placement, venting adjustment and post-mold buffing, for a flush seam.

Insert Molding - XC Machining
Sand blasting

an even matte texture on metal inserts that prepares them for coating.

Insert Molding - XC Machining
Brushing

a directional grain on accessible metal surfaces.
Insert Molding - XC Machining
Anodizing

a protective oxide layer and color options on aluminum inserts.

Insert Molding - XC Machining
Powder coating

a durable colored coat on suitable metal parts.

Insert Molding - XC Machining
Polishing

a satin or reflective surface on accessible metal inserts.

Insert Molding - XC Machining
Electroplating

nickel, chrome, zinc or gold on metal inserts for corrosion resistance, conductivity and wear.

Plastic Materials for Insert Molding

XC Machining uses engineering thermoplastics such as ABS, Nylon, Polycarbonate, POM and PEEK. Insert molding gives parts with secure fastening points, electrical connections and steady mechanical performance. Insert fit, bonding needs, dimensional stability and use conditions decide the material.

Insert Molding - XC Machining
ABS

ABS has good impact resistance, stable size and a clean surface. It suits electronic housings, threaded mounting parts, automotive interior parts and consumer products with metal inserts.

Color:
Black, white, natural.
Tensile Yield (MPa)
35 to 55 MPa.
Common Grades
general-purpose, impact-modified and flame-retardant ABS.
Insert Molding - XC Machining
Nylon (PA)

Nylon is tough, wear resistant and fatigue resistant. It suits metal-reinforced brackets, threaded fittings, automotive connectors and industrial assemblies with durable fastening points.

Color:
Natural white, black.
Tensile Yield (MPa)
50 to 90 MPa.
Common Grades
PA6, PA66, PA12 and glass-filled nylon.
Insert Molding - XC Machining
Polycarbonate (PC)

Polycarbonate gives impact resistance, stable size and toughness. It suits protective housings, electrical enclosures, precision connectors and structural parts with metal inserts.

Color:
Transparent, white, black.
Tensile Yield (MPa)
55 to 75 MPa.
Common Grades
general-purpose, optical-grade and flame-retardant PC.
Insert Molding - XC Machining
POM (Delrin)

POM has low friction, wear resistance and stable size. It suits gears, mechanical fittings, precision housings and moving parts with embedded inserts. Plan insert retention and shrinkage with care.

Color:
Natural white, black.
Tensile Yield (MPa)
60 to 80 MPa.
Common Grades
POM-C, POM-H, Delrin 150 and Delrin 500.
Insert Molding - XC Machining
PEEK

PEEK offers heat resistance, chemical stability and strength. It suits aerospace parts, electrical connectors, medical equipment parts and industrial assemblies with metal inserts that run hot.

Color:
Natural beige, black.
Tensile Yield (MPa)
90 to 110 MPa.
Common Grades
unfilled PEEK, PEEK GF30, PEEK CF30 and bearing-grade PEEK.
Insert Molding - XC Machining
PTFE (Teflon)

PTFE has exceptional chemical resistance, low friction and thermal stability. Standard PTFE is not usually injection molded. Parts with embedded inserts need other forming, sintering or mechanical assembly.

Color:
White, black.
Tensile Yield (MPa)
20 to 35 MPa.
Common Grades
virgin, glass-filled, carbon-filled and bronze-filled PTFE.

Specialist Industries

XC Machining is a trusted partner for industries demanding complexity, reliability and precision. Our extensive experience in producing millions of high quality components brings unmatched expertise to every project. Our services cover a diverse range of applications to ensure that we meet the unique needs of each sector with great care.

Our Insert Molding Prototype Manufacturing Capabilities

As a leader in precision manufacturing, we offer a wide range of capabilities that cater to both one-off prototyping and low-volume production. We specialize in delivering geometrically complex and highly cosmetic parts, ensuring the highest quality standards. At XC Machining, we pride ourselves on being the go-to manufacturer for all your Insert Molding needs, providing reliable and efficient solutions under one roof.
With 3, 4, and 5-axis CNC machining services, we can produce complex prototypes and parts with precise tolerances. More than 60+ materials are available for you to choose from.

Provides injection molding for prototypes and custom parts, emphasizing expert support, competitive pricing, and faster production cycles.

Get reliable vacuum casting services for high-quality prototypes and production parts at competitive prices. XC Machining offers highly detailed casting parts with consistent quality.

Uses cutting, bending, and forming techniques to produce precision metal components suited for industrial, commercial, and manufacturing applications.

Get In Touch

Bring Your Designs to Life with XC Machining

Experience precision engineering with XC Machining. From detailed prototypes to high-volume production, we’re here to turn your concepts into reality. Contact us today to discuss your project needs!

Get In Touch With Us!
Prompt response guaranteed within 12 hours

Insert Molding FAQs

Choose it when the design needs metal bonded inside plastic, such as threaded inserts, contacts, bushings or pins. It also fits when press-fitting, gluing or ultrasonic insertion adds cost or lowers reliability. Choose it when pull-out or torque needs exceed post-mold installation, and when volume justifies the mold. Automotive connectors, medical devices and consumer electronics use it widely.

It cuts cost three ways. It removes assembly labor, because nothing is pressed, glued or installed after molding. It reduces part count by joining metal and plastic in one part. It speeds production with 20 to 90 second cycles against 2 to 5 minutes of multi-step assembly. Savings of 20% to 40% are typical above 5,000 parts.

The plastic forms a mechanical bond and full surface contact with the insert during injection. Knurled brass inserts in glass-filled nylon reach pull-out forces of 200 to 500 N. Torque-out resistance is 2 to 8 N·m, by diameter and knurl pattern. XC estimates this beats ultrasonic or press-fit inserts by 30% to 50%.

Yes. We mold copper, brass and phosphor bronze contacts, terminals and bus bars directly into plastic housings. Uses include automotive wire harness connectors with 4 to 64 pins, PCB header connectors, sensor housings with molded-in terminals and industrial switchgear parts. Every insert molded electrical part gets electrical continuity testing.

We check six points. They are insert position by CMM (±0.020 mm), pull-out force to your specification and torque-out of threaded inserts. We also inspect for flash, sink marks and exposed inserts (100% on critical parts), test continuity of molded-in contacts and check dimensions against CAD. Production orders include first-article inspection reports.

Insert molding places a metal insert in an open mold cavity and injects plastic around it. The result is a metal-in-plastic assembly. Overmolding bonds a soft plastic (TPE, TPU, LSR) over a rigid plastic base, giving a multi-material plastic part. Insert molding adds structural metal. Overmolding adds grip and sealing. XC Machining offers both.

We make custom metal inserts in house by CNC turning, CNC milling and metal stamping. They include threaded inserts (M2 to M12), dowel pins, electrical terminals, bushings and custom shapes per your drawing. We also accept customer-supplied inserts. Each incoming batch gets dimensional inspection before loading, to confirm it fits the mold cavity.

CNC Manufacturing Resources