Injection Molding Services

XC Machining provides injection molding services for US product teams that need production-grade plastic parts. We mold ABS, PC, Nylon, PP, PEEK and 50+ thermoplastic resins on presses from 50 to 800 tons. Typical tolerance is ±0.127 mm. Critical dimensions can reach ±0.05 mm, depending on resin and part design.

All uploads are secure and confidential.

Injection Molding - XC Machining

Prototype Injection Molded Parts in 15 to 20 Days

Our injection molding services for prototypes use aluminum 7075 rapid tooling. Prototype molds ship in 15 to 20 business days with T1 samples for size approval. They produce 500 to 5,000 parts for design checks, material tests and pre-production validation before you invest in hardened steel tooling.

Molded plastic parts can have walls from 0.5 mm and tolerances to ±0.05 mm. Surface finish runs from SPI A-1 (mirror) to D-3 (textured). For metal inserts or tight-tolerance features, our CNC machining services work directly with the molding process.

Injection Molding - XC Machining

Plastic Part Capabilities and Press Range

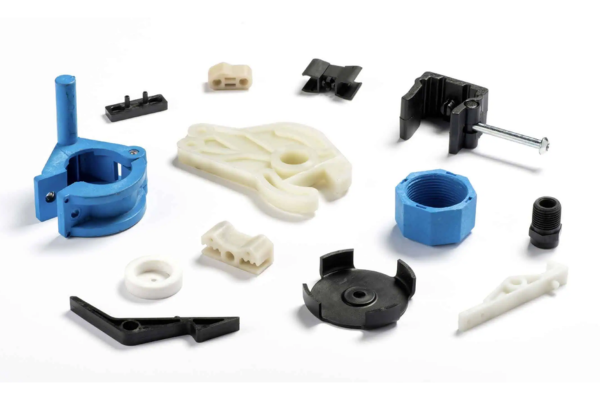
XC Machining molds plastic parts for automotive, medical device, consumer electronics and industrial applications. Our presses run from 50 to 800 tons of clamping force. Parts range from 5 x 5 x 2 mm to 1000 x 1000 x 500 mm, in single-cavity, multi-cavity and family mold layouts.

Functional prototypes arrive as T1 samples from aluminum tooling. Every prototype part goes through CMM dimensional verification against your CAD model before it ships.

Why Choose XC for Injection Molding

Our injection molding services combine ISO 9001:2015 quality procedures and in-house mold design and fabrication. Every project gets a DFM review, and presses run from 50 to 800 tons. One team handles the mold and the molded part, so design changes reach the tool without a handoff.

Injection Molding - XC Machining
In-House Mold Fabrication

We design and build molds in house. Aluminum 7075 serves prototypes for 5,000 to 10,000 shots. P20 pre-hardened steel runs 100,000+ shots, and H13 hardened steel runs 500,000+ shots. S136 stainless steel reaches 1,000,000+ shots and suits corrosive resins. Our injection mold tooling page covers the tool build in depth.

Injection Molding - XC Machining
50+ Moldable Resins

Moldable resins include ABS, PC, PC/ABS, Nylon 6/66, PP, PE, POM (Delrin), PMMA, PBT, PPS, PEEK, TPU, TPE and LSR (liquid silicone). Glass-filled and carbon-filled engineering compounds are also available. Our materials page lists the wider material range.

Injection Molding - XC Machining
Injection Molding DFM Review

Our mold engineers check wall thickness uniformity, draft angle (minimum 0.5°), gate location, sink marks, weld lines and ejector pin placement. DFM feedback arrives within 12 hours of file upload.

Injection Molding - XC Machining
Molded Part Surface Finishes

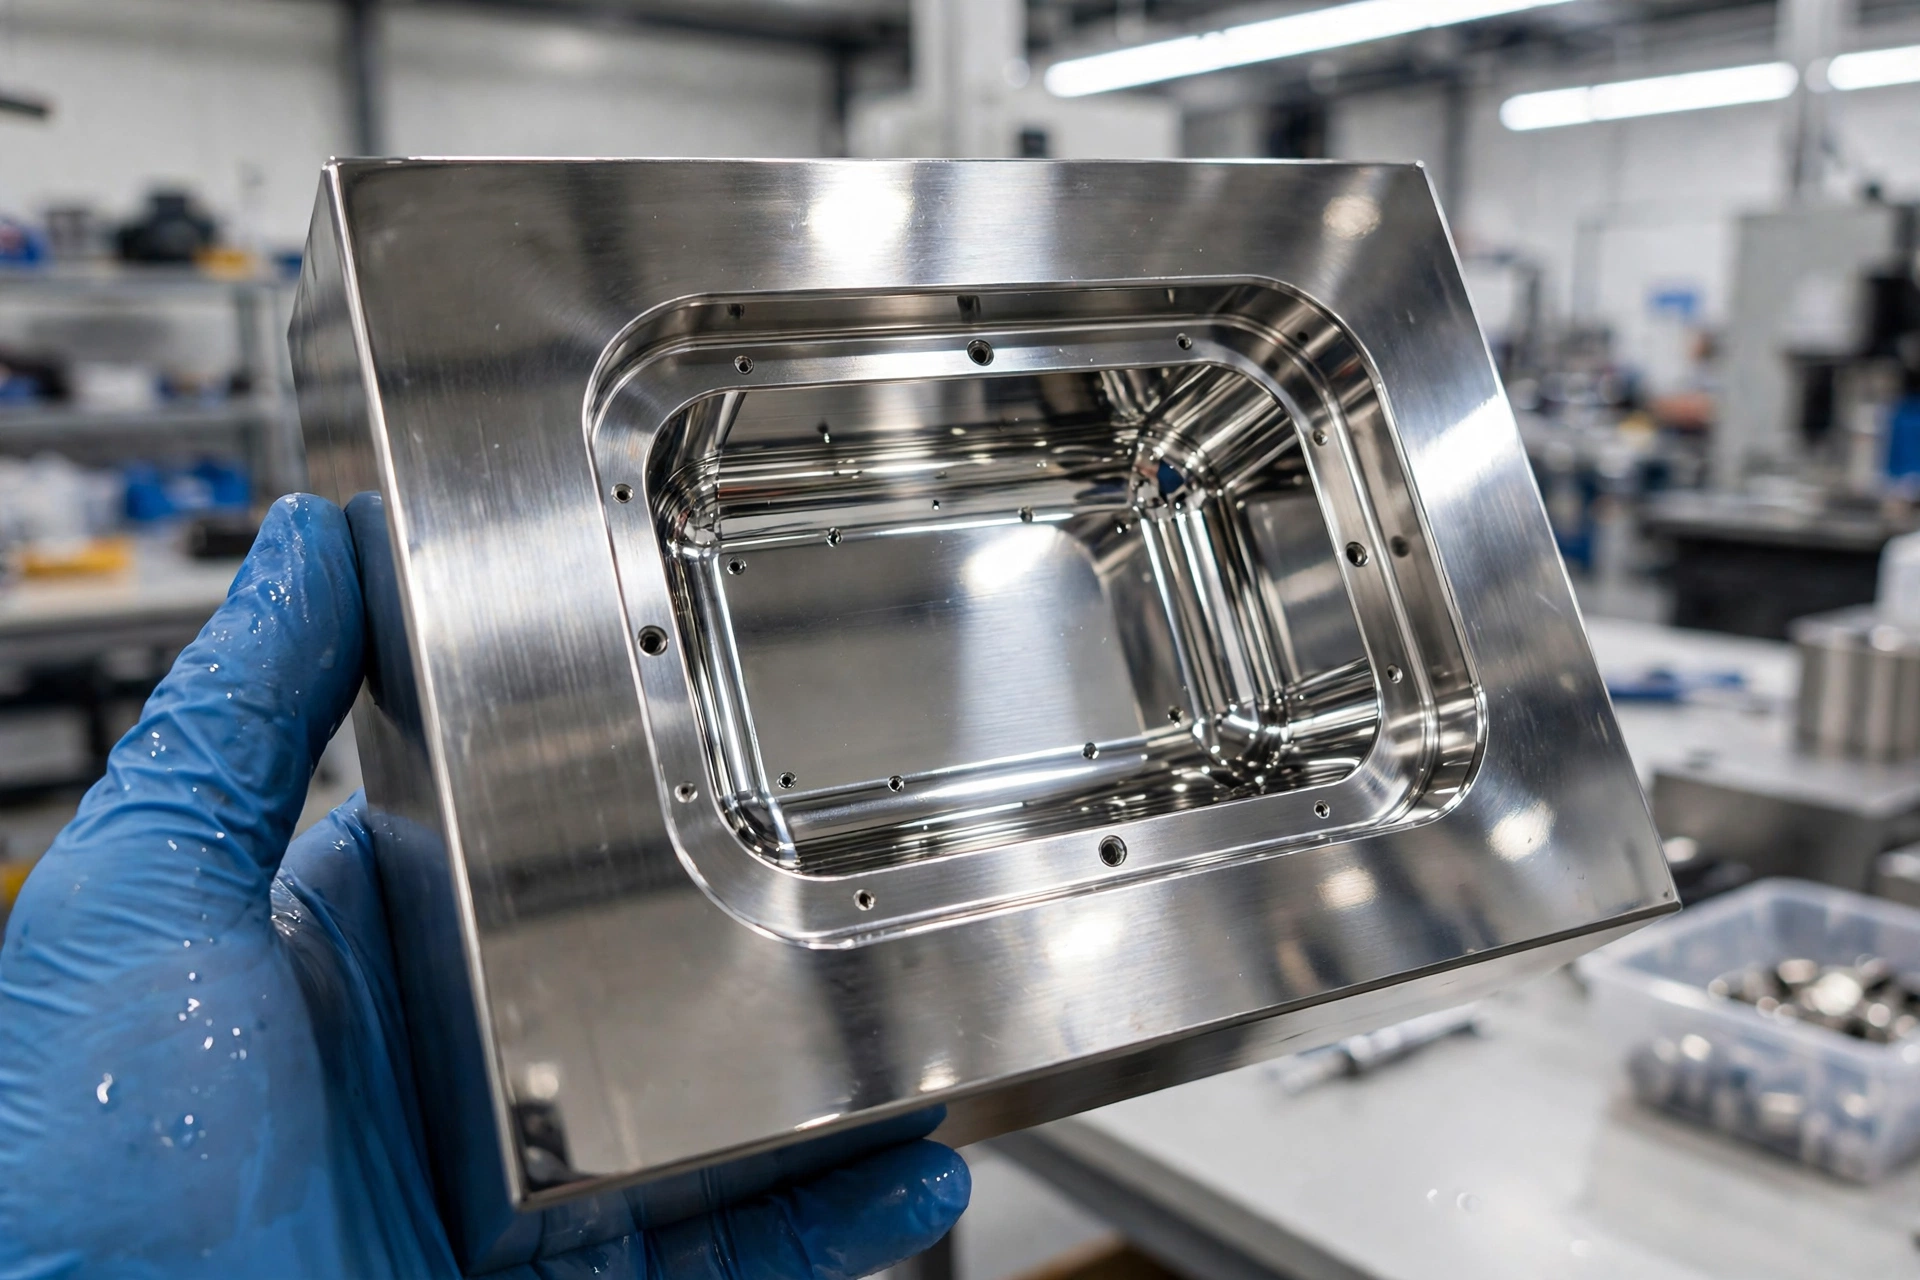
Molded parts receive SPI finishes from A-1 (diamond-polished mirror, Ra 0.012 μm) to D-3 (sandblast texture, Ra 3.2 μm). VDI and Mold-Tech textures are available for grip and cosmetic needs.
Which Mold Material Fits Your Volume?

The mold material sets the shot life of a tool. Use the table as a starting point, and our engineers confirm the choice in DFM review.

Mold material

Typical shot life

Best for

Lead time

Aluminum 70755,000 to 10,000 shotsPrototypes and bridge production15 to 20 business days
P20 pre-hardened steel100,000+ shotsLow to mid volume production25 to 35 business days
H13 hardened steel500,000+ shotsHigh volume production and filled resins25 to 35 business days
S136 stainless steel1,000,000+ shotsCorrosive resins and optical finishes25 to 35 business days

Quantity also decides the process. Below 500 parts, vacuum casting or CNC machining can cost less than a mold. Above 1,000 parts, mold cost spreads out and the part price drops.

Injection Molding Tolerances and Part Sizes

XC Machining holds the tolerances below. Amorphous resins hold tighter tolerances than semi-crystalline resins. Wall thickness uniformity and mold temperature control also set what is achievable.

Specification

Value

Precision toleranceTypical ±0.005 in (±0.127 mm). Up to ±0.002 in (±0.05 mm) on critical dimensions
Shrinkage allowance0.4% to 2.0%, by polymer type
Surface finishRa 8 μin (0.2 μm) to Ra 63 μin (1.6 μm)
Minimum wall thickness0.5 to 1.5 mm, by plastic material
Draft angle0.5° to 2° for most part designs
Gate tolerance±0.003 in (±0.076 mm)
Ejector pin tolerance±0.001 in (±0.025 mm)
Maximum part size1000 x 1000 x 500 mm
Minimum part size5 x 5 x 2 mm
Prototyping volume1 to 500 pieces
Low volume501 to 10,000 pieces
High volumeAbove 10,000 pieces


Plastic Materials for Injection Molding

Our injection molding services cover ABS, Nylon, Polycarbonate, POM, PEEK and PTFE-based parts. These materials differ in strength, impact resistance, heat stability and chemical resistance. They make housings, precision components, automotive parts and industrial products. Part design, performance needs and process fit decide the material.

Injection Molding - XC Machining
ABS

ABS offers impact resistance, stable size and a clean surface. It suits electronic housings, automotive interior parts, protective covers and consumer enclosures.

Color:
Black, white, natural.
Tensile Yield (MPa)
35 to 55 MPa.
Common Grades
general-purpose, impact-modified and flame-retardant ABS.
Injection Molding - XC Machining
Nylon (PA)

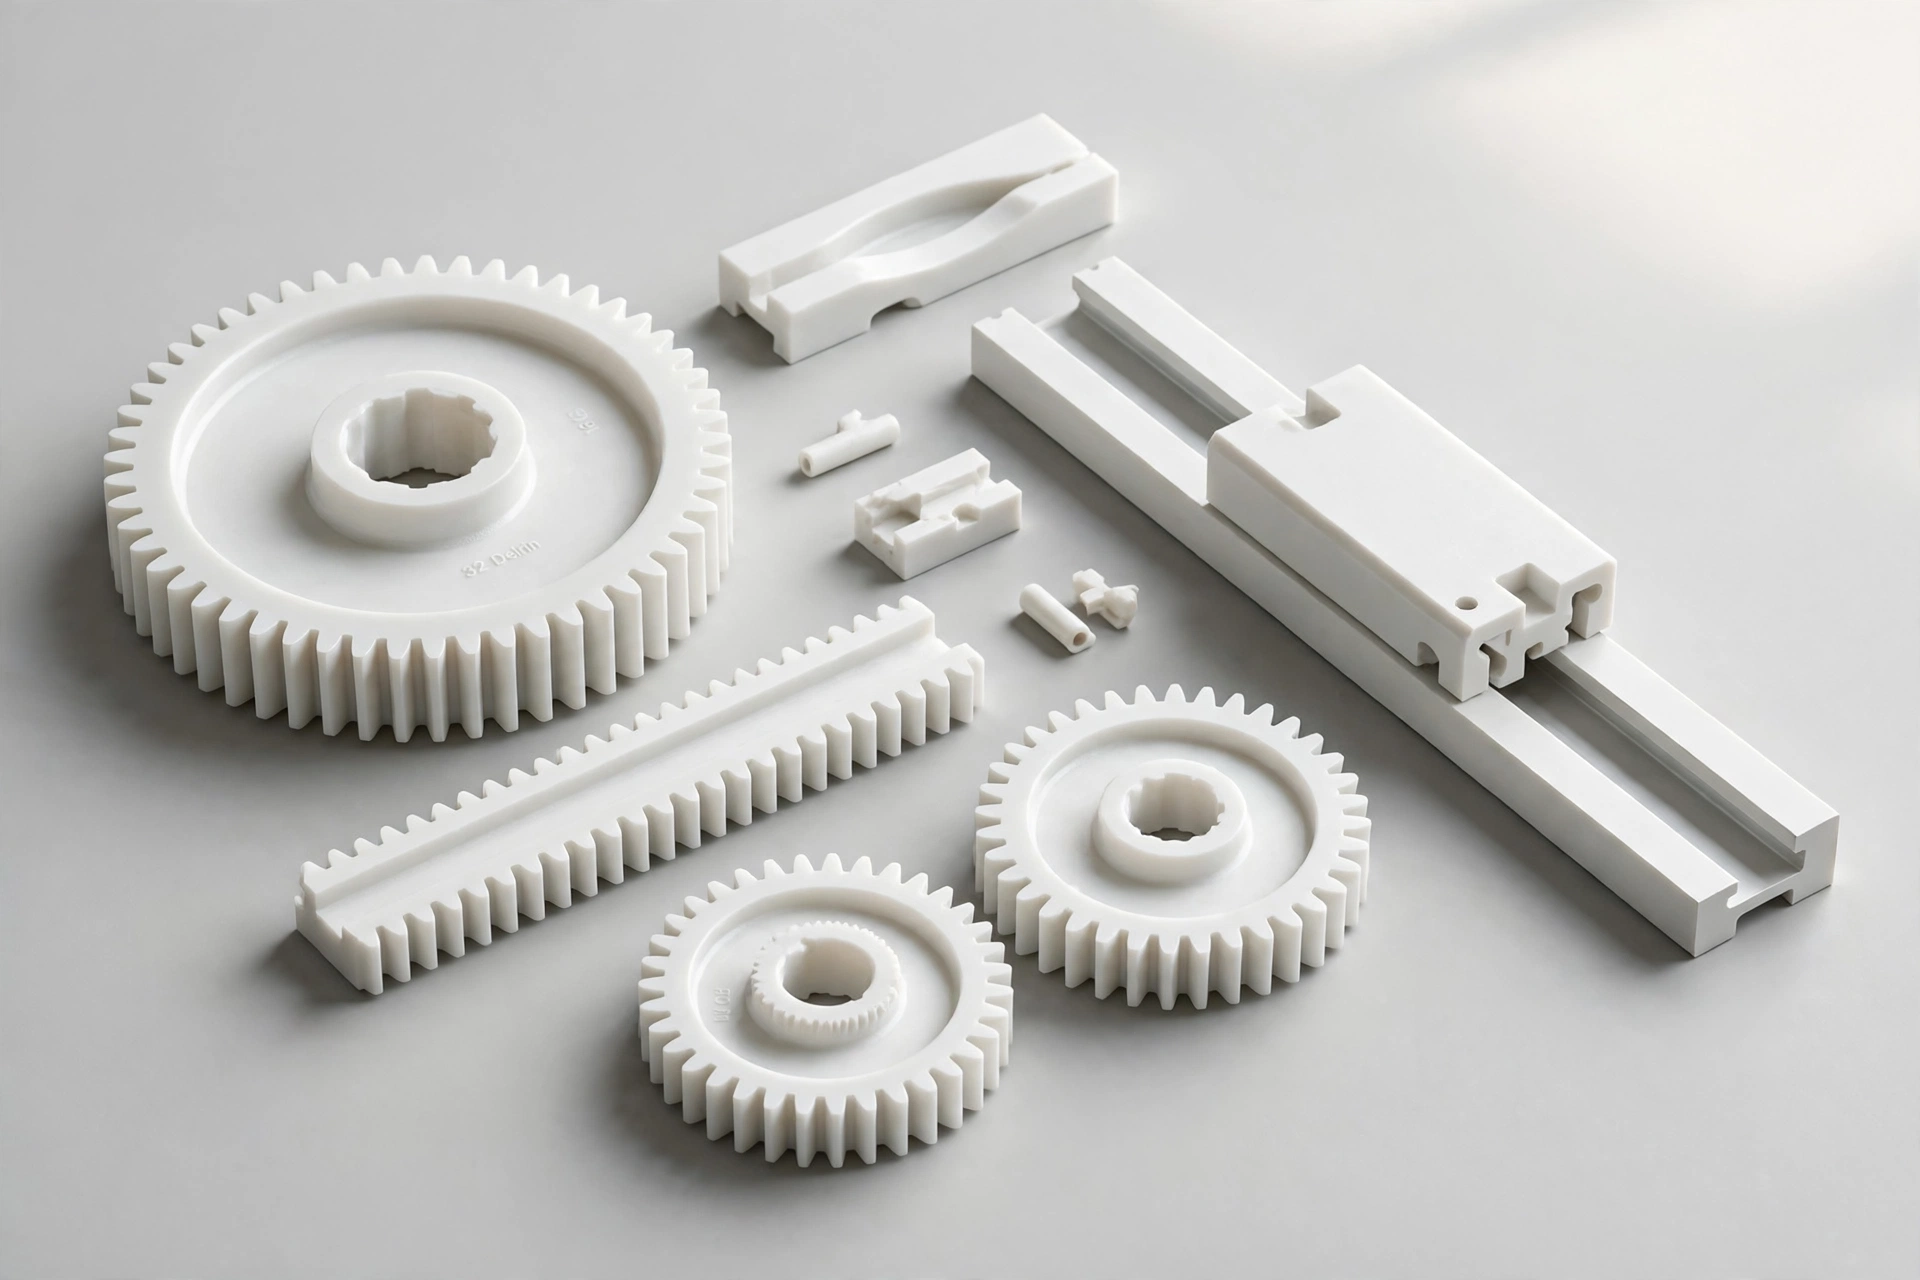
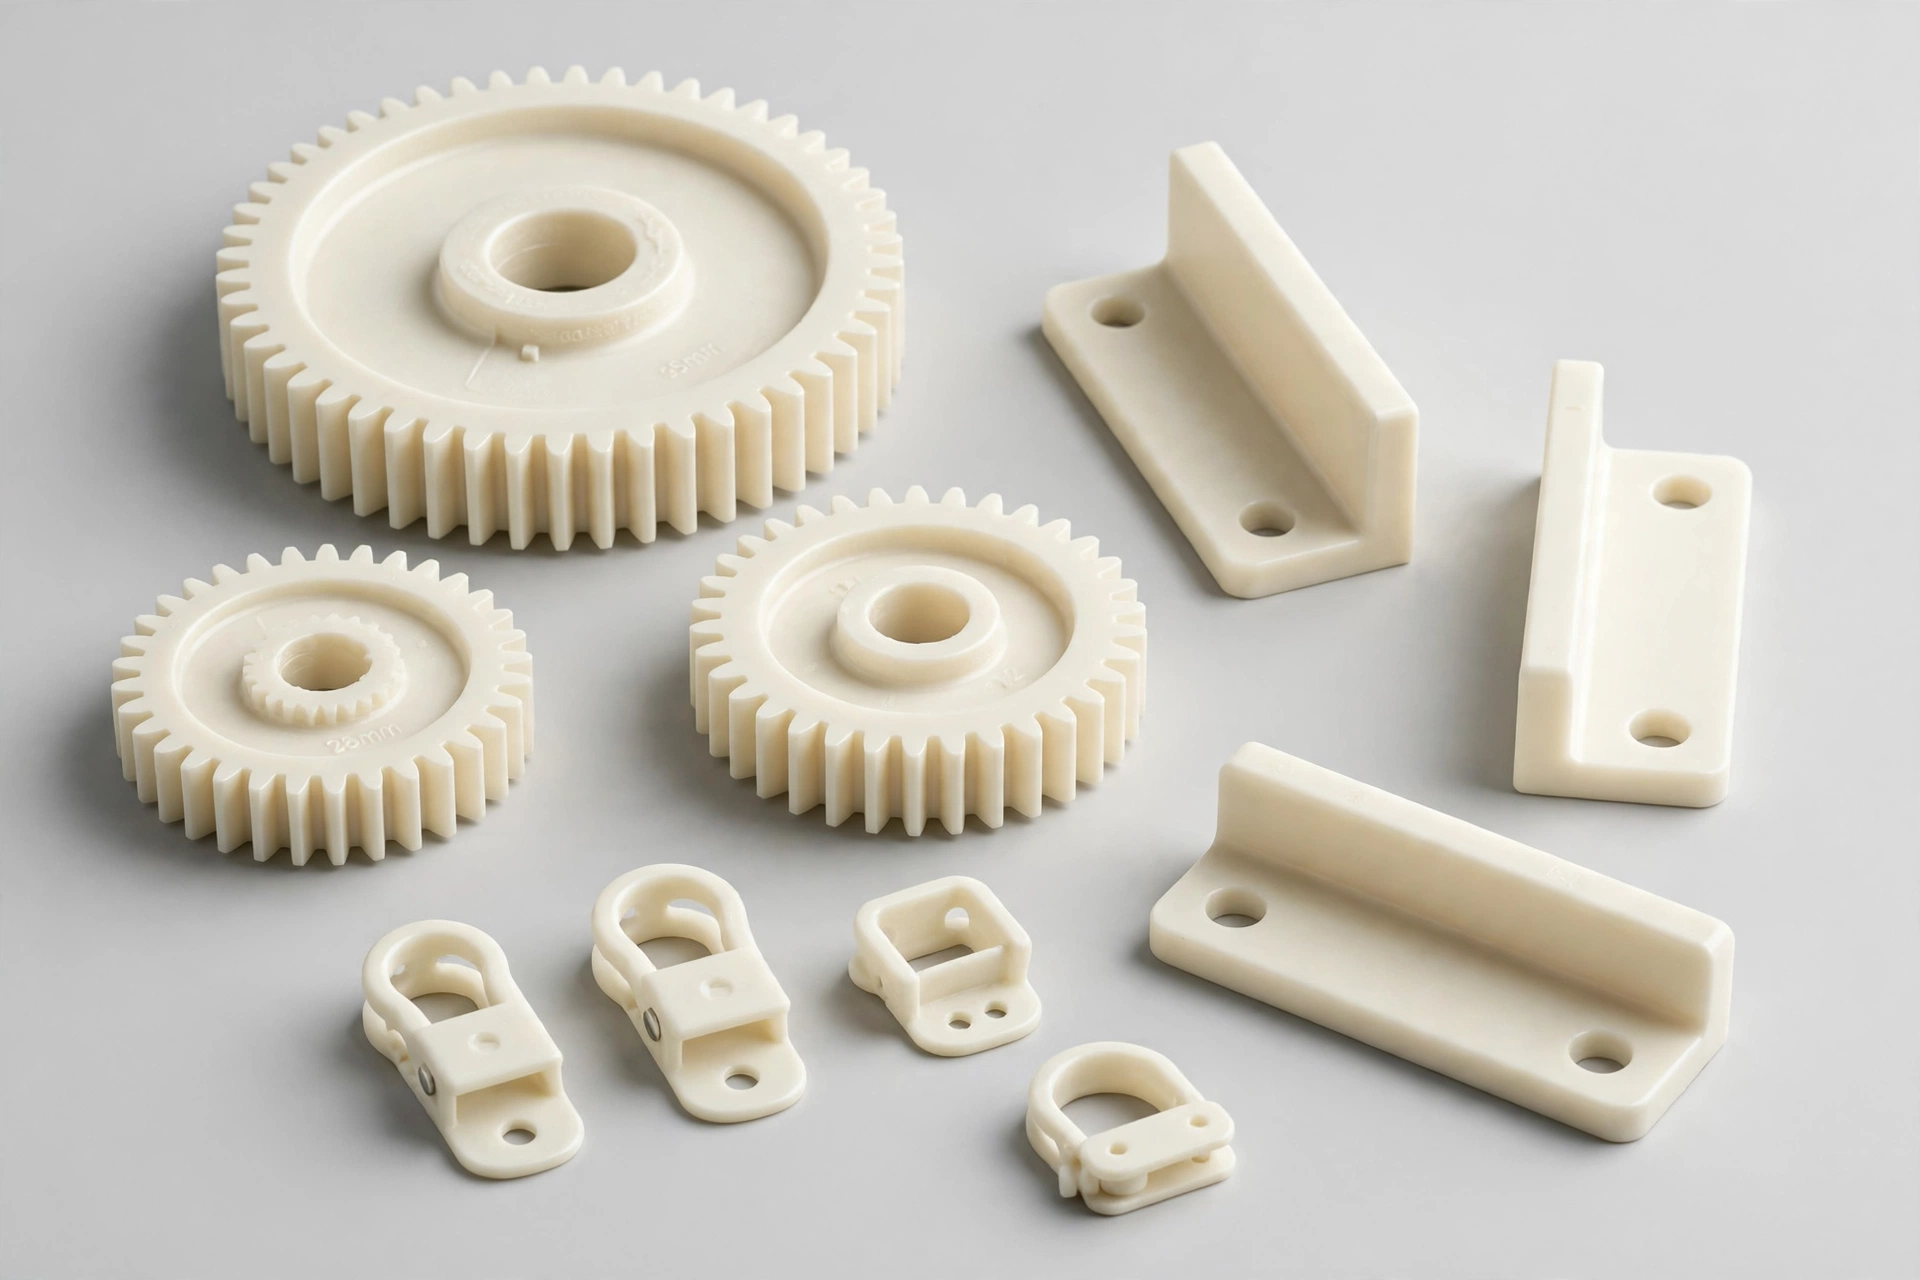
Nylon is strong and wear resistant, with good fatigue resistance and low friction. It suits gears, clips, bushings, brackets and mechanical parts for automotive, electrical and industrial use.

Color:
Natural white, black.
Tensile Yield (MPa)
50 to 90 MPa.
Common Grades
PA6, PA66, PA12 and glass-filled nylon.
Injection Molding - XC Machining
Polycarbonate (PC)

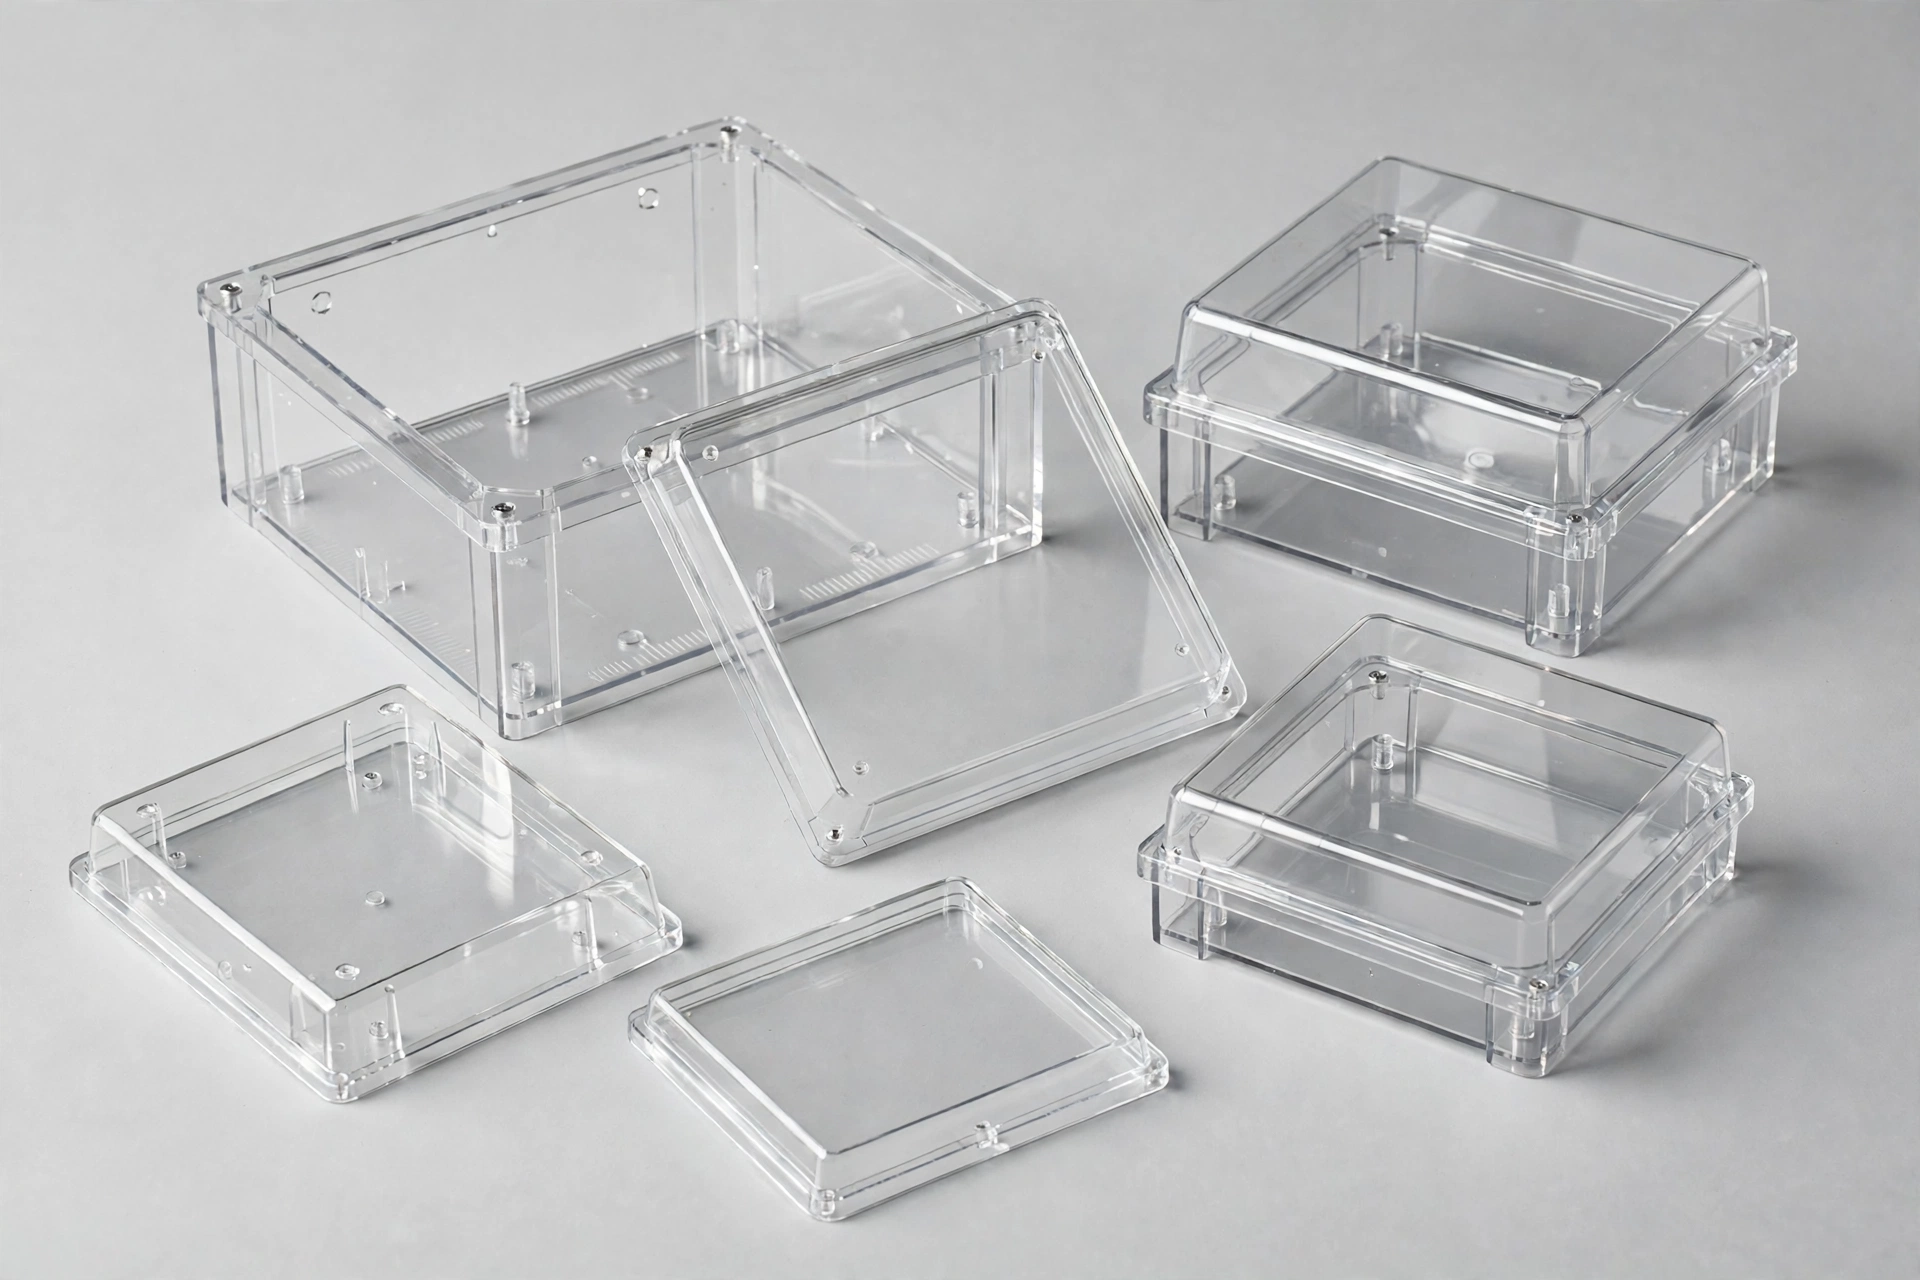
Polycarbonate gives high impact resistance and stable size. Suitable grades give optical clarity. It suits protective covers, transparent housings, electronic enclosures and lenses.

Color:
Transparent, white, black.
Tensile Yield (MPa)
55 to 75 MPa.
Common Grades
general-purpose, optical-grade and flame-retardant PC.
Injection Molding - XC Machining
POM (Delrin)

POM is a stiff engineering plastic with low friction and wear resistance. It suits precision gears, bearings, clips, fasteners and sliding parts that need accurate dimensions.

Color:
Natural white, black.
Tensile Yield (MPa)
60 to 80 MPa.
Common Grades
POM-C, POM-H, Delrin 150 and Delrin 500.
Injection Molding - XC Machining
PEEK

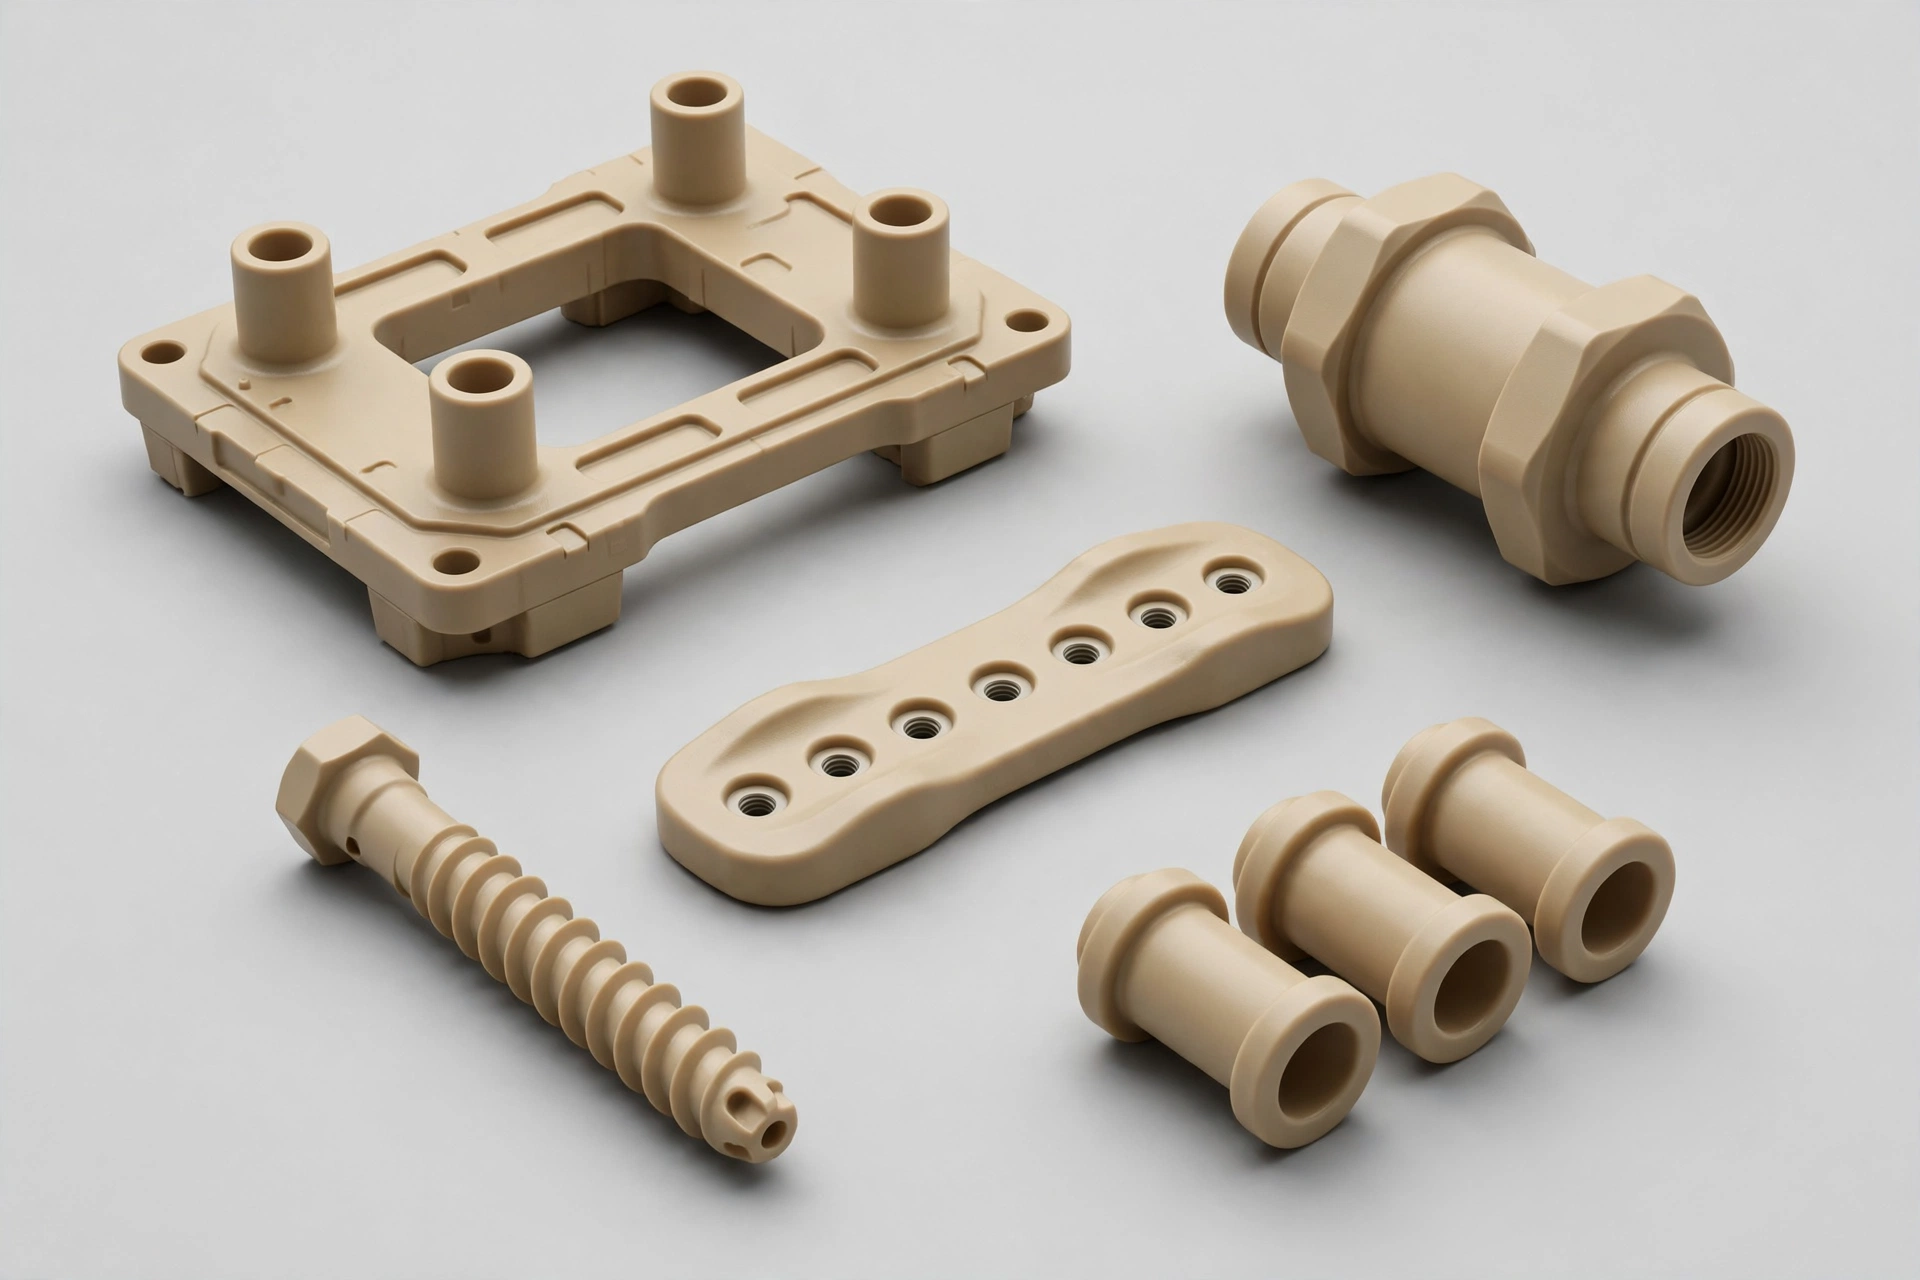
PEEK is a high performance thermoplastic with heat resistance, chemical stability and strength. It suits aerospace parts, medical equipment parts, electrical insulators and industrial parts under demanding conditions.

Color:
Natural beige, black.
Tensile Yield (MPa)
90 to 110 MPa.
Common Grades
unfilled PEEK, PEEK GF30, PEEK CF30 and bearing-grade PEEK.
Injection Molding - XC Machining
PTFE (Teflon)

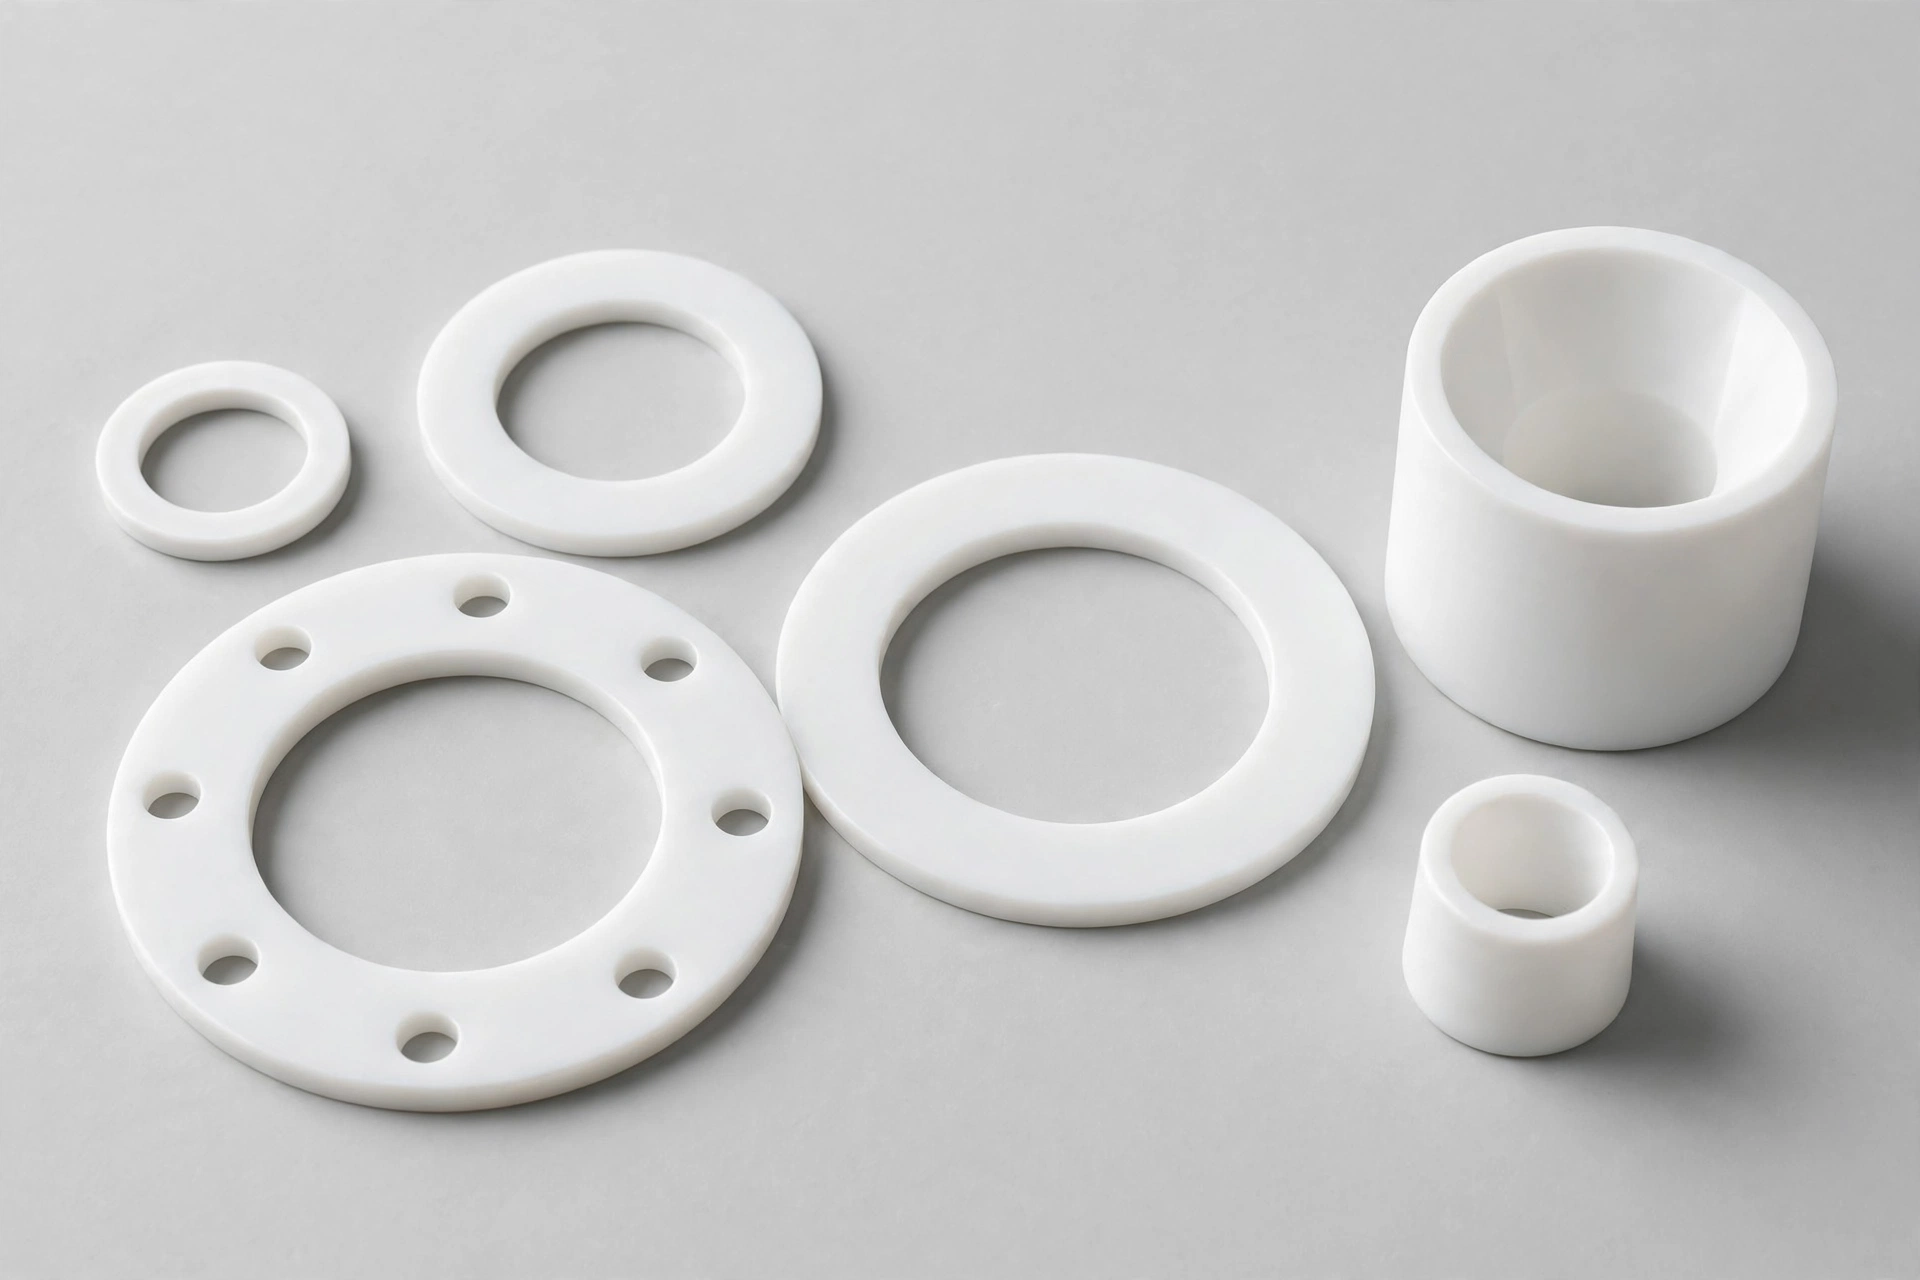
PTFE has exceptional chemical resistance, very low friction and thermal stability. Standard PTFE is usually compression molded and sintered, not injection molded. It suits seals, gaskets, valve seats and chemical-resistant parts.

Color:
White, black.
Tensile Yield (MPa)
20 to 35 MPa.
Common Grades
virgin, glass-filled, carbon-filled and bronze-filled PTFE.

Resins, Elastomers, Ceramics and Metals

XC Machining molds thermoplastics, engineering plastics, elastomers and specialty feedstocks. The groups below list typical materials, shrinkage and processing data.

Plastic

Commodity resins include PP (0.4% to 0.7% shrinkage), PE, PS and ABS. Engineering resins include PC, Nylon 6/66, POM, PBT, PMMA and PPS. High-performance resins include PEEK, PEI (Ultem) and LCP. Processing temperatures run from 180°C to 400°C by resin.

Ceramic

Ceramic injection molding (CIM) uses alumina (Al₂O₃), zirconia (ZrO₂) and silicon nitride (Si₃N₄). It makes wear-resistant, high-temperature and electrically insulating parts with geometry that ceramic pressing cannot form.

Elastomer

Elastomers include TPE-S, TPE-O, TPE-U, TPE-V, TPU and liquid silicone rubber (LSR). They suit soft-touch grips, seals, gaskets and overmolded parts in Shore A 20 to 90. See overmolding for bonded soft-touch layers.

Metal

Metal injection molding (MIM) uses stainless steel 316L and 17-4PH, titanium, copper alloys and tool steel. It makes small, complex metal parts of 1 to 100 g at near-net shape, with 95% to 99% theoretical density.

Injection Molding - XC Machining

Surface Finishes for Molded Parts

We apply these finishes to molded plastic parts and mold cavities. Mold finish follows SPI (Society of the Plastics Industry) grades from A-1 to D-3. Our surface finishing page lists related options.

Injection Molding - XC Machining
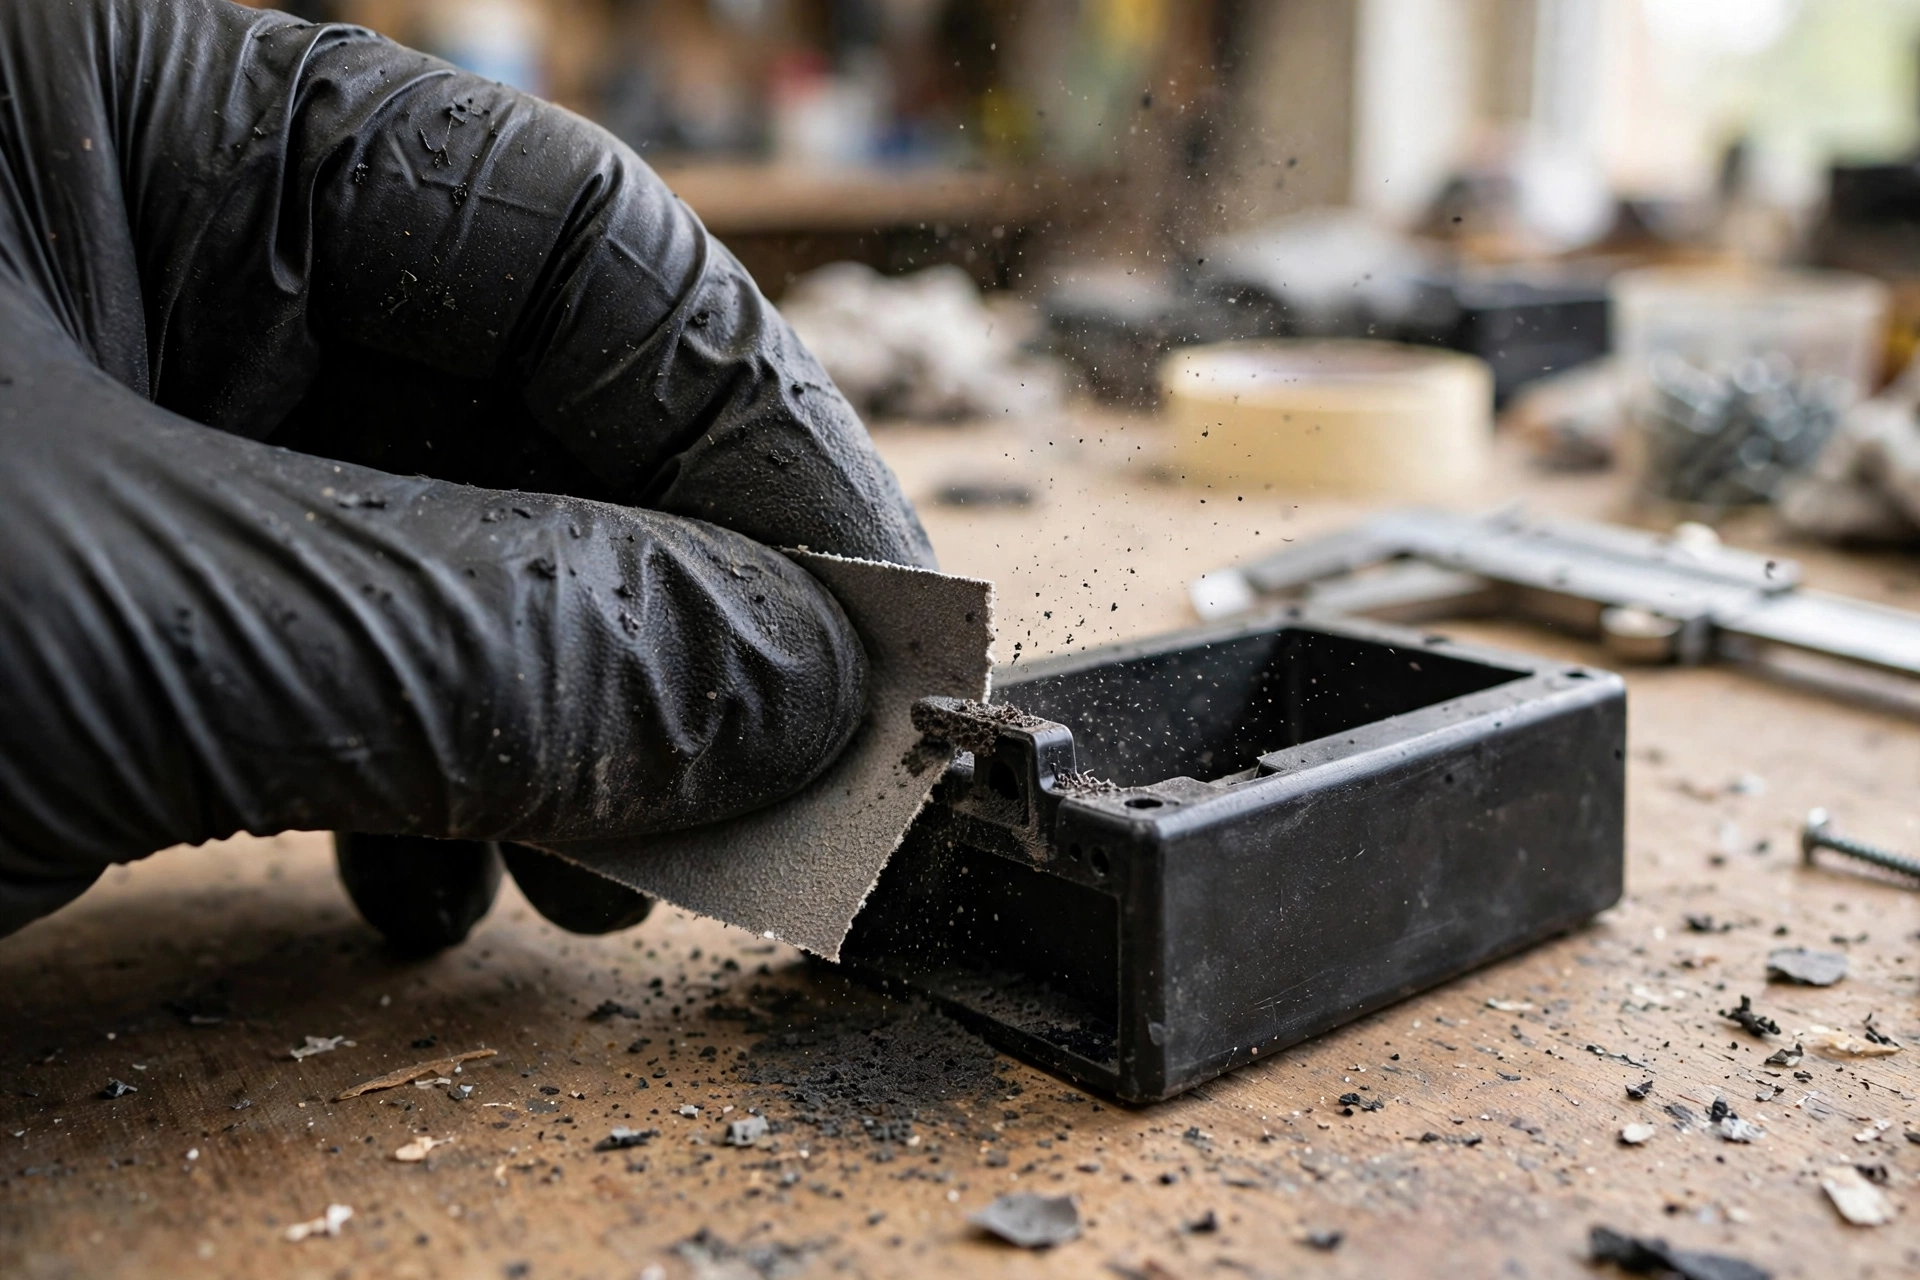
Sanding

removes gate marks, parting line flash and ejector pin marks for a clean surface.

Injection Molding - XC Machining
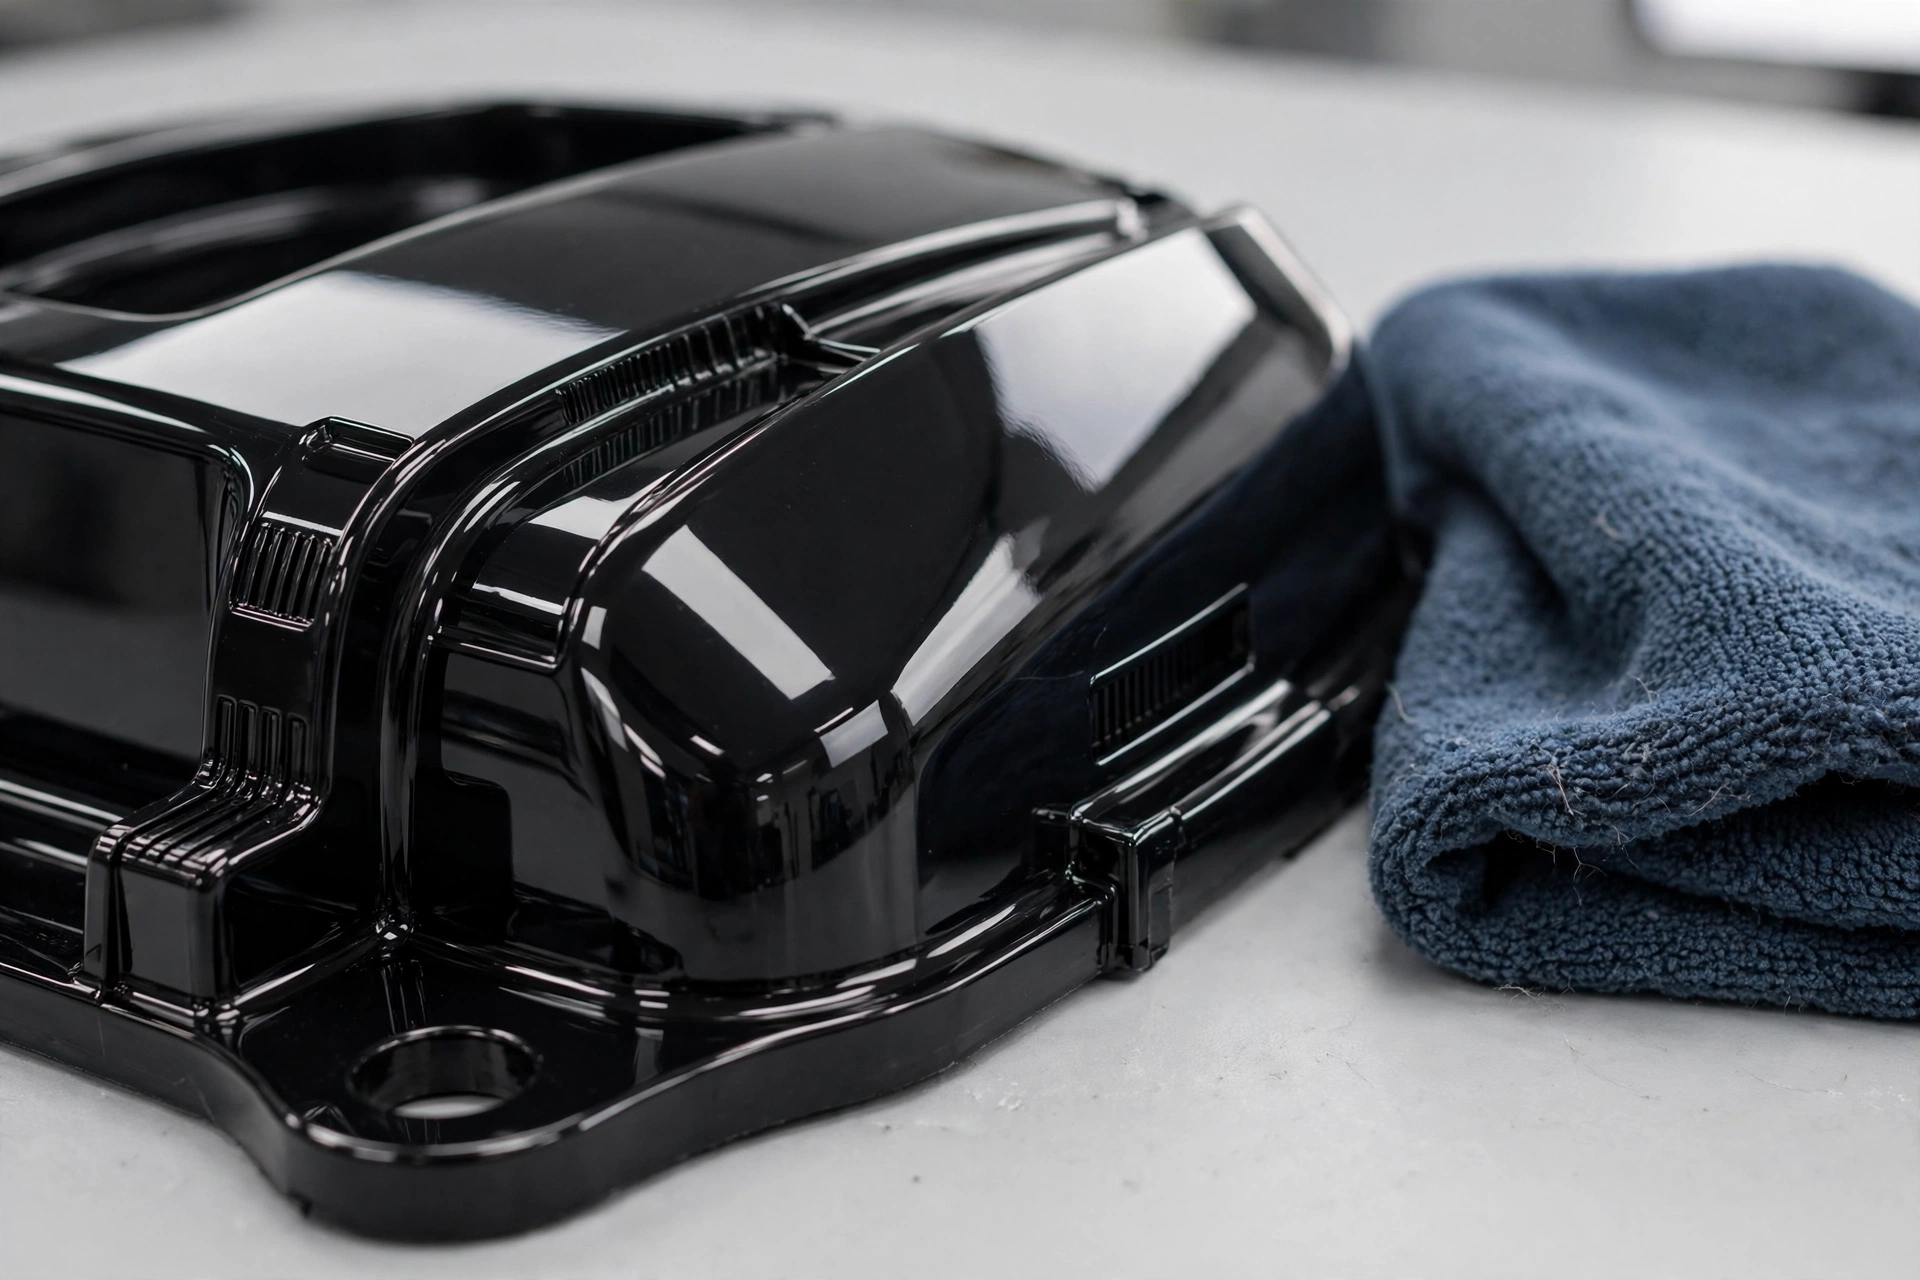
Polishing

SPI A-1 diamond-polished cavities give mirror parts straight from the mold, for lenses, light guides and cosmetic electronics.

Injection Molding - XC Machining
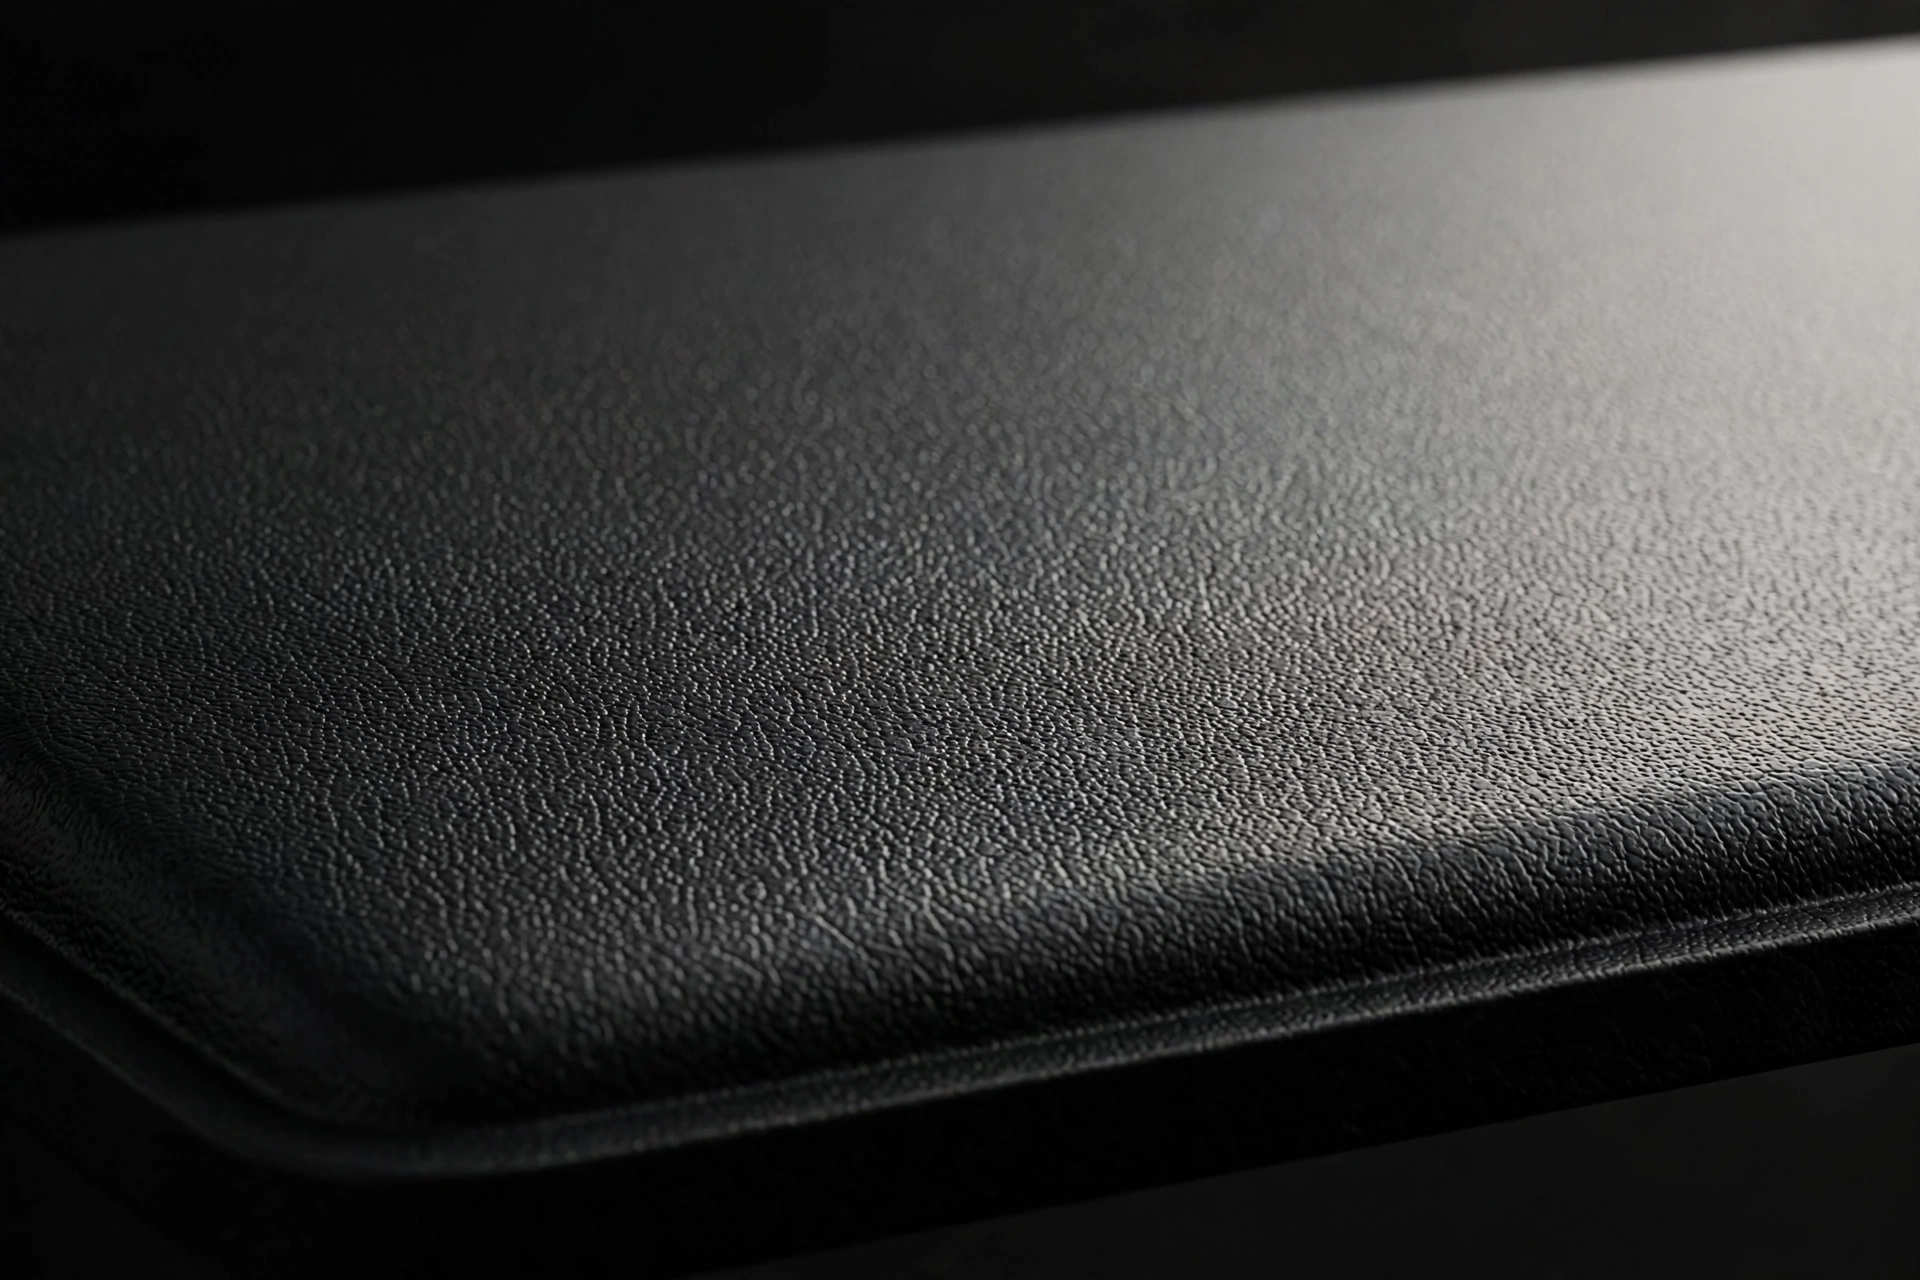
Texturing

Mold-Tech and VDI textures run from fine leather grain to geometric stipple (SPI C-1 to D-3). They hide sink marks, improve grip and reduce fingerprints.

Injection Molding - XC Machining
Electropolishing

applied to S136 and H13 cavities. It helps part release, shortens cycle time and cuts cavity wear.

Injection Molding - XC Machining
Anodizing

Type III hard coat on aluminum prototype molds adds a 25 to 50 μm oxide layer. It extends mold life from 5,000 to 10,000+ shots at SPI B-1 quality.

Injection Molding - XC Machining
Vibratory finishing

batch deburring removes gate nubs and flash for safe handling.

Injection Molding - XC Machining
Sand blasting

an even matte texture that prepares surfaces for coating.

Injection Molding - XC Machining
Brushing

a directional grain on accessible metal inserts.

Injection Molding - XC Machining
Powder coating

a durable colored coat on suitable metal inserts and brackets.

Injection Molding - XC Machining
Electroplating

nickel, chrome, zinc or gold layers on metal parts for corrosion resistance, conductivity and wear.

Our Injection Molding Prototype Manufacturing Capabilities

As a leader in precision manufacturing, we offer a wide range of capabilities that cater to both one-off prototyping and low-volume production. We specialize in delivering geometrically complex and highly cosmetic parts, ensuring the highest quality standards. At XC Machining, we pride ourselves on being the go-to manufacturer for all your Injection Molding needs, providing reliable and efficient solutions under one roof.
With 3, 4, and 5-axis CNC machining services, we can produce complex prototypes and parts with precise tolerances. More than 60+ materials are available for you to choose from.

Provides injection molding for prototypes and custom parts, emphasizing expert support, competitive pricing, and faster production cycles.

Get reliable vacuum casting services for high-quality prototypes and production parts at competitive prices. XC Machining offers highly detailed casting parts with consistent quality.

Uses cutting, bending, and forming techniques to produce precision metal components suited for industrial, commercial, and manufacturing applications.

Specialist Industries

XC Machining is a trusted partner for industries demanding complexity, reliability and precision. Our extensive experience in producing millions of high quality components brings unmatched expertise to every project. Our services cover a diverse range of applications to ensure that we meet the unique needs of each sector with great care.
Get In Touch

Bring Your Designs to Life with XC Machining

Experience precision engineering with XC Machining. From detailed prototypes to high-volume production, we’re here to turn your concepts into reality. Contact us today to discuss your project needs!

Get In Touch With Us!
Prompt response guaranteed within 12 hours

Injection Molding FAQs

Injection molding drops the part price above 1,000 units as the mold cost spreads out. Cycle times of 15 to 60 seconds support high volume. It holds tolerances to ±0.05 mm across runs and offers 50+ resins. One shot forms undercuts, living hinges and snap fits. Runner regrind keeps waste under 5% of material.

Accuracy depends on four factors: resin shrinkage (0.4% to 2.0%), mold temperature stability (±2°C), injection pressure consistency and wall thickness uniformity. Typical tolerance is ±0.127 mm, with ±0.05 mm on critical dimensions. We verify production parts with CMM inspection and go/no-go gauges against your drawing.

Yes. Aluminum rapid tooling produces 500 to 10,000 parts at 40% to 60% lower tooling cost than hardened steel molds. Aluminum molds ship in about 15 days against 25 to 35 days for steel. That suits bridge production and market tests. Below 500 parts, consider CNC machining or vacuum casting.

Aluminum prototype tooling ships in 15 to 20 business days with T1 samples. Steel production tooling ships in 25 to 35 business days. After mold approval, production parts ship in 5 to 10 business days per batch, by quantity and resin availability. Rush delivery is available for time-critical projects.

CNC Manufacturing Resources